Compressor Cast Iron Housing Casting
Compressor Cast Iron Housing Casting is one of the core capabilities of our ISO 9001:2015 certified foundry in China. We produce custom compressor cast iron housing parts in grey iron and ductile iron — from compact compressor bearing housing casting components to heavy centrifugal compressor volute casting parts of several tons. In-house pattern making, resin sand molding, CNC machining and 100% pressure testing allow us to supply ready-to-install housings to OEMs, engineering contractors and aftermarket distributors worldwide.
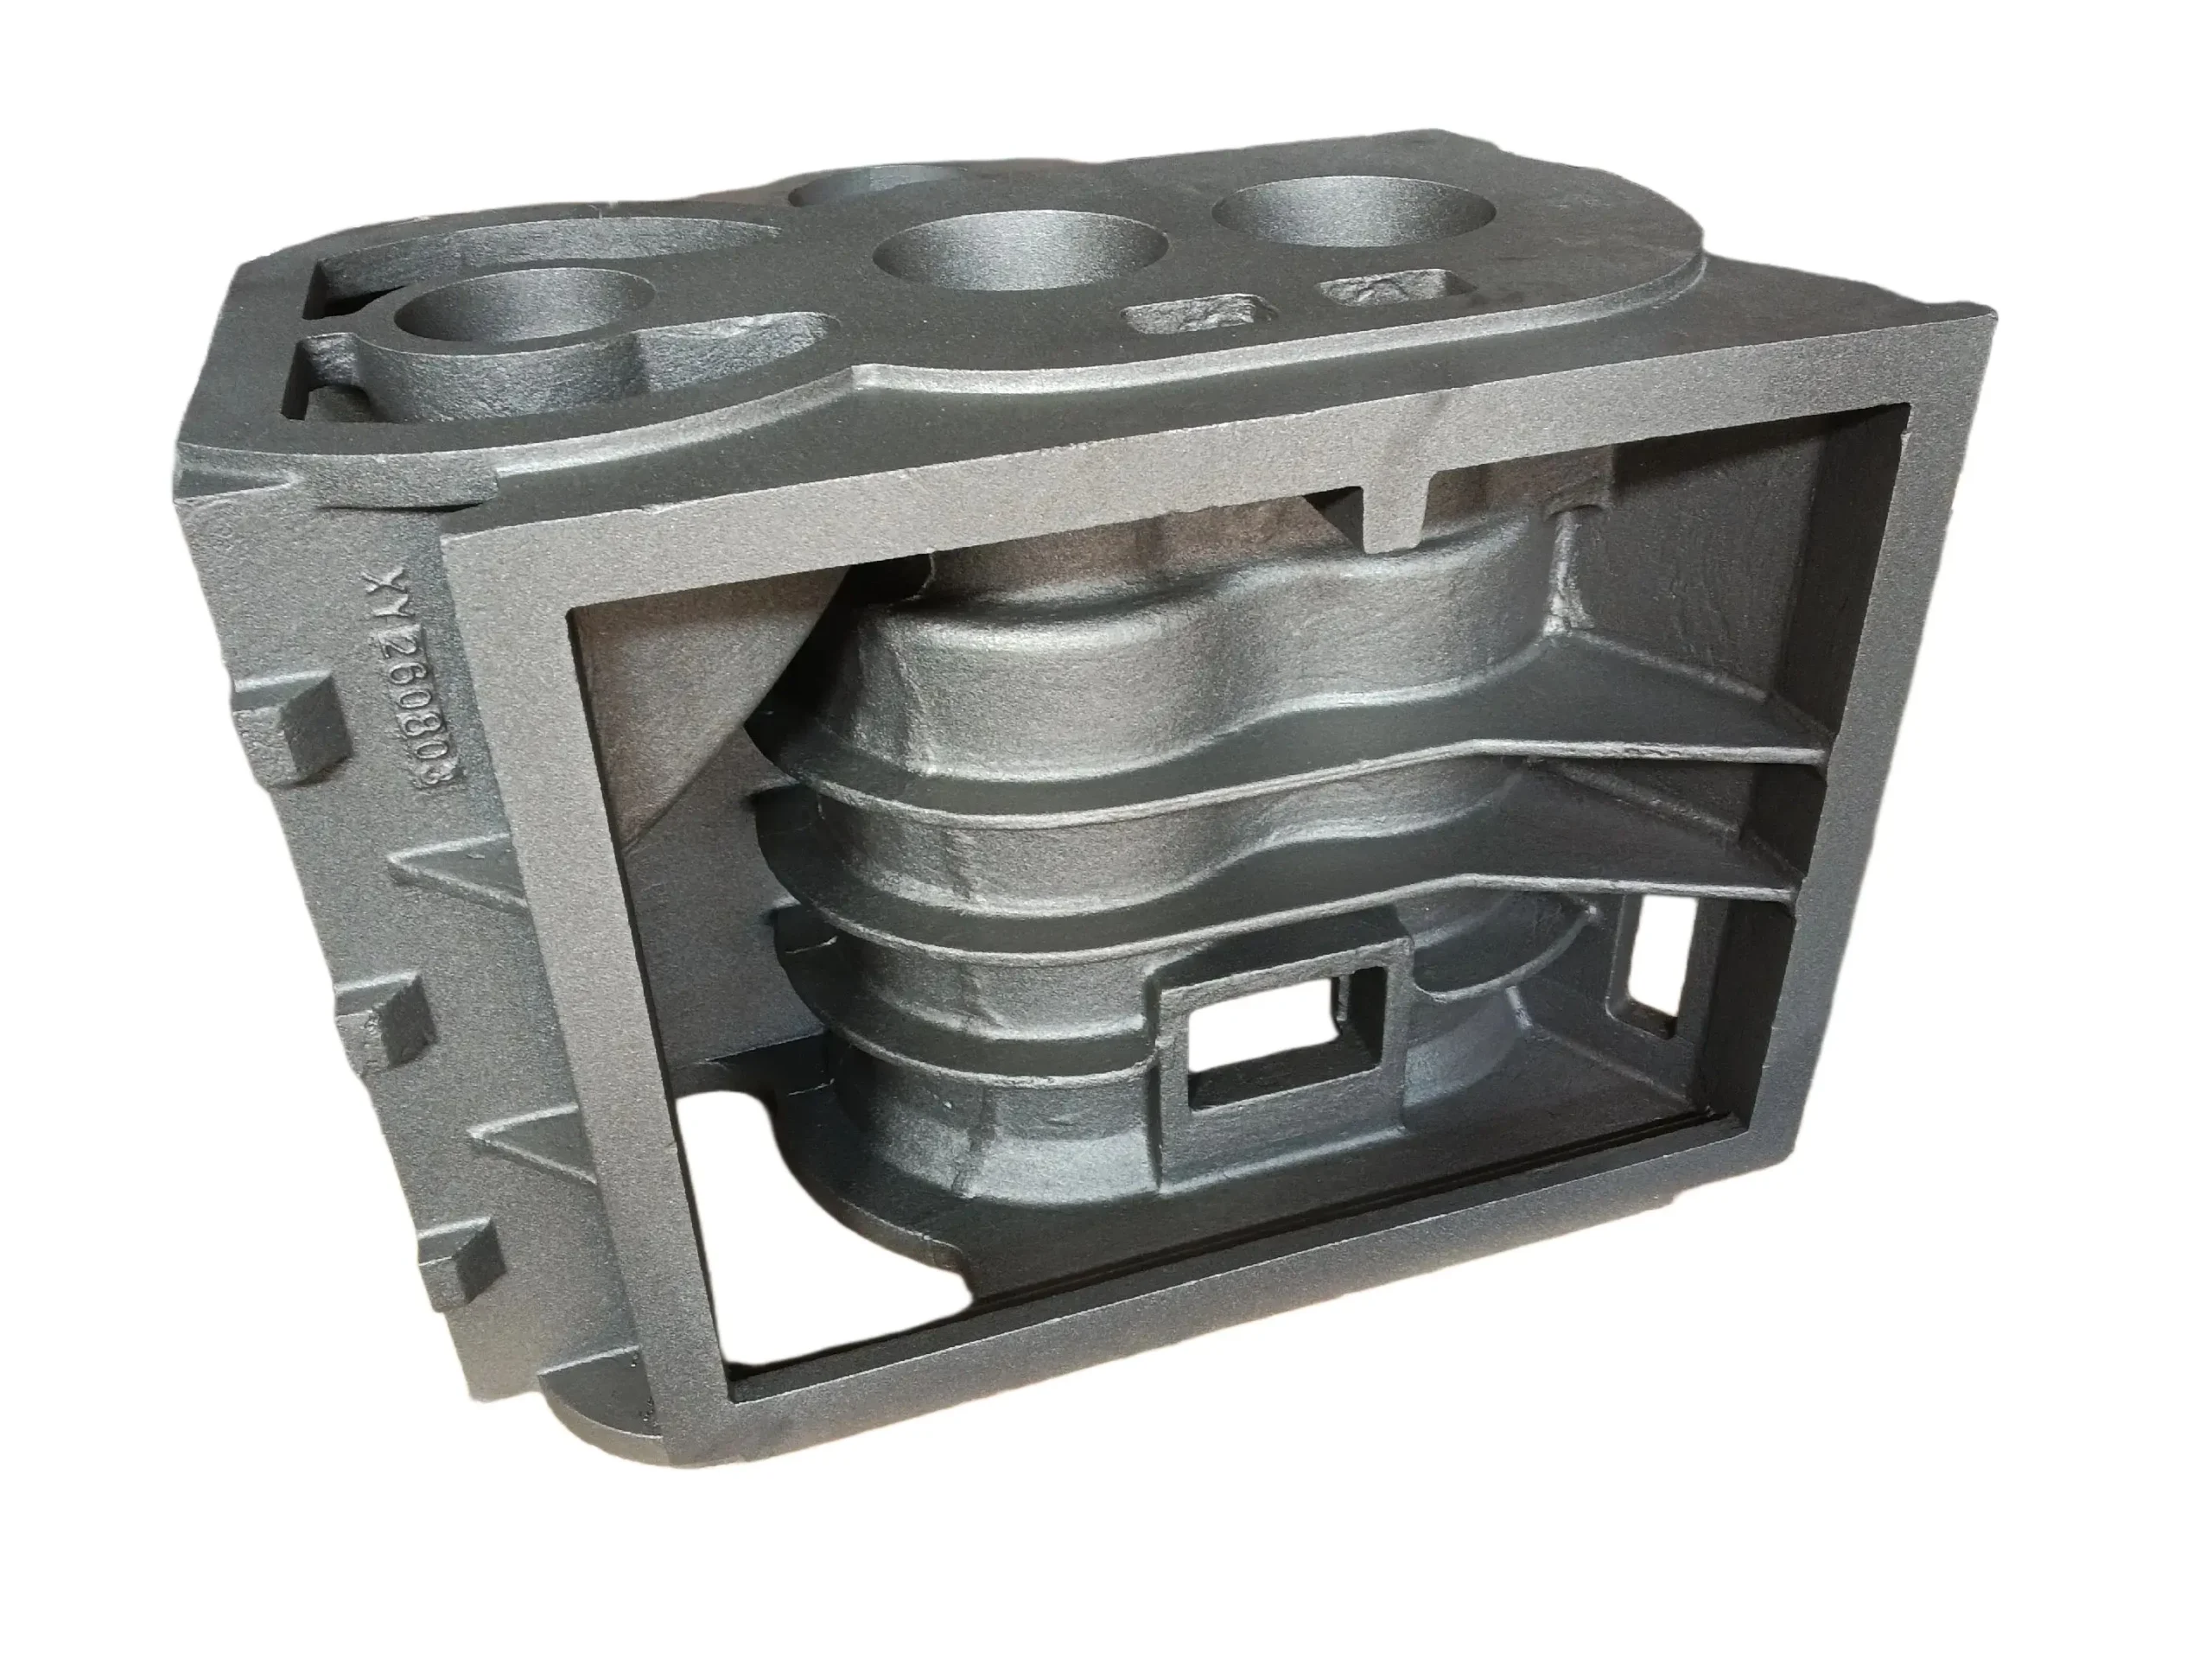
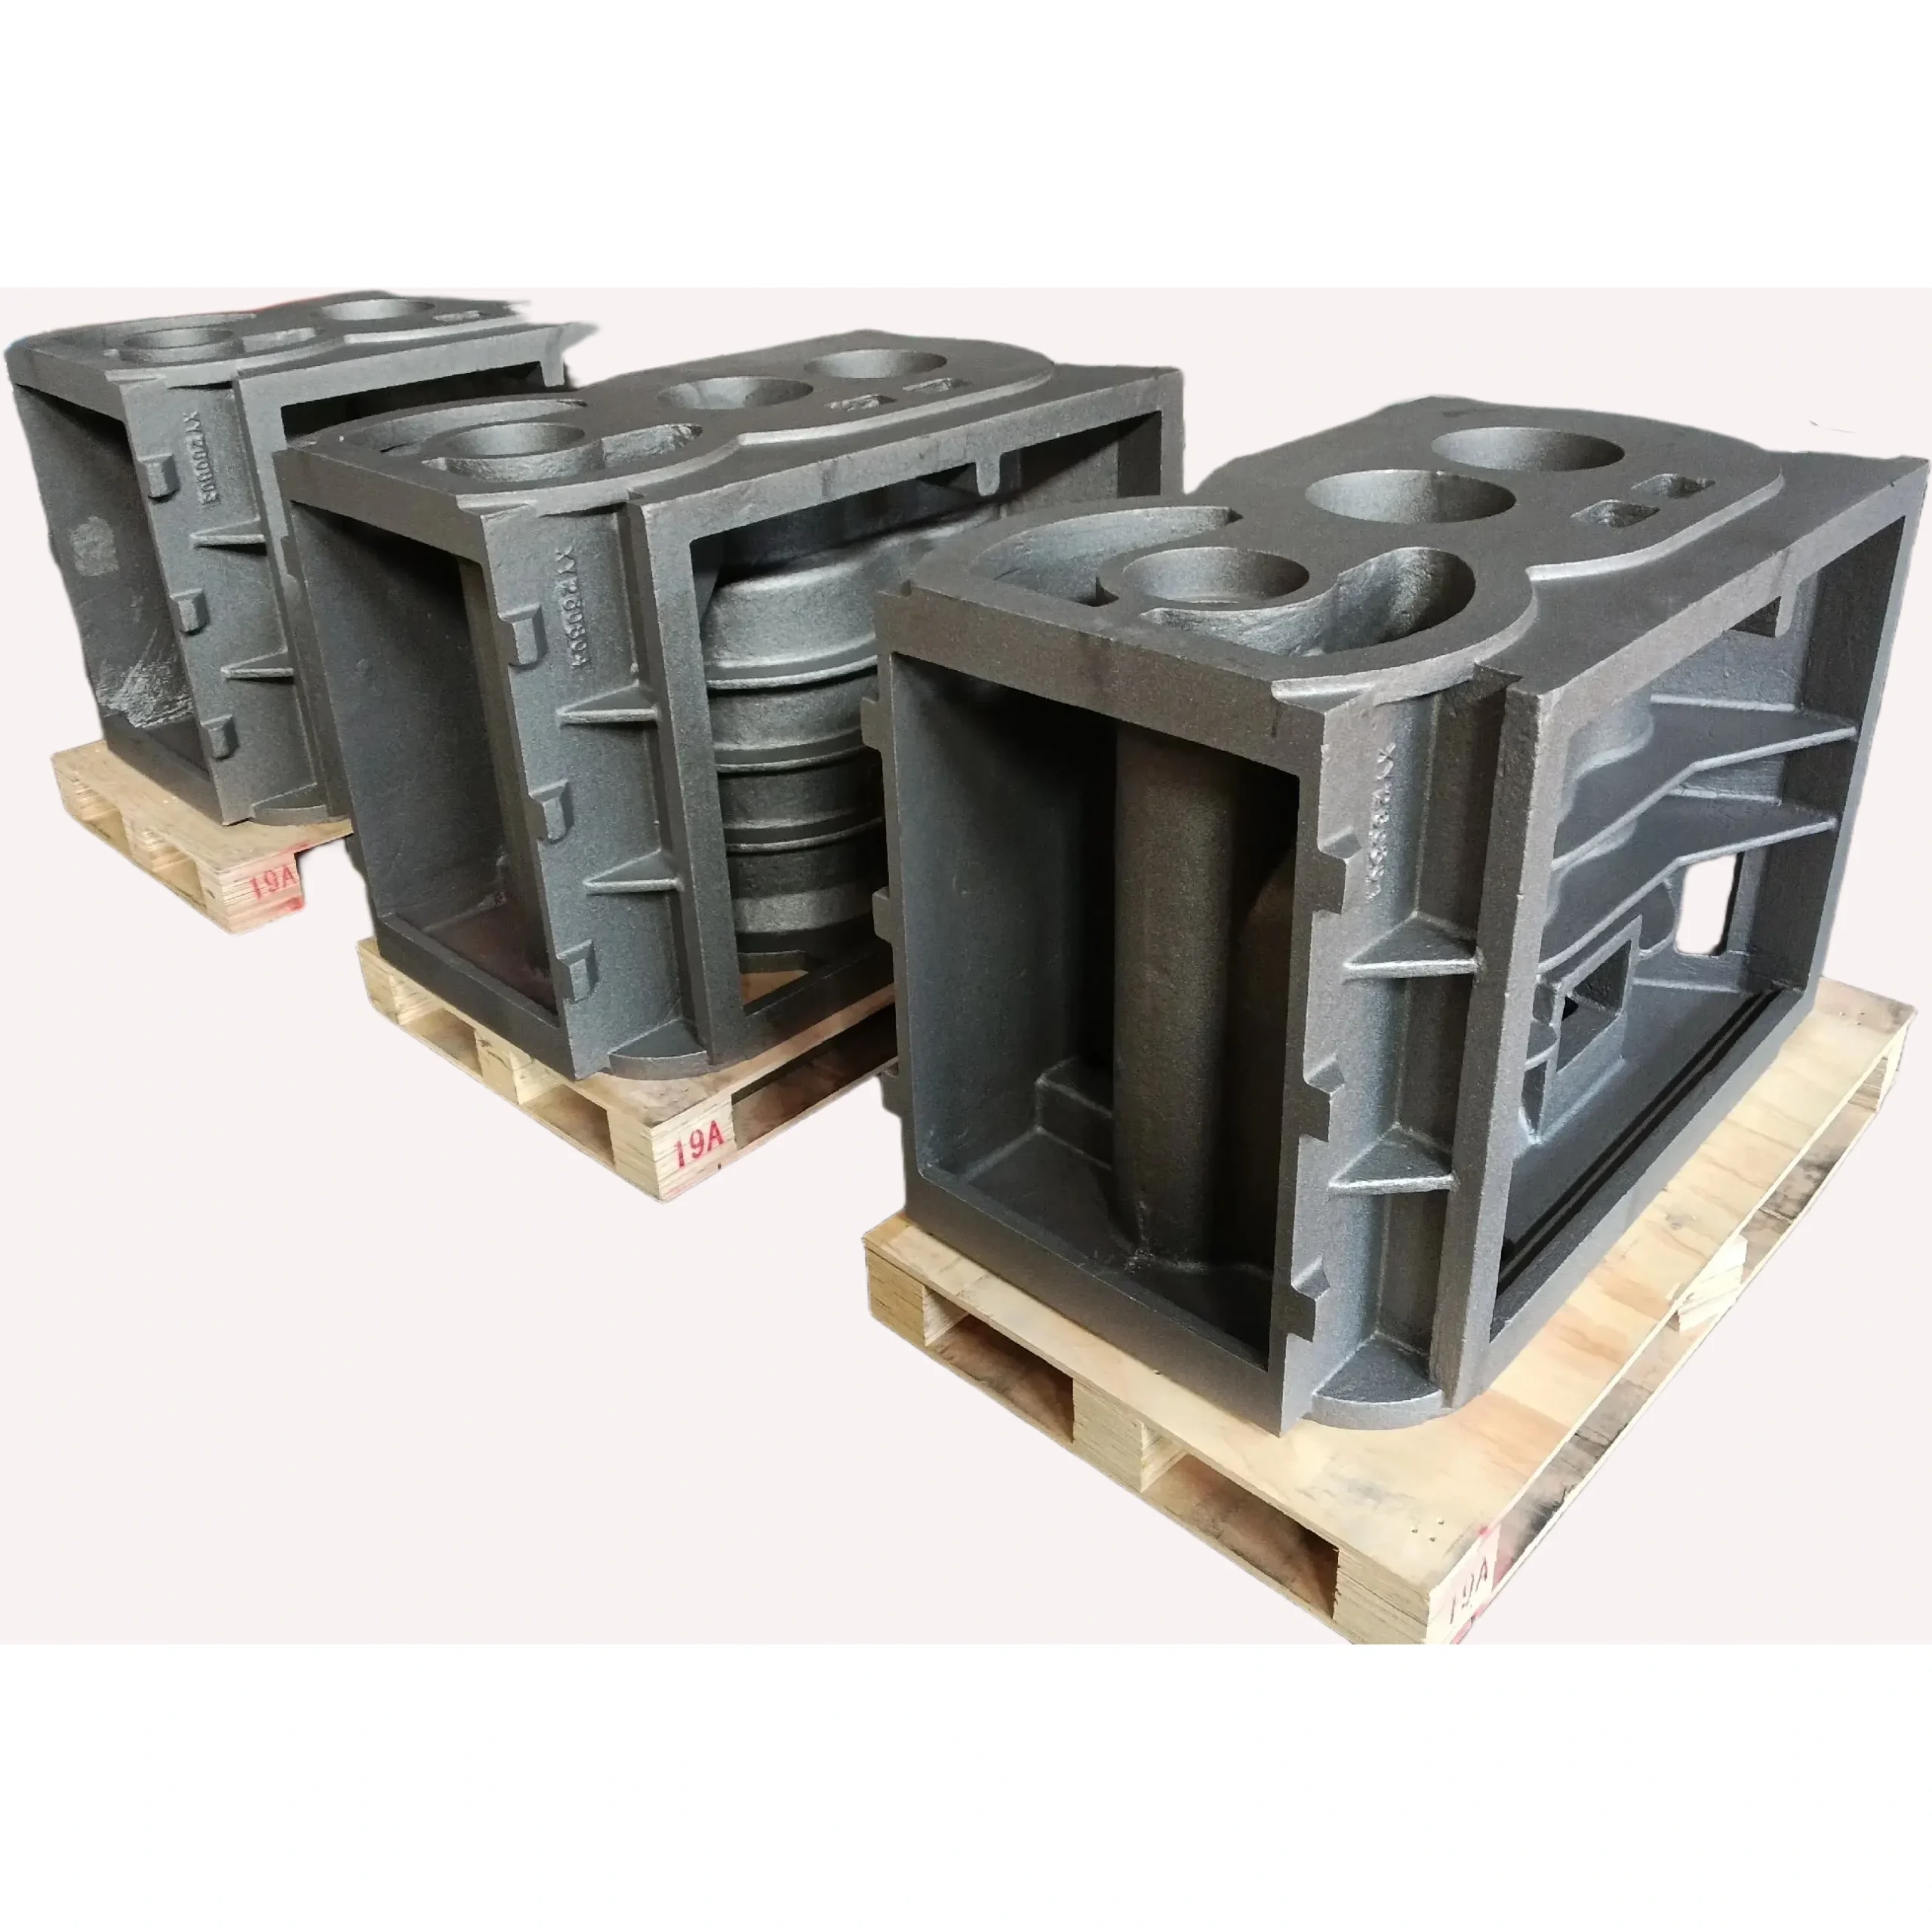
Compressor Cast Iron Housing Casting Product Gallery
The photos below show typical compressor cast iron housing casting parts finished in our machining workshop:
Custom Compressor Cast Iron Housing Solutions
Every compressor cast housing iron casting we deliver is controlled from the melting furnace to the final machining bench. Typical compressor cast iron housing casting parts we produce include volute casings, bearing housings, rotor housings and end covers. Compared with steel fabrication, a casting keeps the gas passage smooth and airtight, reaches complex volute geometry and reduces unit cost significantly at production volume.
- Material grades: grey iron HT150–HT300 (GG15–GG30) and ductile iron QT400–QT600 (GGG40–GGG60), produced to GB, ASTM, EN or DIN standards;
- Casting processes: resin sand, green sand and shell molding, with part weights from 0.5 kg to 8,000 kg;
- Precision machining: CNC lathes and machining centers finish rotor bores, bearing seats and sealing faces at Ra 3.2–6.3 μm;
- Quality assurance: spectrometer analysis, CMM dimension inspection and air or hydrostatic pressure tests on every batch;
- Flexible cooperation: prototypes made directly from 3D models, low MOQ for samples and stable capacity for mass production.
Product Specifications
The table below shows the standard capability range of our compressor cast iron housing casting service; requirements beyond these values are always welcome.
| Item | Specification |
|---|---|
| Material grades | Grey iron HT150/HT200/HT250/HT300 (GG15–GG30); ductile iron QT400–QT600 (GGG40–GGG60) |
| Casting process | Resin sand casting, green sand casting, shell molding; furan resin sand for large housings |
| Weight range | 0.5 kg – 8,000 kg per piece |
| Max dimensions | Up to 4,500 × 2,500 × 1,800 mm |
| Typical parts | Compressor cast iron housing casting bodies, volute casings, bearing housings, end covers |
| Tolerance | ISO 8062 CT10–CT12 as cast; machined dimensions per drawing (ISO 2768) |
| Surface finish | Ra 3.2–6.3 μm on machined faces; shot blasted as cast |
| Heat treatment | Stress-relief annealing or aging on request |
| Pressure test | Air or water test at 0.6–1.0 MPa (or per drawing), 100% for gas passages |
| Surface treatment | Anti-rust oil, primer and epoxy painting per requirement |
| Quality documents | Spectrometer report, dimension report, pressure test report; MT/UT on request |
Casting & Machining Process Flow
Each compressor cast iron housing casting passes through eight controlled steps before shipment:
| No. | Process Step | Key Control |
|---|---|---|
| 1 | Pattern & core box making | CAD/CAM pattern design with machining allowance; resin or metal patterns |
| 2 | Molding & core making | Resin sand molding; shell or sand cores form volute channels and cooling cavities |
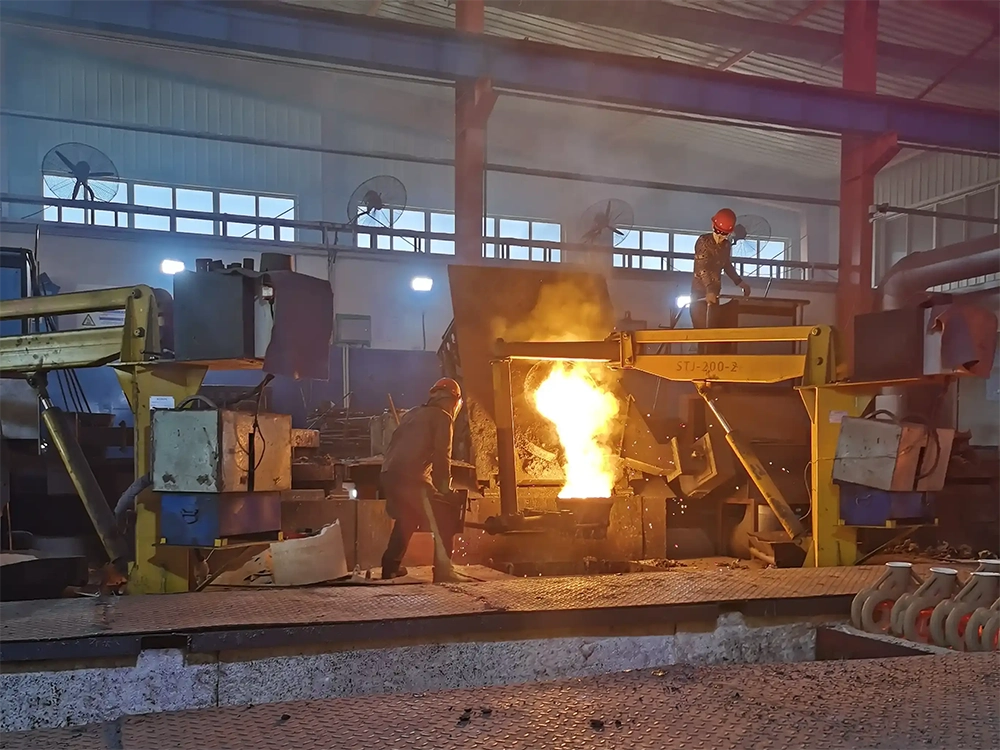
| 3 | Melting & pouring | Medium-frequency induction furnaces; spectrometer check before every pour |
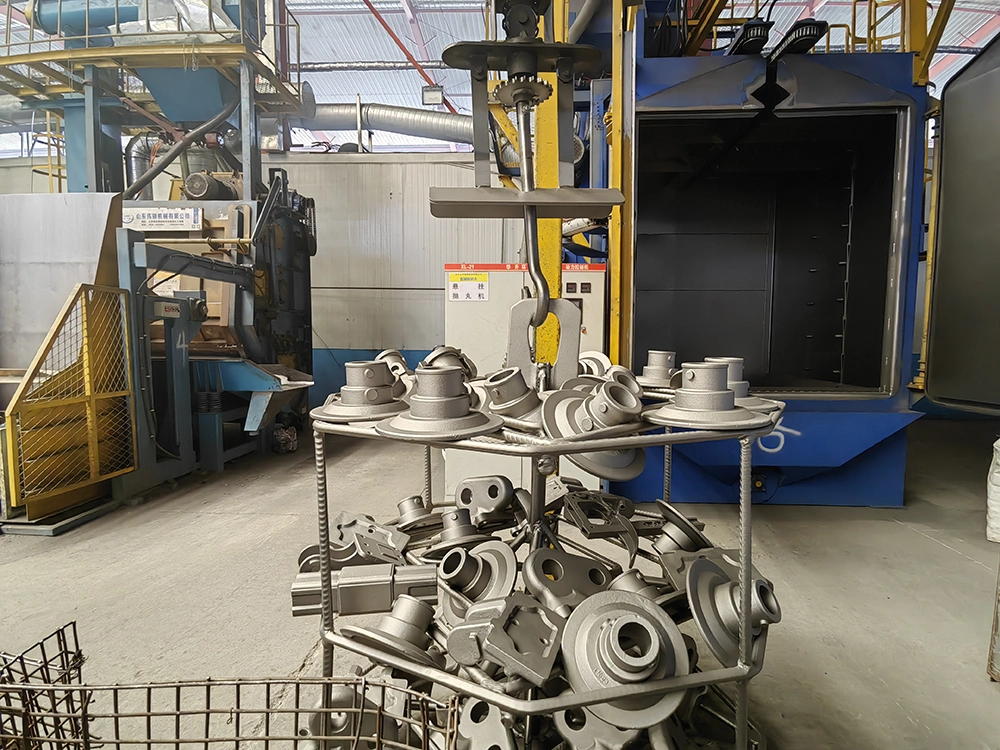
| 4 | Shakeout & fettling | Knockout, runner removal and shot blasting for a clean surface |
| 5 | Heat treatment | Stress-relief annealing for dimensional stability |
| 6 | CNC machining | Rotor bores, bearing seats and sealing faces machined to drawing |
| 7 | Pressure & leak testing | 100% air test on gas and water passages |
| 8 | Final inspection & packing | CMM sampling, anti-rust treatment and seaworthy packing |
Leesh Holdings Sand Casting Service & Process
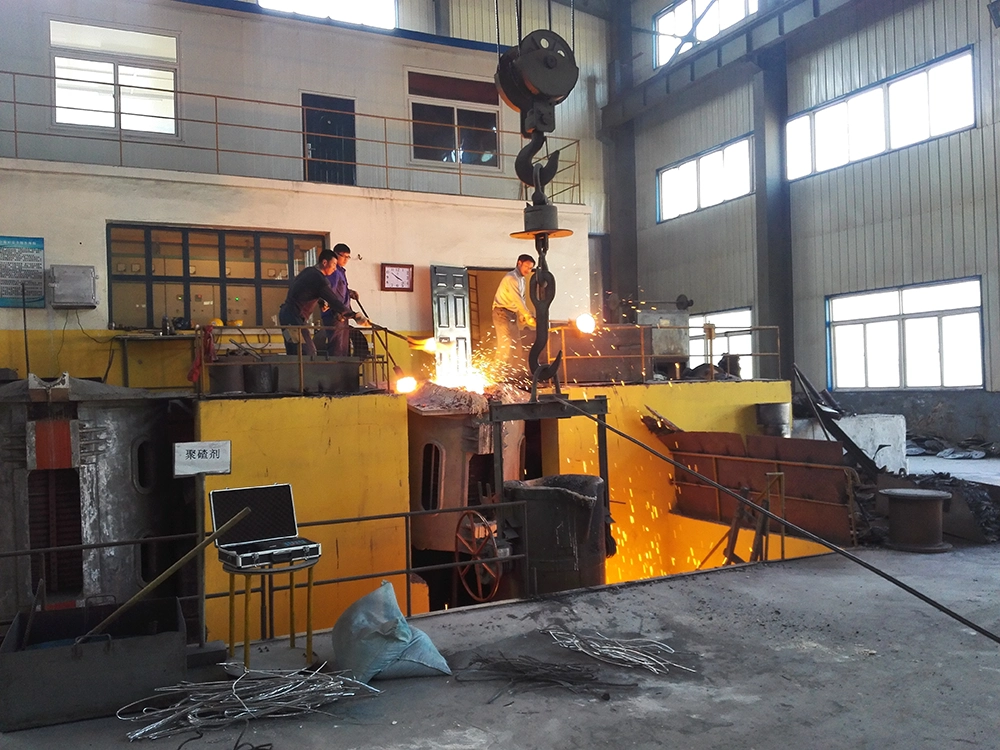
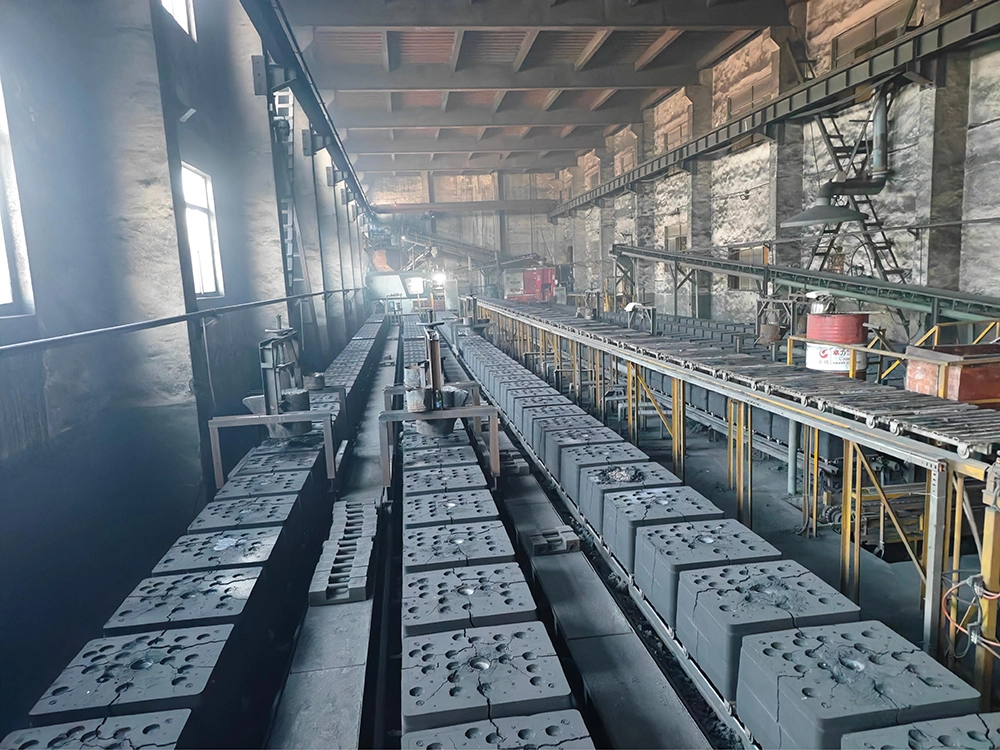
Leesh Holdings runs two automatic casting production lines for iron and steel castings, and sand casting is our most mature process — the same route used for about 80% of all metal castings worldwide. A pattern is made from your drawing first, sand molds and cores form the housing walls and internal cavities, molten iron is poured and solidified in the mold, and the cleaned casting is inspected before machining and delivery.
For compressor cast iron housing casting parts we supply grey iron (ASTM A48 Cl.20–Cl.40 / GG20–GG35) and ductile iron (ASTM A536 60-40-18, 60-42-10, 70-50-05 / GGG40–GGG60) in weights from 0.1 kg to 3,000 kg, produced to ASTM, SAE, AISI, DIN, EN, ISO and GB standards.
- Cost-effective for both prototype and large production runs;
- Suitable for a wide range of metals and alloys;
- Flexible design and size capabilities;
- Shorter lead times for samples and bulk orders.
Typical Applications
Our compressor cast iron housing casting components serve the following markets:
| Application | Typical Castings | Key Requirements |
|---|---|---|
| Centrifugal air & gas compressors | Centrifugal compressor volute casting, inlet casings | Smooth flow channel, airtightness |
| Screw air compressors | Screw compressor housing casting, rotor housings | Bore alignment, dimensional stability |
| Reciprocating compressors | Compressor bearing housing casting, crankcases | Fatigue strength, precise bearing bores |
| Refrigeration & HVAC units | Hermetic and semi-hermetic compressor housings | Pressure tightness, clean internal surface |
| Oil & gas / petrochemical plants | Gas compressor frames and cylinders | Heavy-section integrity, RT/UT examination |
| General industrial equipment | End covers, brackets, valve plates | Cost-efficient volume production |
Quality Control & Testing
Quality is designed into every compressor cast iron housing casting instead of being inspected in afterwards. Chemical composition is verified by spectrometer before pouring, core assembly is photographed for traceability, critical dimensions are measured on CMM, and all gas or water passages are 100% air-tested at 0.6–1.0 MPa. Each shipment comes with a material certificate, dimension report and pressure test report, and third-party inspection by SGS, BV or TÜV is welcome before delivery.
Inside Our Foundry
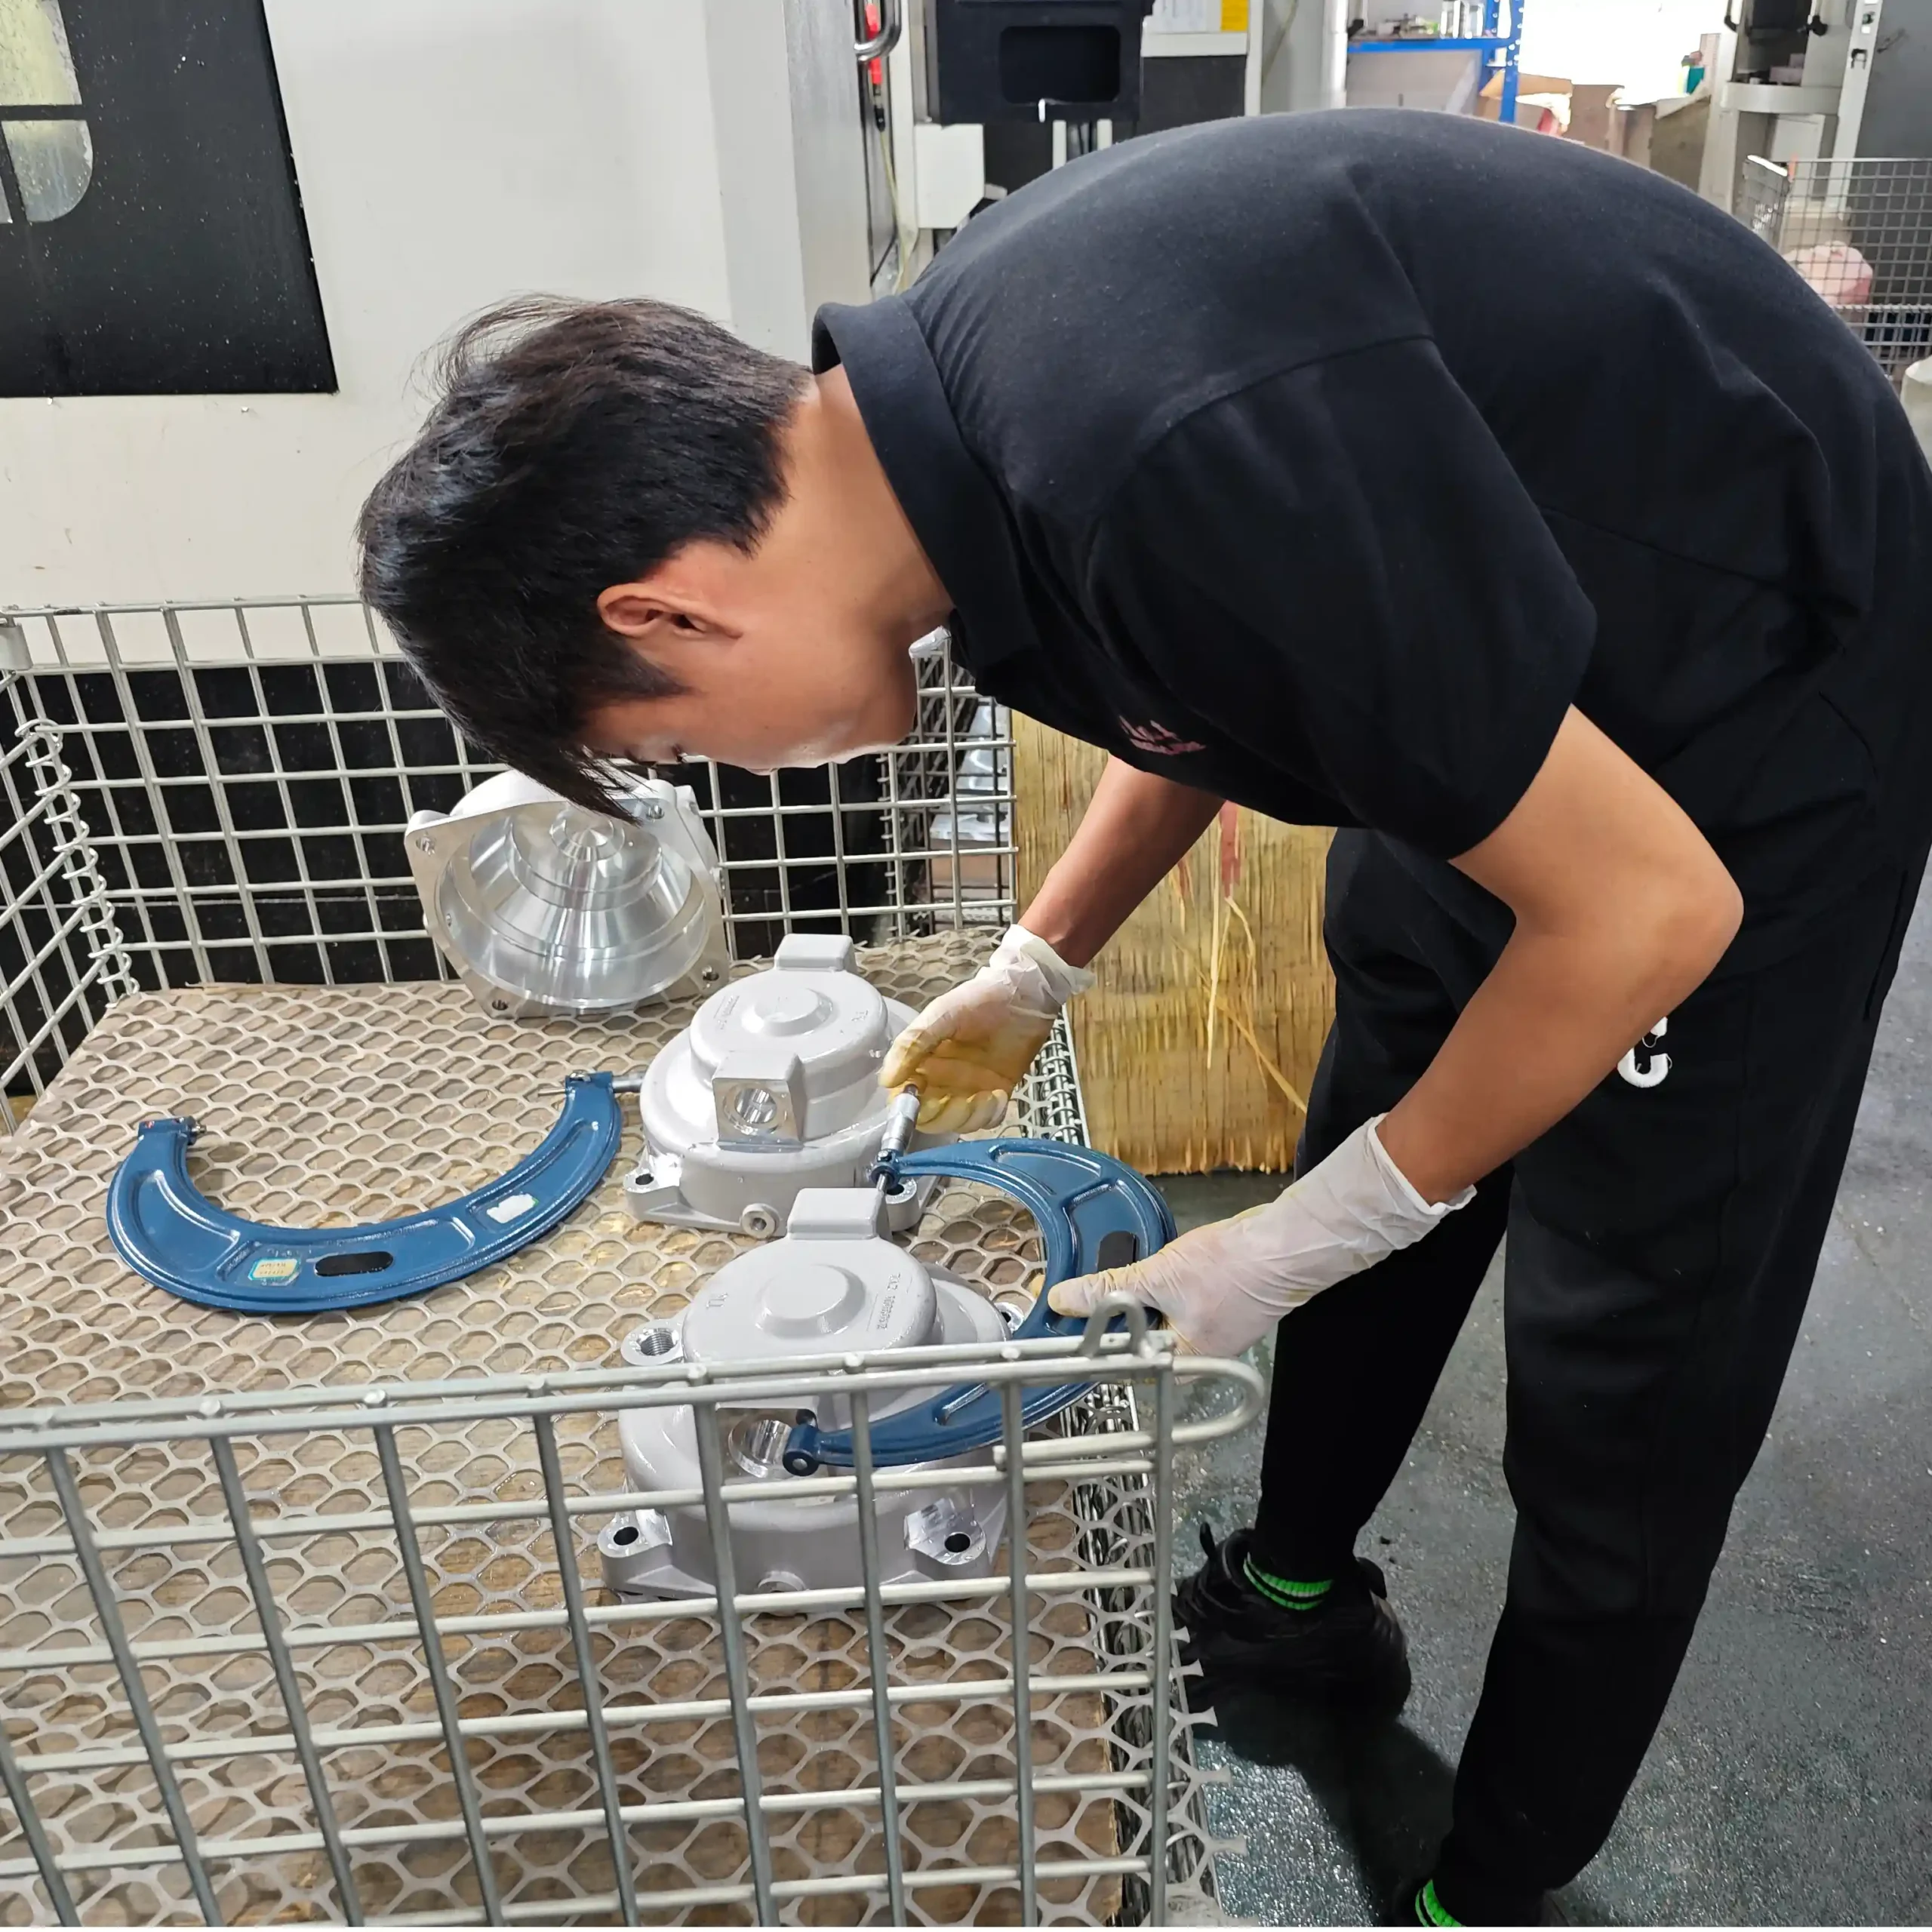
Real production scenes from our ISO 9001:2015 certified casting workshop — melting, molding, machining and inspection under one roof:

Frequently Asked Questions
1. What information do you need to quote a compressor cast iron housing casting?
Please send the 2D drawing with tolerances (PDF) and a 3D model (STEP or IGS) if available, together with the material grade, estimated weight and annual quantity. Our engineers will reply with a casting plan, unit price and lead time within 24–48 hours.
2. What is your MOQ and delivery time?
Sample orders start from 1–10 pieces. Samples are usually delivered 3–5 weeks after drawing confirmation, and batch production takes 4–8 weeks depending on weight and machining scope. Sea, air and express shipping are all supported.
3. Can the housing be fully machined and pressure tested before shipment?
Yes. Boring, drilling, tapping and face milling are completed in our own machining workshop, and every compressor cast iron housing casting with gas or water passages is air-tested before packing. Dimension reports, material certificates and test reports are sent together with the goods.
4. Which material is best for a compressor housing grey iron casting?
HT250 (GG25) grey iron is the most widely used grade thanks to its damping capacity and machinability. For higher pressure or impact loads we recommend HT300 or ductile iron GGG50; our metallurgists will confirm the best grade after reviewing your working conditions.
Request a Quote for Compressor Cast Iron Housing Casting
Share your drawings or sample pictures — our casting engineers will get back to you with price and lead time within 48 hours.
