AS2074 H1A Casting – High Manganese Wear-Resistant Steel Parts
AS2074 H1A casting is the austenitic high-manganese (Hadfield / Mn13-type) steel casting grade defined in Australian Standard AS 2074, supplied by Leesh Holdings as water-toughened wear parts for crushers, grinding mills and mining equipment. In plain terms: it is a cast steel that leaves the quench tank soft and tough, then hardens at the surface under repeated impact — which is exactly why crusher jaw plates and liners last longer when they are made from it. We pour every AS2074 H1A steel casting in resin sand molds from your 2D drawing or 3D model, water-toughen and machine it in-house, and certify chemistry and mechanical properties with a mill test certificate.
Under impact, the working surface of high manganese cast steel hardens from roughly 200 HB as-quenched to more than 500 HB in service, while the core stays tough and crack-resistant — a combination through-hardened steels cannot copy. Because the austenitic structure is non-magnetic, AS2074/H1A castings are inspected with ultrasonic and penetrant methods instead of magnetic particle testing.
AS2074/H1A Casting Specifications
Chemistry of AS 2074 Grade H1A, equivalent to GB 5680 ZGMn13-1:
| Element | Requirement (AS 2074 Grade H1A) |
|---|---|
| Carbon (C) | 1.00 – 1.35% |
| Silicon (Si) | ≤ 1.00% |
| Manganese (Mn) | ≥ 11.0% (typical range 11.0 – 14.0%) |
| Phosphorus (P) | ≤ 0.10% |
| Sulfur (S) | ≤ 0.06% |
Certified heat chemistry is supplied with every mill test certificate; final analysis can be tuned to your working condition.
Typical mechanical properties after water-toughening:
| Property | Typical Delivered Value (water-toughened) |
|---|---|
| Tensile Strength | ≥ 635 MPa |
| 0.2% Yield Strength | ≥ 390 MPa |
| Elongation | ≥ 20% |
| Initial Hardness (as-quenched) | ≤ 230 HB |
| Work-Hardened Surface (in service) | up to ≈ 500 HB |
| Structure | Fully austenitic, non-magnetic |
AS 2074 defines the material standard; the mechanical values above are typical delivered results verified per heat with test bars.
AS2074/H1A Wear Parts Gallery
Typical wear parts cast in AS2074/H1A high manganese steel:

Jaw Crusher Jaw Plate – Mn13
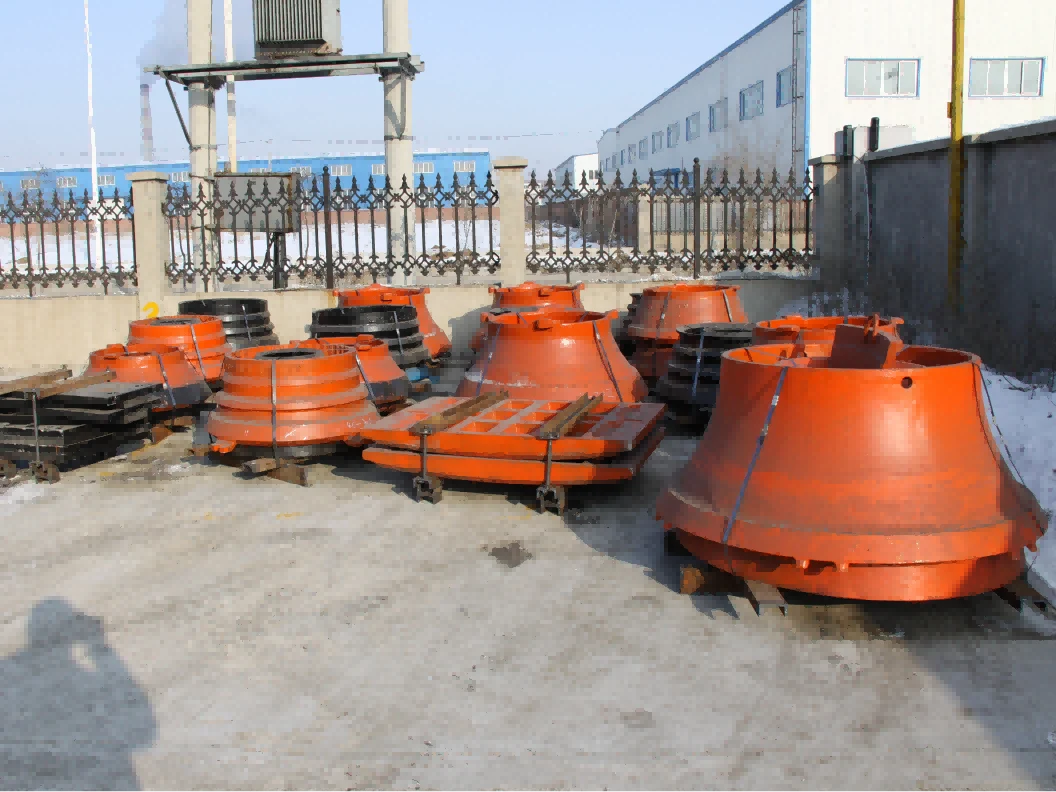
Cone Crusher Liner & Mantle
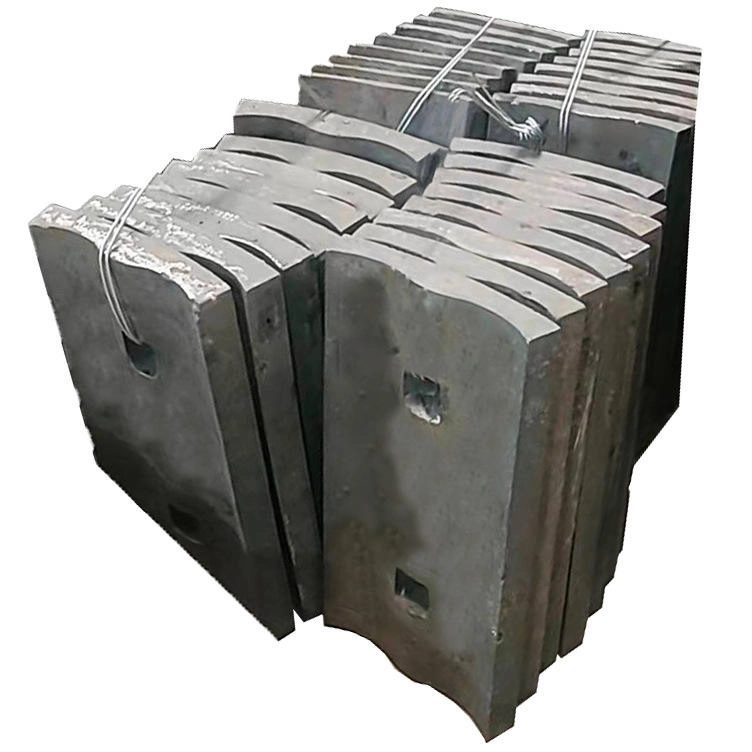
Ball Mill Liner
AS2074/H1A Casting Production Process Flow
Every casting follows the same disciplined workflow; molds are produced on the lines described in our sand casting service:
| No. | Process Step | Key Control Points |
|---|---|---|
| 1 | Pattern & Core Box Making | Pattern built from the customer drawing; shrinkage and machining allowances confirmed by engineers |
| 2 | Sand Molding & Core Setting | Alkali phenolic resin sand or water glass quartz sand molds; cores set for bolt holes and hollow sections |
| 3 | Melting & Pouring | Scrap steel melted in electric furnace; chemistry of every heat checked by spectrometer before pouring |
| 4 | Cooling & Shakeout | Castings cooled in the mold, then shaken out and separated from the running system |
| 5 | Fettling & Grinding | Risers and ingates removed; parting lines and gates ground smooth |
| 6 | Water-Toughening Heat Treatment | Heated to about 1000–1050 °C and quenched in water to restore the tough austenitic structure |
| 7 | CNC Machining | Bolt holes, seats and mating faces machined while the surface is still soft |
| 8 | Inspection & Packing | UT/PT inspection (non-magnetic steel), hardness and dimension checks, MTC issued, seaworthy packing |
Leesh Holdings Sand Casting Craftsmanship
Every AS2074/H1A casting starts from the customer drawing: engineers confirm shrinkage and machining allowances, build the pattern and core boxes, and produce sand molds on Leesh Holdings’ two automatic production lines. Molten high-manganese steel is poured, cooled, shaken out and fettled, then water-toughened and machined — the same disciplined workflow described in detail on our sand casting service page.
For steel castings, Leesh Holdings works with water glass quartz sand, alkali phenolic resin sand and coated resin sand (hot-box and shell molding), producing casting weights from 50 kg to 25,000 kg with CT8–CT12 as-cast tolerance per ISO 8062. Materials are supplied to ASTM, SAE, AISI, ACI, DIN, EN, ISO, GB and AS standards, and the full range of our castings can be browsed on the sand casting products page.
- ✓ 2 automatic sand casting lines for steel and iron castings
- ✓ Resin sand and water glass sand molds up to 25,000 kg
- ✓ In-house water-toughening heat treatment for manganese steel
- ✓ Spectrometer chemistry, test bars, UT/PT and CMM reporting per batch
- ✓ Certification to AS 2074, ASTM A128, GB 5680 or your nominated standard

Melting – Electric Furnace

Resin Sand Molding Line
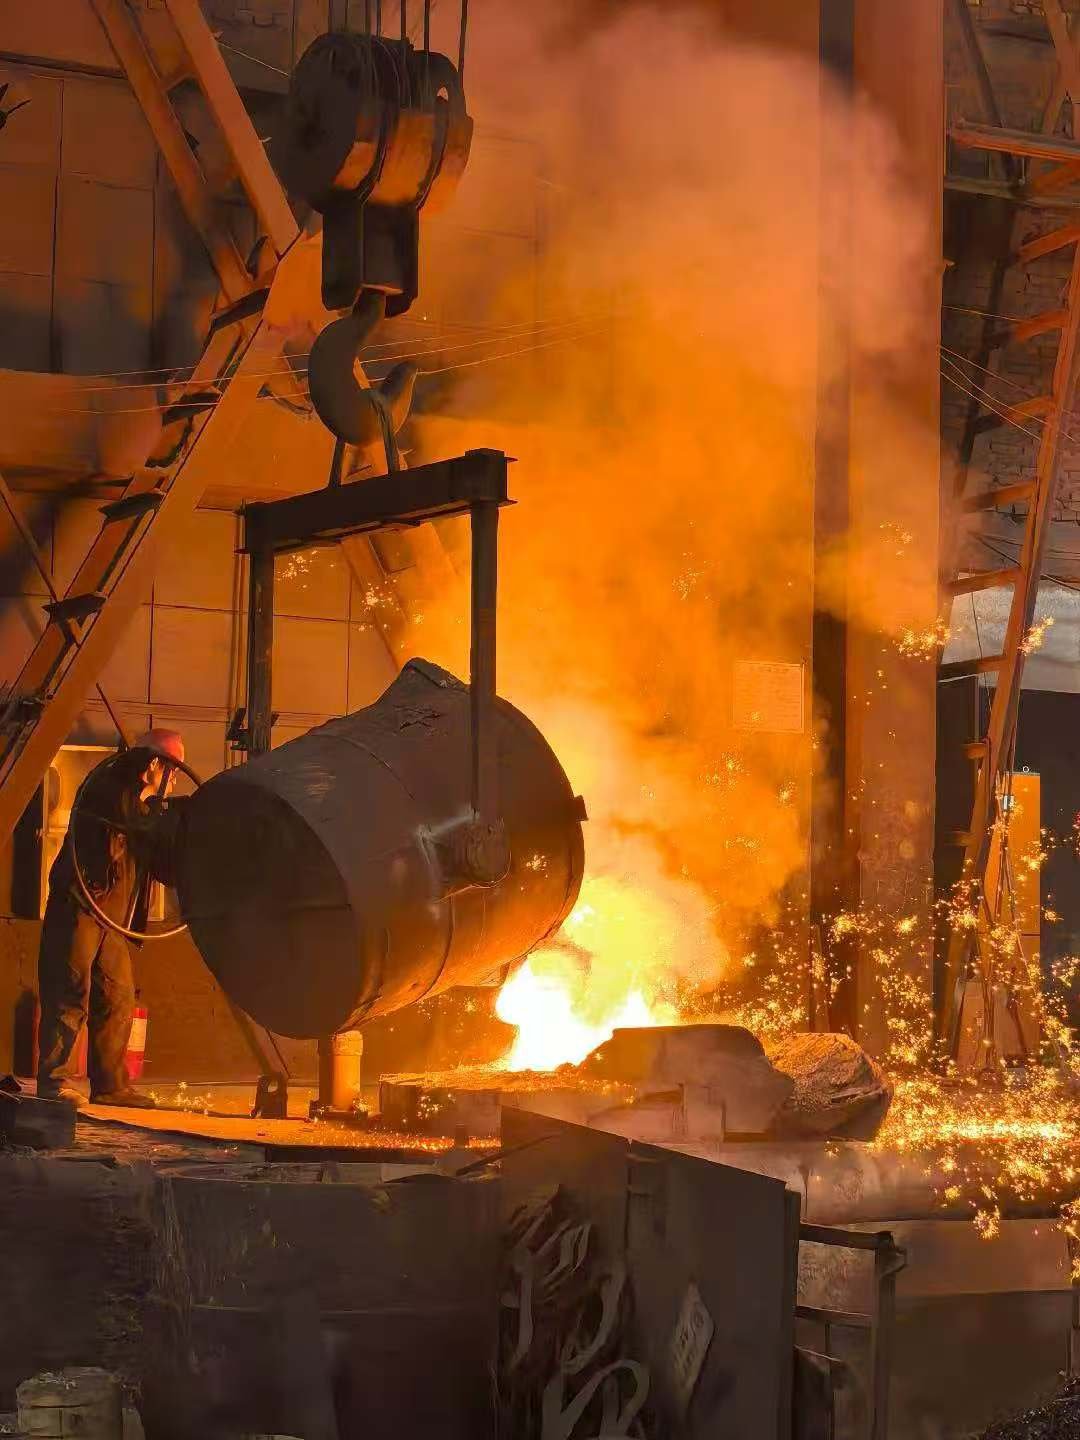
Pouring High Manganese Steel
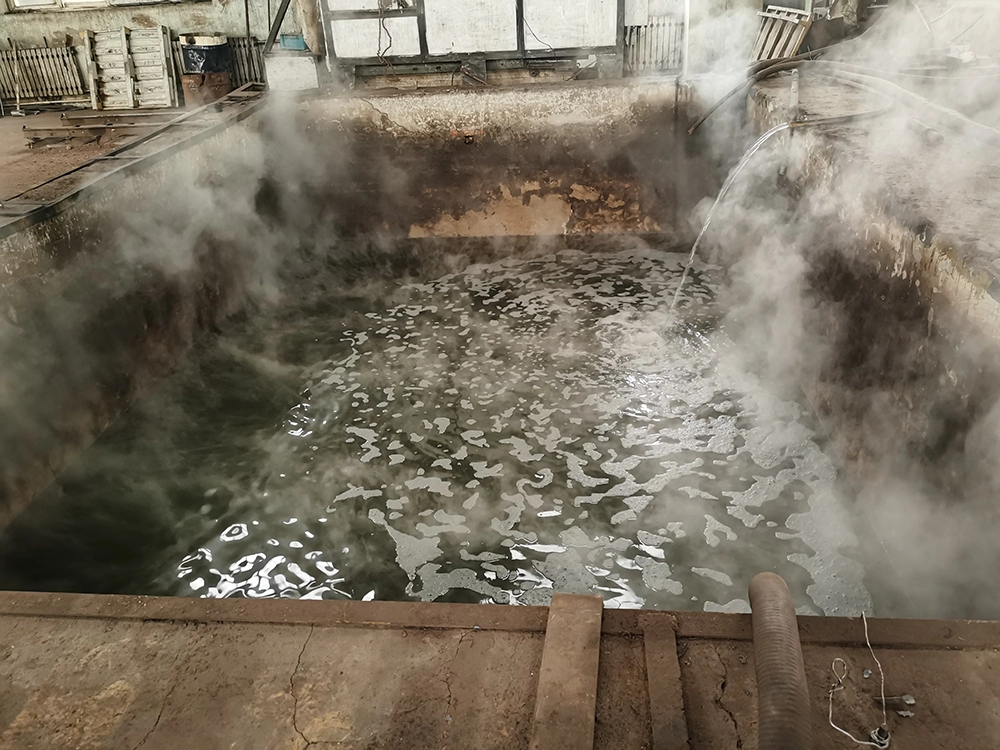
Water-Toughening Quench
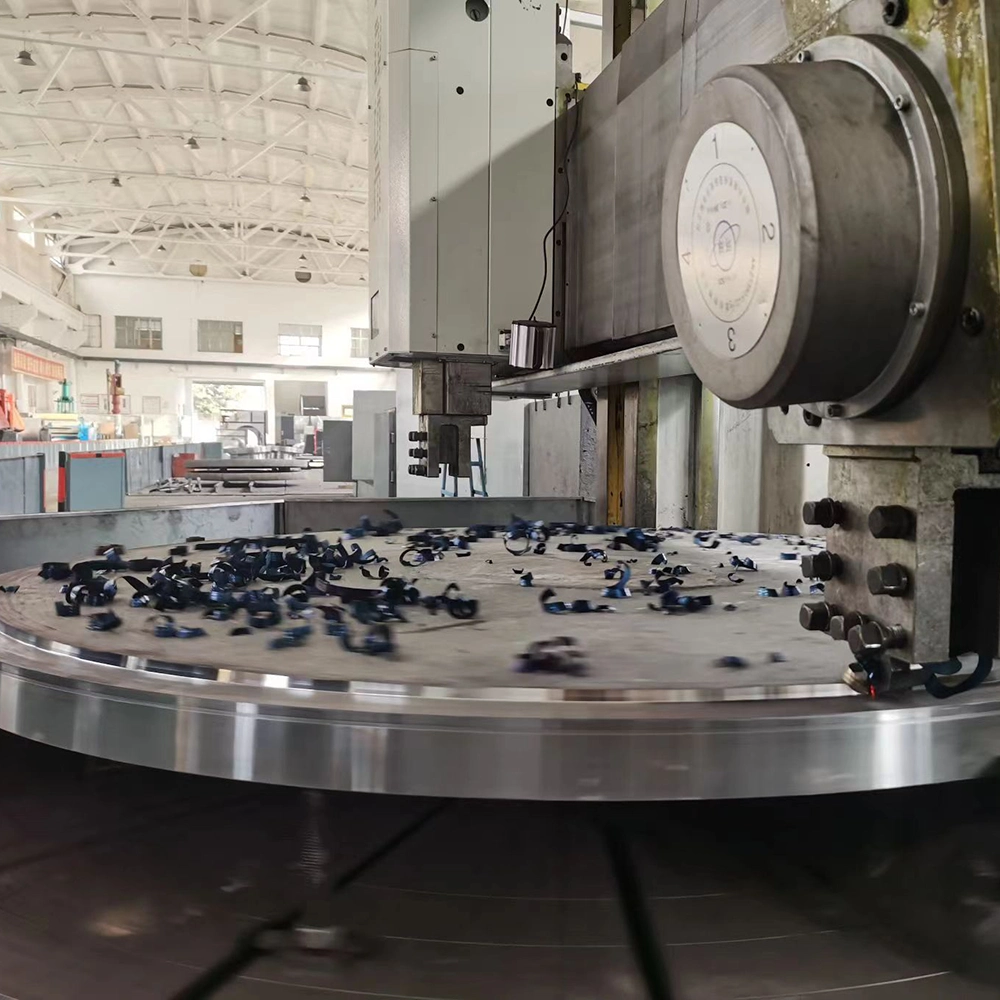
CNC Machining Shop
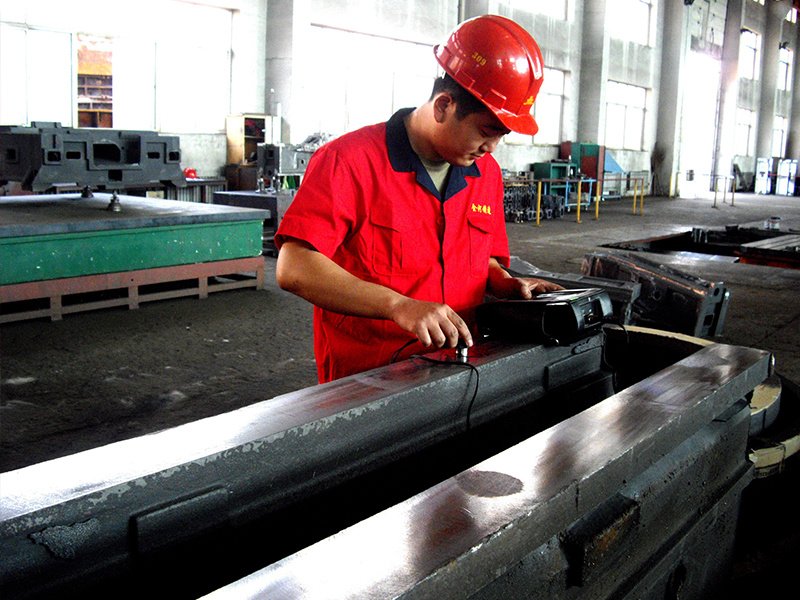
Inspection & Testing
Typical Applications of AS2074/H1A Castings
AS2074/H1A is chosen where impact and abrasion quickly destroy ordinary steels; other steel casting grades are covered on our high strength steel casting page.
| Application Field | Typical Parts | Why AS2074/H1A Works |
|---|---|---|
| Crushing & Screening | Jaw crusher jaw plates, cheek plates | Severe impact and abrasion; the surface work-hardens in service |
| Cone & Gyratory Crushers | Concaves, mantles, step liners | Handles heavy compressive loads without cracking |
| Grinding Mills | Ball mill and rod mill liners, end liners | Continuous impact abrasion with long service life |
| Rail & Track Work | Frogs, crossings, switch castings | Resists rolling-contact wear; tough under cyclic loads |
| Mining & Earthmoving | Track shoes, drive tumblers, shovel parts | Combines impact toughness with abrasion resistance |
AS2074/H1A Casting FAQs
Is AS2074/H1A the same as Mn13?
Yes — AS2074 Grade H1A is the Australian Standard designation for the same austenitic high-manganese (Hadfield) steel that Chinese standards call Mn13 or ZGMn13-1. The chemistry is the classic 1.0–1.35% carbon with 11%+ manganese, water-quenched to a fully austenitic structure. If your drawing calls out Mn13, ASTM A128 or AS2074 H1A, we can cast and certify it to whichever standard you nominate.
What heat treatment does an AS2074/H1A casting require?
Water-toughening (solution treatment) is mandatory. The casting is reheated to about 1000–1050 °C, held until the carbides dissolve, then quenched rapidly in water to lock carbon and manganese into a tough austenitic structure. A skipped or slow quench leaves brittle carbide networks in the grain boundaries, so every AS2074/H1A casting we ship is quenched and hardness-checked before delivery.
Can AS2074/H1A castings be machined?
Yes, but machining must happen in the as-quenched condition while the surface is still soft. We drill liner bolt holes, bore mounting seats and face mating surfaces in our own CNC machining service workshops before the part work-hardens in service. Once a Mn13 surface has hardened under impact, heavy cutting becomes very difficult, which is why all machining scope is confirmed at the drawing stage.
How is a non-magnetic steel casting inspected?
Because austenitic manganese steel is non-magnetic, magnetic particle testing does not work. We inspect AS2074/H1A castings with ultrasonic testing for internal soundness, dye-penetrant testing for surface defects, plus hardness checks and CMM dimensional reports. Spectrometer chemistry and test-bar mechanical results for every heat are compiled into a mill test certificate that travels with the shipment.
What information do you need to quote an AS2074/H1A casting?
Send a 2D drawing (PDF) and a 3D model (STEP/IGES) if available, with the material standard you require, target weight, annual quantity and any machining or heat-treatment notes. Our engineers will reply with casting price, lead time and DFM suggestions, and an NDA can be signed before the technical review. Samples and pilot batches are welcome.
Get a Quote for Your AS2074/H1A Casting Project
Send your drawings to sales@leesh.cn — our engineering team will review the part and reply with casting price, lead time and DFM suggestions.
