Bearing Cover Casting – Custom Gray Iron & Ductile Iron Solutions
Our bearing cover casting service delivers sealing and protection parts for gearboxes, pumps, conveyors and heavy machinery. Each cast bearing cover keeps lubricant inside the housing and keeps dust, water and impact damage out, so your bearings run longer with less downtime.
As an ISO 9001-certified China foundry, we pour gray iron and ductile iron covers from 0.3 kg to 500 kg, machine them to your drawing and ship worldwide with EN 10204 3.1 material certificates. Send us a PDF, DWG or STEP file and you will receive DFM feedback plus a firm quotation within 24-48 hours.
Request a Free Quote Or email us directly: sales@leesh.cn
What Is a Cast Iron Bearing Cover?
A cast iron bearing cover – also called a bearing end cover, bearing cap or housing cover – closes the open side of a bearing housing. It locates the outer ring, retains grease or oil, and shields the rolling elements from contamination. Because most covers are symmetrical, medium-weight parts, sand casting is the most economical production route from prototype batches to large volumes.
We pour every bearing cover casting in-house: medium-frequency induction melting, green sand and furan resin sand molding lines, and a complete CNC machining shop under one roof. Popular grades are ASTM A48 Class 30 gray iron and ASTM A536 65-45-12 ductile iron, with EN-GJL-250 and EN-GJS-400-15 equivalents for European customers. When the housing sees shock loads or vibration, we recommend a ductile iron bearing cover casting instead of gray iron.
All covers are made to drawing, so bolt-hole patterns, sealing grooves, O-ring slots and threaded ports follow your interface exactly.
Bearing Cover Casting Product Gallery
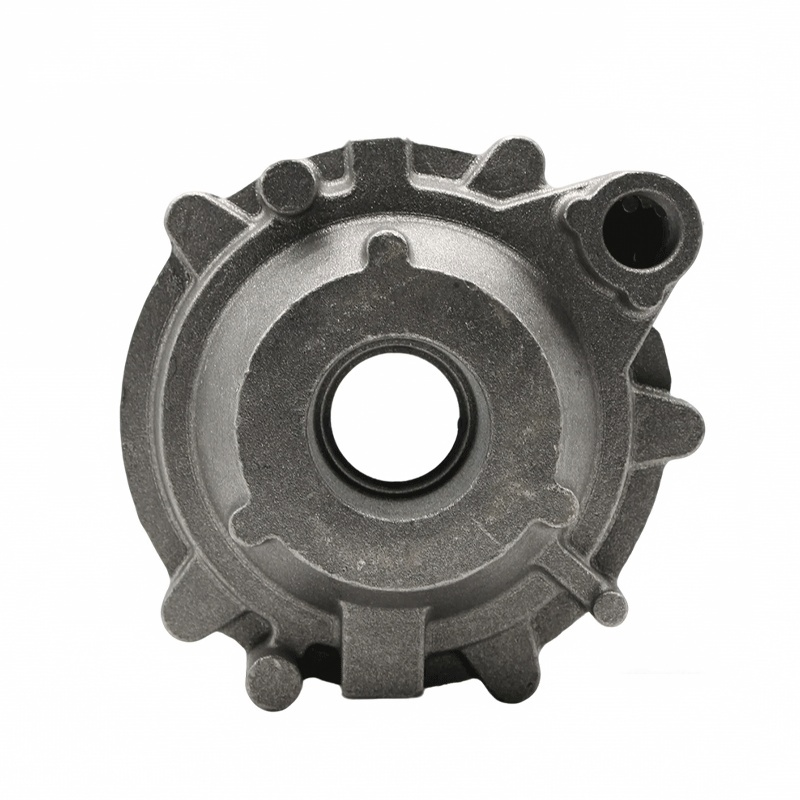
Gray Iron Bearing Cover (As-Cast)
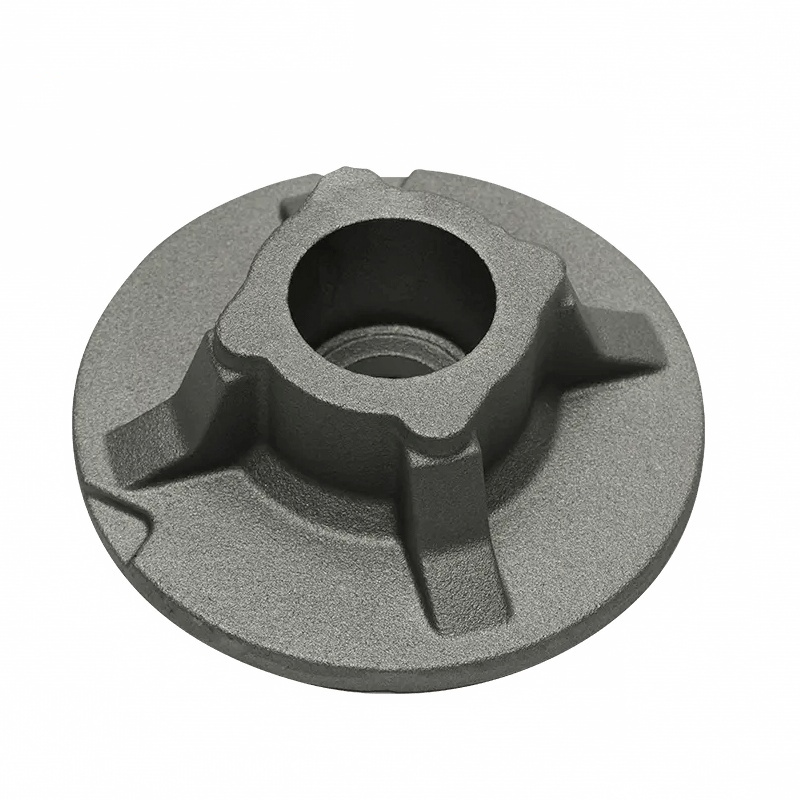
Ductile Iron Bearing Cover
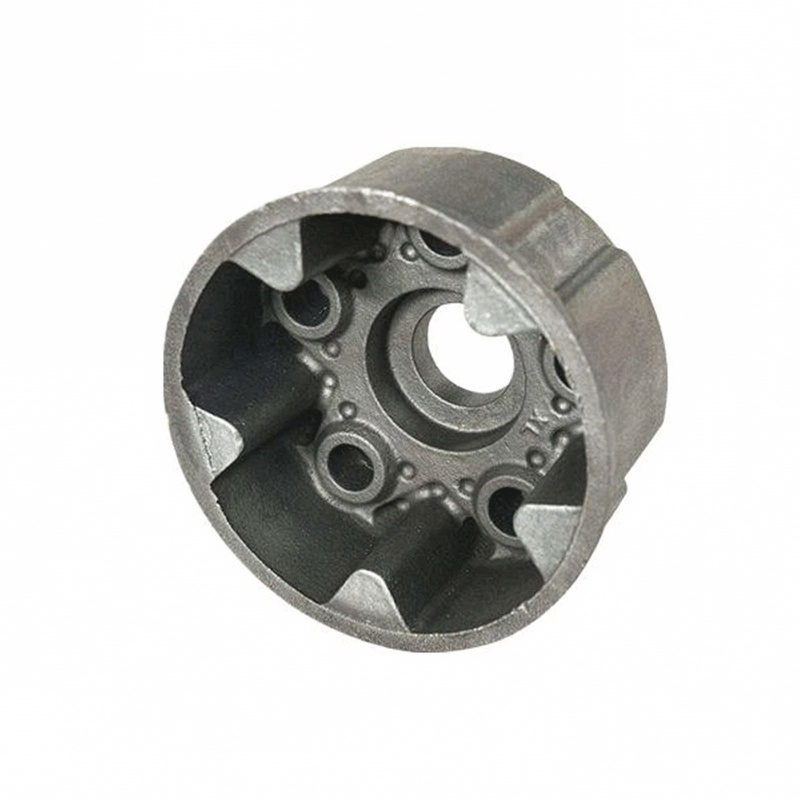
Finished & Painted Cover
Bearing Cover Casting Specifications
The table below lists the standard options for our bearing cover casting; any parameter can be adjusted to match your working conditions.
| Item | Specification Options |
|---|---|
| Product Name | Bearing cover, bearing end cover, bearing cap, housing cover (gray iron & ductile iron) |
| Material Grades | Gray iron: ASTM A48 Class 20 / 30 / 35, EN-GJL-200 / -250, HT150-HT250; Ductile iron: ASTM A536 65-45-12 / 80-55-06, EN-GJS-400-15 / 500-7; other alloys on request |
| Casting Process | Green sand casting, furan resin sand casting, shell molding |
| Weight Range | 0.3-500 kg per piece |
| Size Range | Diameter 50-2,000 mm; minimum wall thickness approx. 6 mm |
| As-Cast Tolerance | ISO 8062 CT11-CT12 (sand casting), CT9-CT10 (shell molding) |
| Machining | CNC turning, milling, drilling and tapping; sealing face Ra 1.6-3.2 um |
| Heat Treatment | Stress-relief annealing; normalizing on request |
| Surface Treatment | Shot blasting to Sa 2.5; water-based paint, powder coating or anti-rust oil |
| Inspection | Spectrometer analysis, CMM dimension report, hardness test, ultrasonic test, air-pressure leak test |
| Custom Options | Cast-in logo and part number, threaded ports, O-ring grooves, paint color per RAL |
| MOQ & Lead Time | Flexible MOQ; samples in 20-30 days, serial production in 30-45 days |
Bearing Cover Sand Casting Process Flow
Every bearing cover casting moves through nine controlled steps. Our green sand line handles small and medium batches while the furan resin sand line produces large-diameter covers, so each sand cast bearing cover keeps stable dimensions from the first sample to the last shipment.
| Step | Process | Key Control Points |
|---|---|---|
| 1 | Drawing & DFM Review | Material grade, tolerances and machining allowance confirmed within 24-48 hours |
| 2 | Pattern Making | Wood, resin or aluminum pattern with shrinkage set per grade |
| 3 | Molding & Core Making | Green sand or furan resin sand molds; resin-coated sand cores for bores and windows |
| 4 | Melting & Pouring | Induction furnace with spectrometer control; pouring temperature logged for every heat |
| 5 | Cooling & Shakeout | Controlled cooling in the mold; shakeout with sand reclamation |
| 6 | Fettling & Blasting | Gates and risers removed, joints ground smooth, shot blasting to Sa 2.5 |
| 7 | Heat Treatment | Stress-relief annealing for dimensional stability |
| 8 | CNC Machining | Face turning, boring, drilling and tapping; sealing face finished to Ra 1.6-3.2 um |
| 9 | Inspection & Packing | CMM report, hardness test, protective coating, export plywood case with heat numbers |
Our Foundry and Equipment
Take a look inside our ISO 9001-certified factory – melting, molding, machining and inspection all happen in-house.
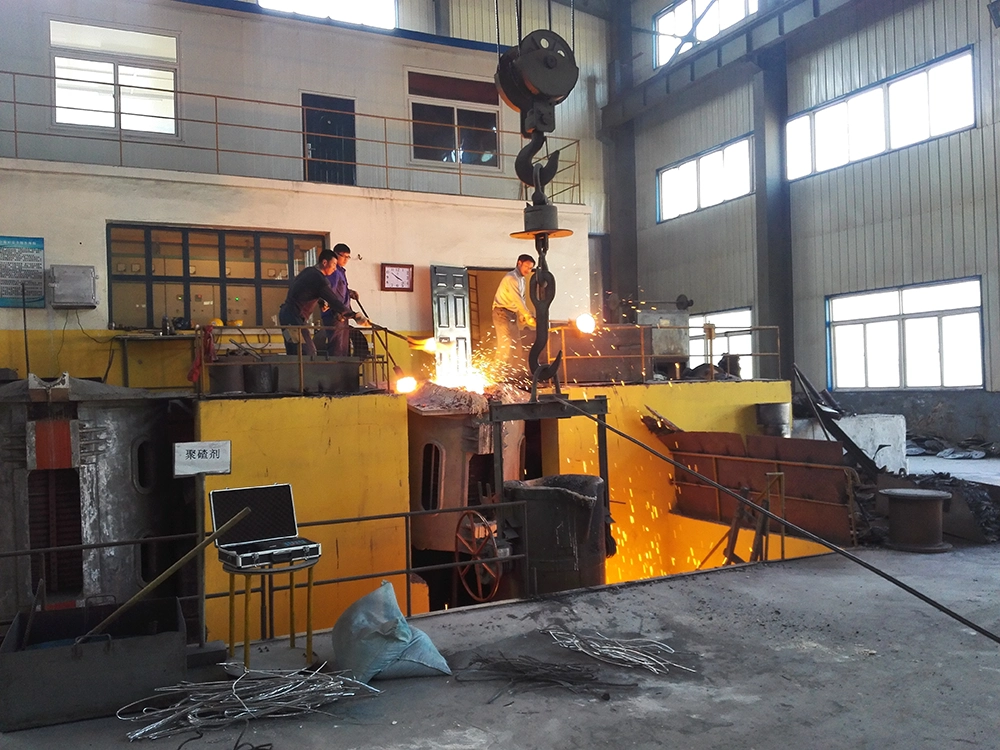
Induction Melting
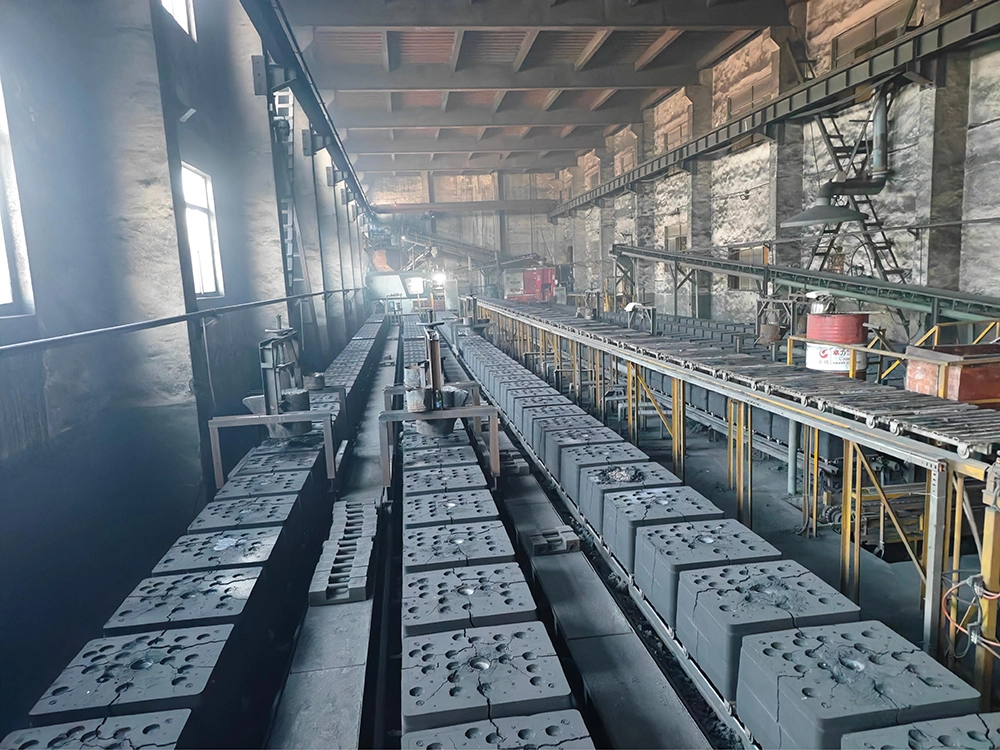
Sand Molding Line
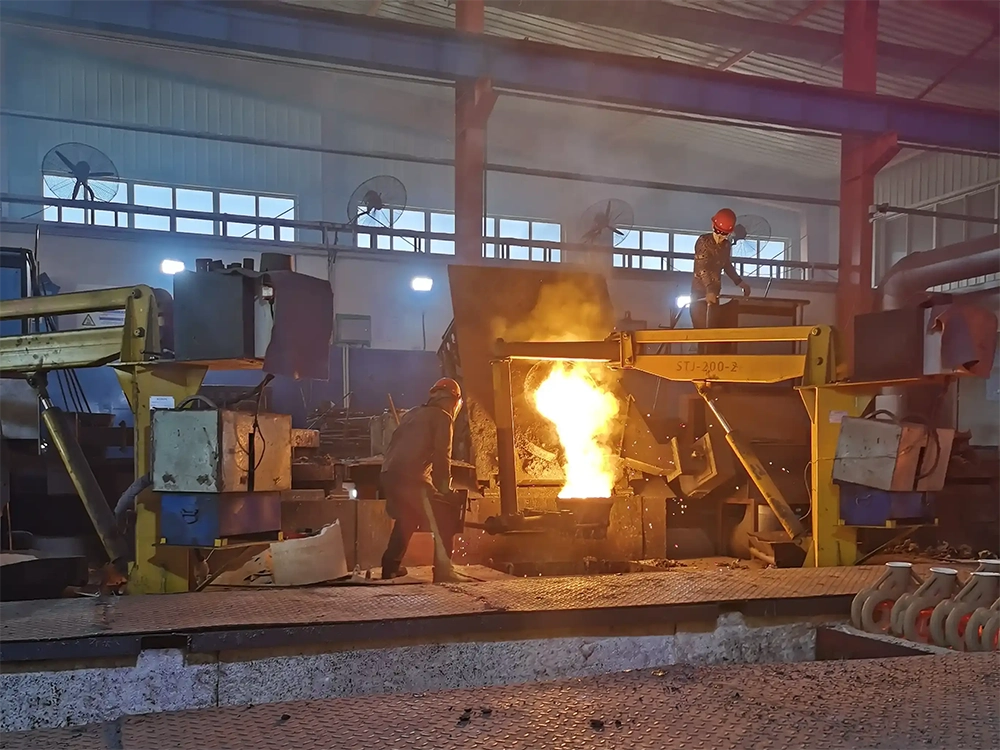
Molten Iron Pouring
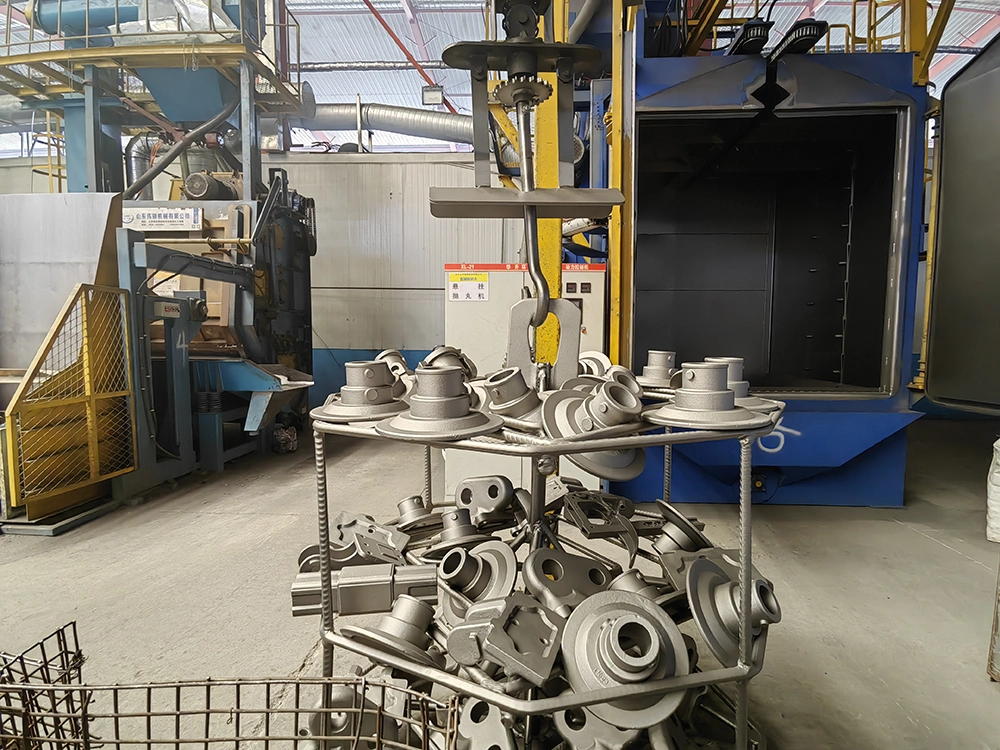
Shot Blasting
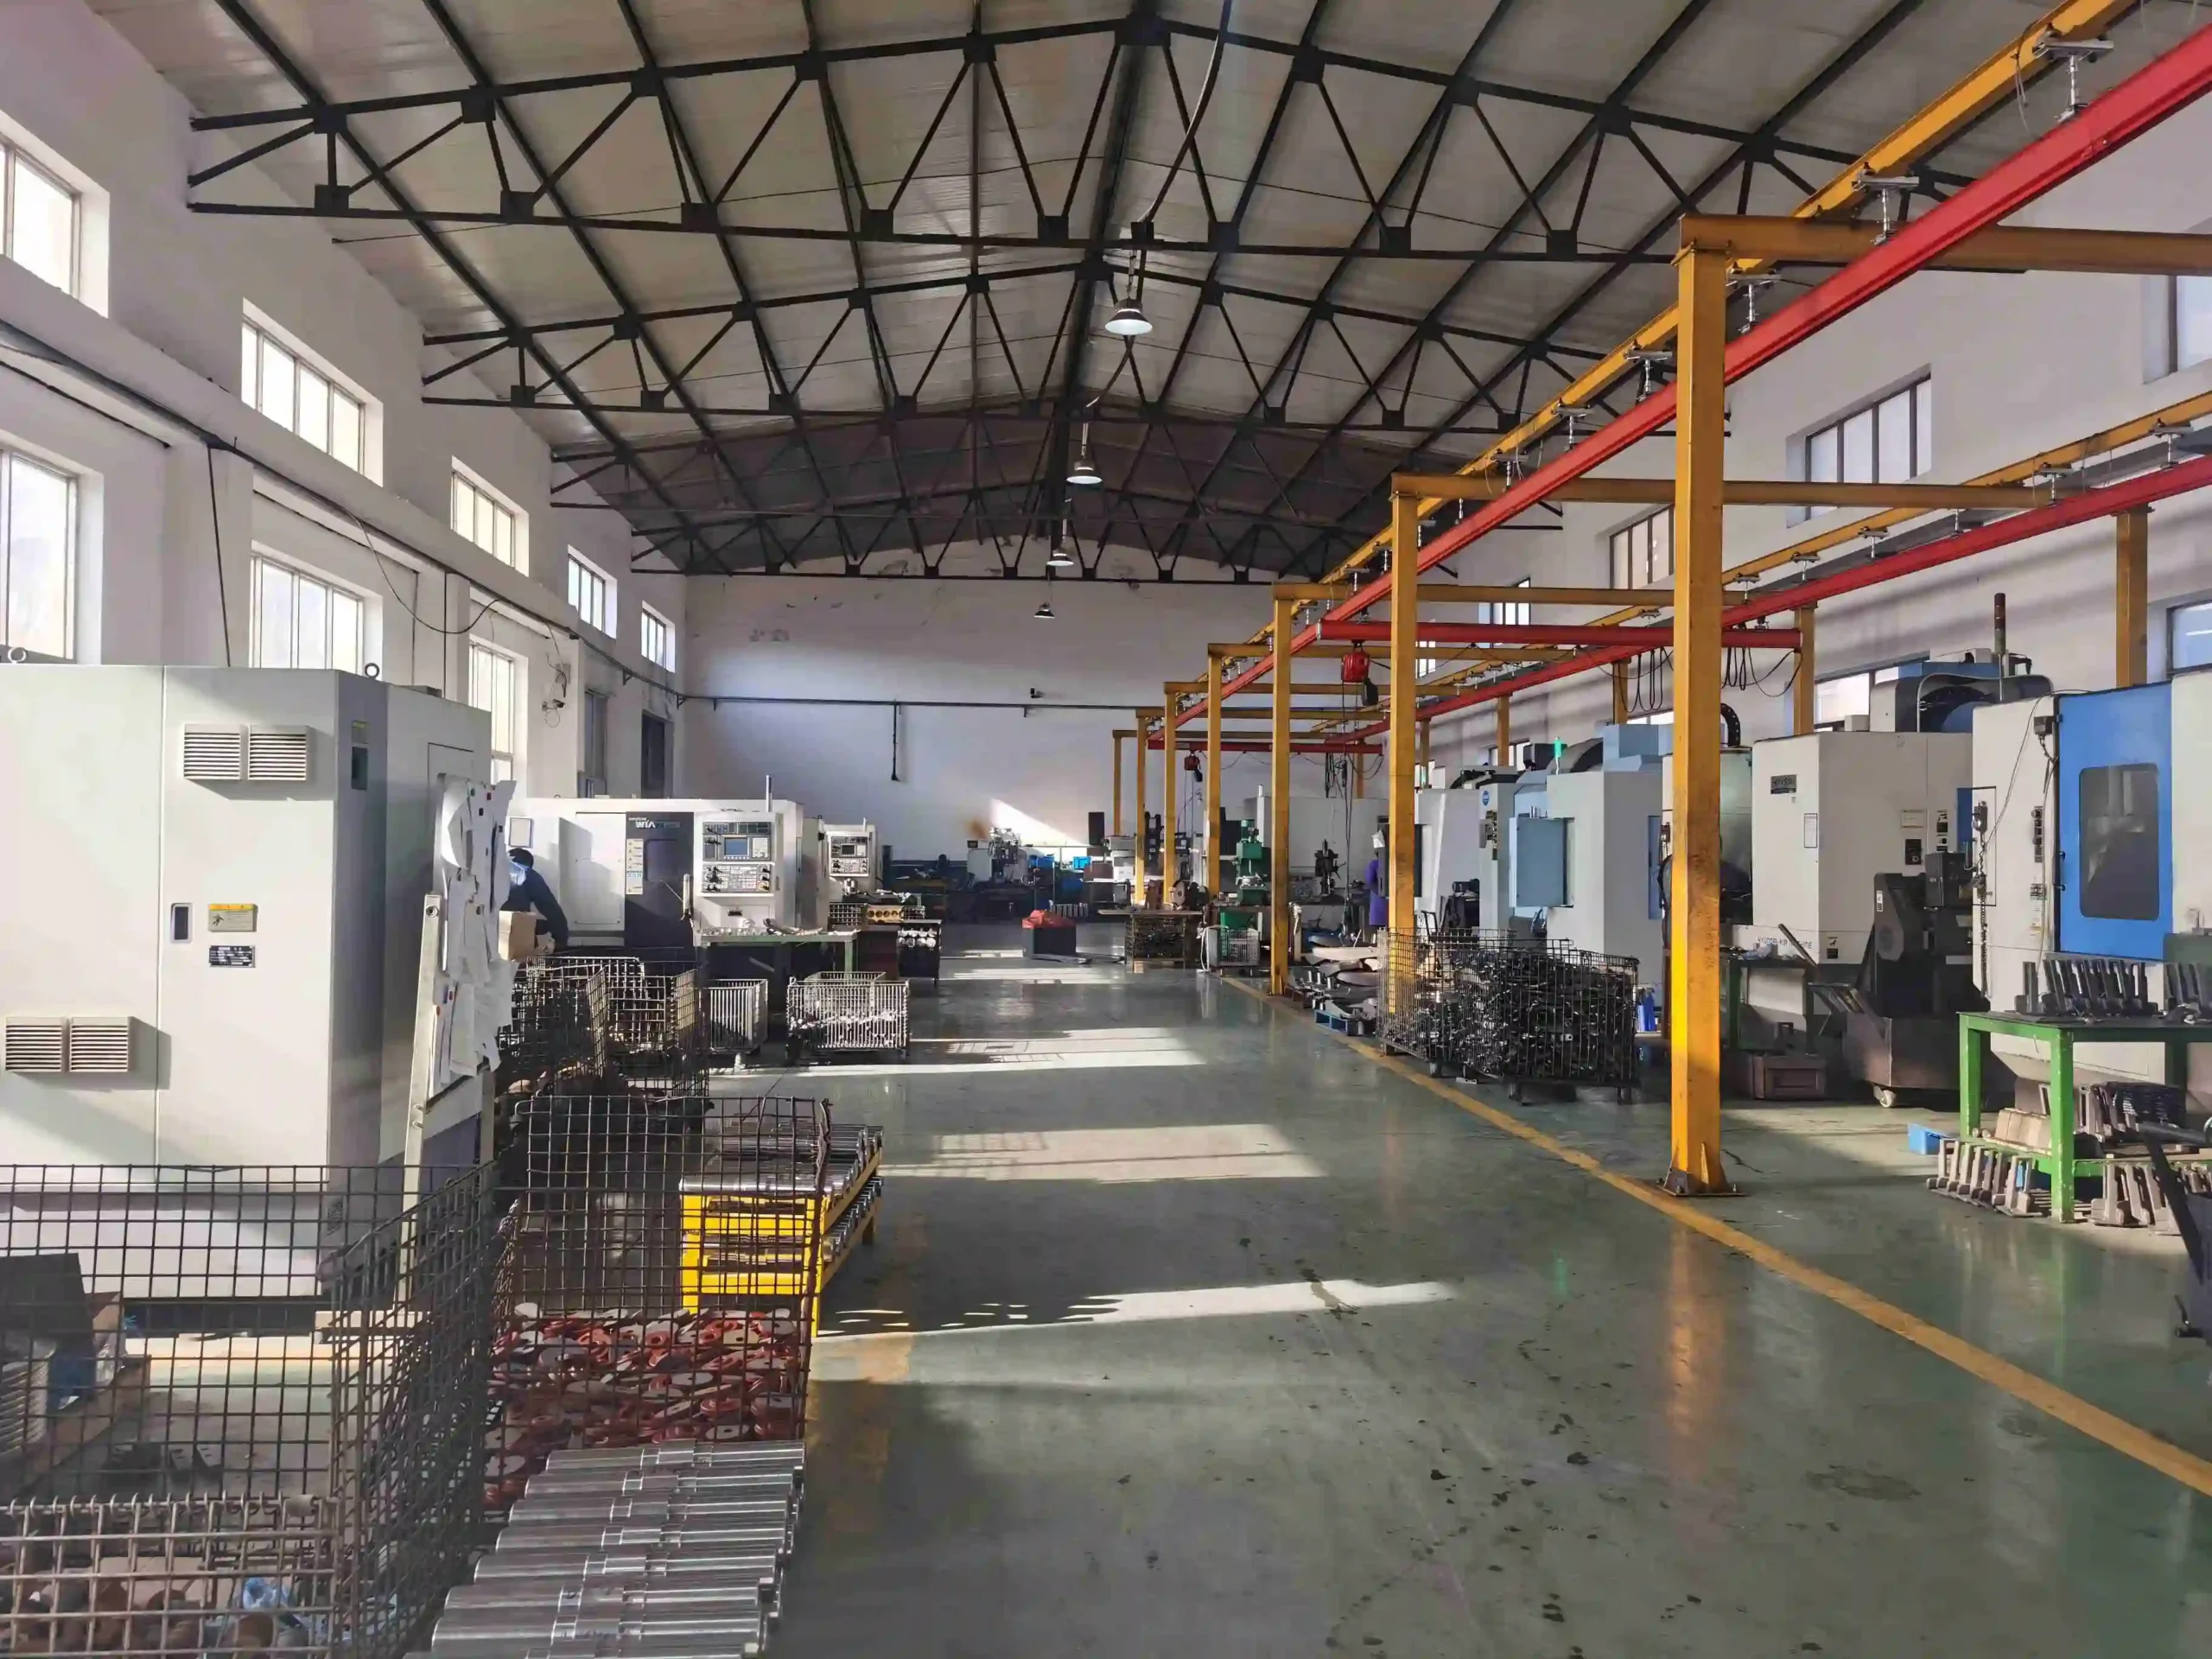
CNC Machining
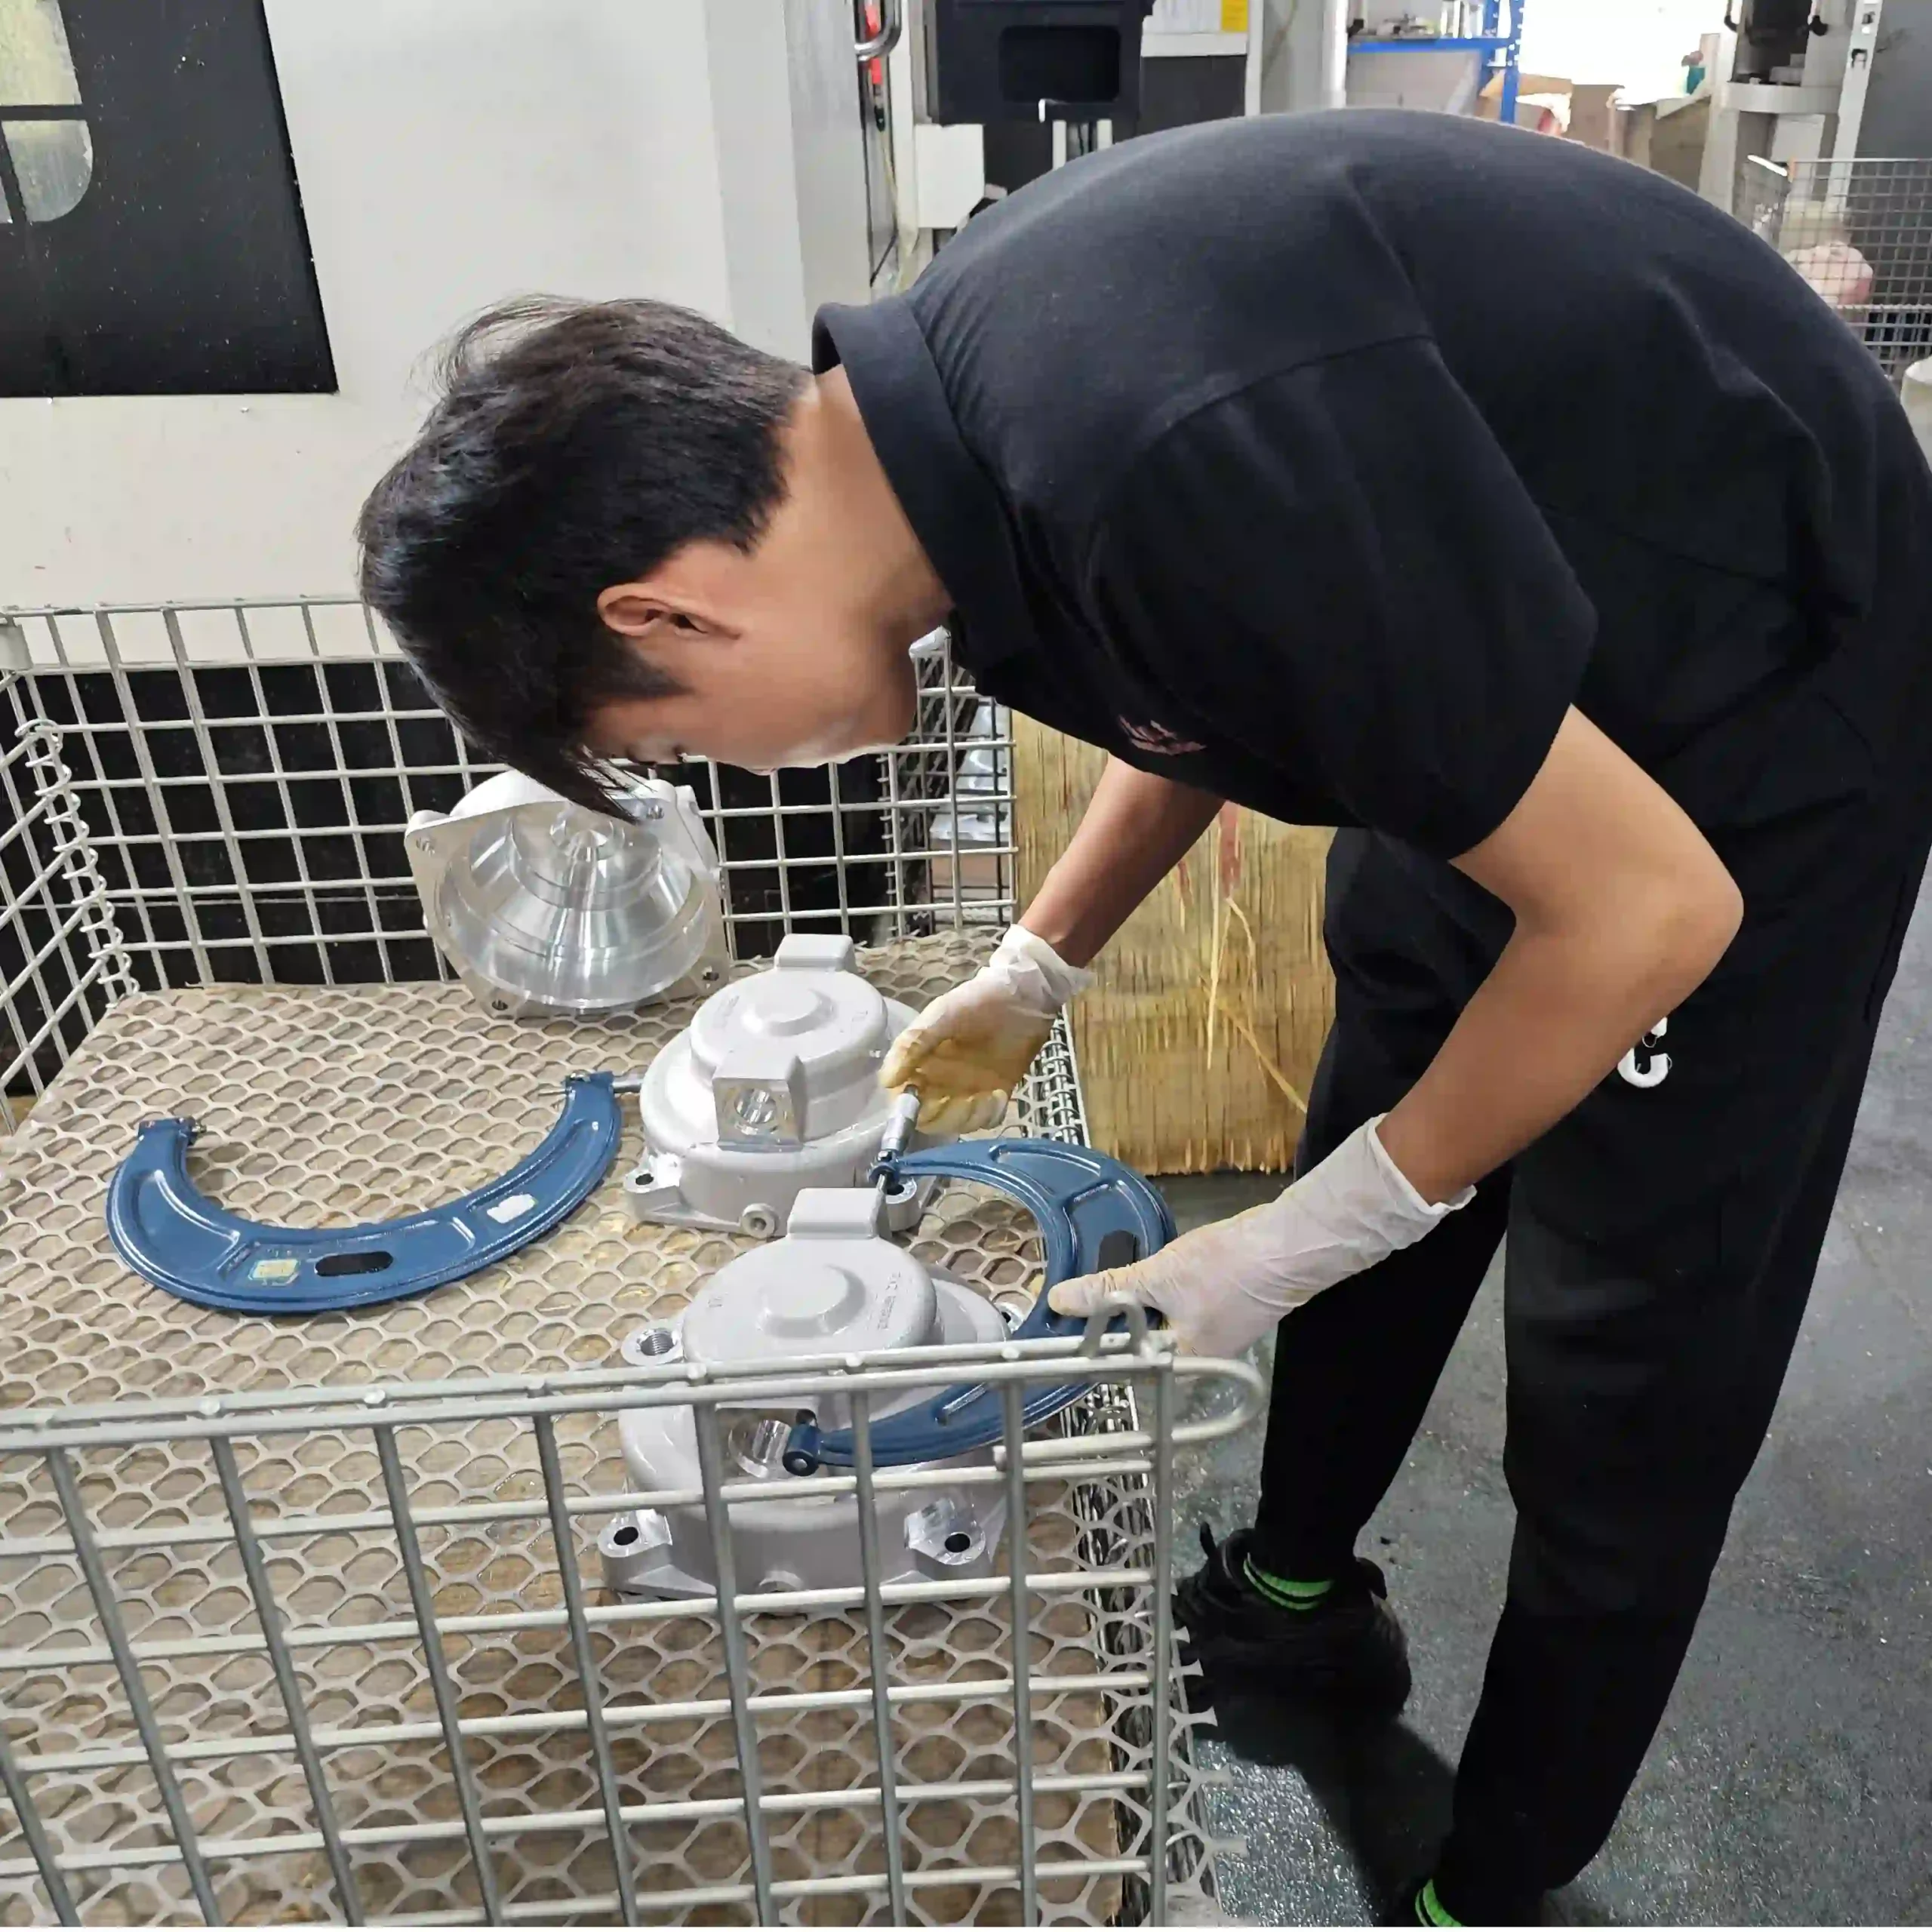
Quality Inspection
Application Scenarios
Bearing cover castings serve any machine where a rotating shaft needs sealing, locating and protection – from farm tractors to cement plants.
| Industry | Typical Parts | What the Cover Does |
|---|---|---|
| Gearboxes & Speed Reducers | Bearing end covers, bearing caps, inspection covers | Retain oil or grease and locate the bearing outer ring |
| Pumps, Compressors & Valves | Pump housing covers, bearing brackets, gland covers | Support the shaft seal and block water and dust |
| Mining, Cement & Conveyors | Pulley bearing covers, idler covers, crusher housings | Resist impact and abrasive dust on heavy-load sites |
| Agriculture & Construction Machinery | Axle hub covers, wheel bearing caps | Keep out mud, stones and wash-down water |
| Wind Power & Metal Processing | Large slew-bearing covers, mill and roller housings | Give weather protection for slow, heavily loaded bearings |
| Rail & Marine | Axle-box covers, shaft coupling covers | Provide corrosion-resistant sealing in harsh climates |
Quality Control and Certification
Each bearing cover casting is inspected against your drawing before it leaves the factory.
- Each ASTM A48 bearing cover casting is poured with attached test coupons, and hardness plus tensile results are recorded heat by heat.
- CMM dimensional reports cover machined sealing faces, pilot diameters and bolt-hole patterns.
- Optional testing: ultrasonic inspection, air-pressure leak testing and coating thickness measurement.
- Every order ships with an EN 10204 3.1 material certificate and full heat-number traceability.
Frequently Asked Questions
1. How do I get a quote for a custom cast bearing cover?
Send your drawing in PDF, DWG, STEP or IGS format to sales@leesh.cn together with material grade, quantity and machining requirements. Our engineers reply with DFM feedback and a firm price within 24-48 hours.
2. Which materials and standards can you pour?
The most common bearing cover casting materials are gray iron to ASTM A48 Class 20 / 30 / 35 and ductile iron to ASTM A536 65-45-12 / 80-55-06; EN-GJL, EN-GJS and GB/T grades are also available. If you are not sure which alloy suits your load case, our engineers will advise.
3. What is your MOQ and delivery time?
MOQ is flexible – one-piece samples and low-volume orders are welcome. Samples of your bearing cover casting need 20-30 days including pattern making, and serial production ships in 30-45 days.
4. Can you machine and coat the covers before shipment?
Yes. CNC turning, drilling and tapping produce the sealing face and bolt holes to your drawing, while shot blasting with water-based paint or powder coating protects the finished cover in transit.
5. Which casting process is best for my project?
For most projects a sand cast bearing cover is the most economical route, and shell molding improves surface finish and tolerance on smaller covers. We confirm the process after reviewing your drawing.
Send Us Your Drawing for a Fast Bearing Cover Casting Quote
DFM feedback, firm pricing and a production schedule within 24-48 hours.
Request a Free Quote Or email: sales@leesh.cn
