Cylinder Block Casting for Engines & Mining Machinery
Cylinder Block Casting is one of the core capabilities of Leesh Holdings, a privately owned foundry group located in Shenyang, the heavy industry center of China. We produce every cast cylinder block in gray iron or ductile iron directly from your 2D drawings or 3D models. From pattern making and resin sand molding to CNC machining and final inspection, every sand casting cylinder block is completed under one roof — stable quality, shorter lead times and competitive factory prices.
What Is Cylinder Block Casting?
Cylinder block casting is the process of pouring molten cast iron into a sand mold that reproduces the engine or machine housing, so the water jackets, oil galleries, bores and mounting bosses are already formed in the as-cast part. Compared with fabricated steel housings, a cast iron cylinder block gives better vibration damping, higher wear resistance and lower cost in volume production. Using green sand and resin sand processes, Leesh Holdings casts gray iron and ductile iron blocks from 0.1 kg up to 3,000 kg, then machines the critical faces and bores to the tolerances on your drawing.
Cast Cylinder Block Products
Typical cast cylinder block castings produced and machined in our foundry:
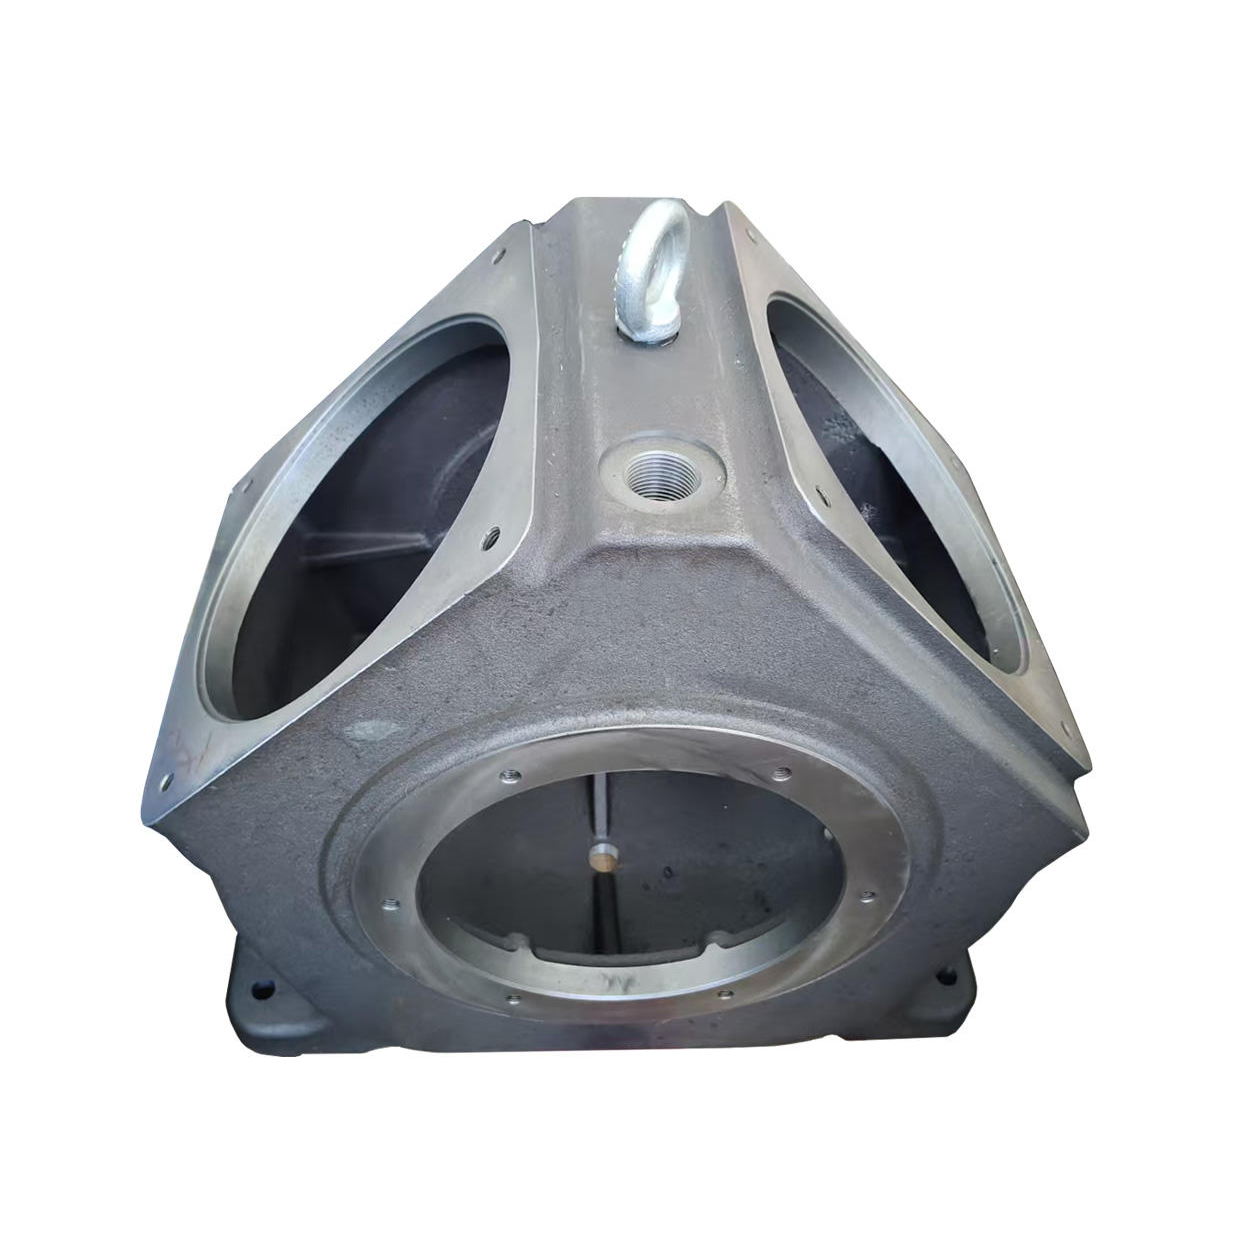
Gray Iron Engine Cylinder Block
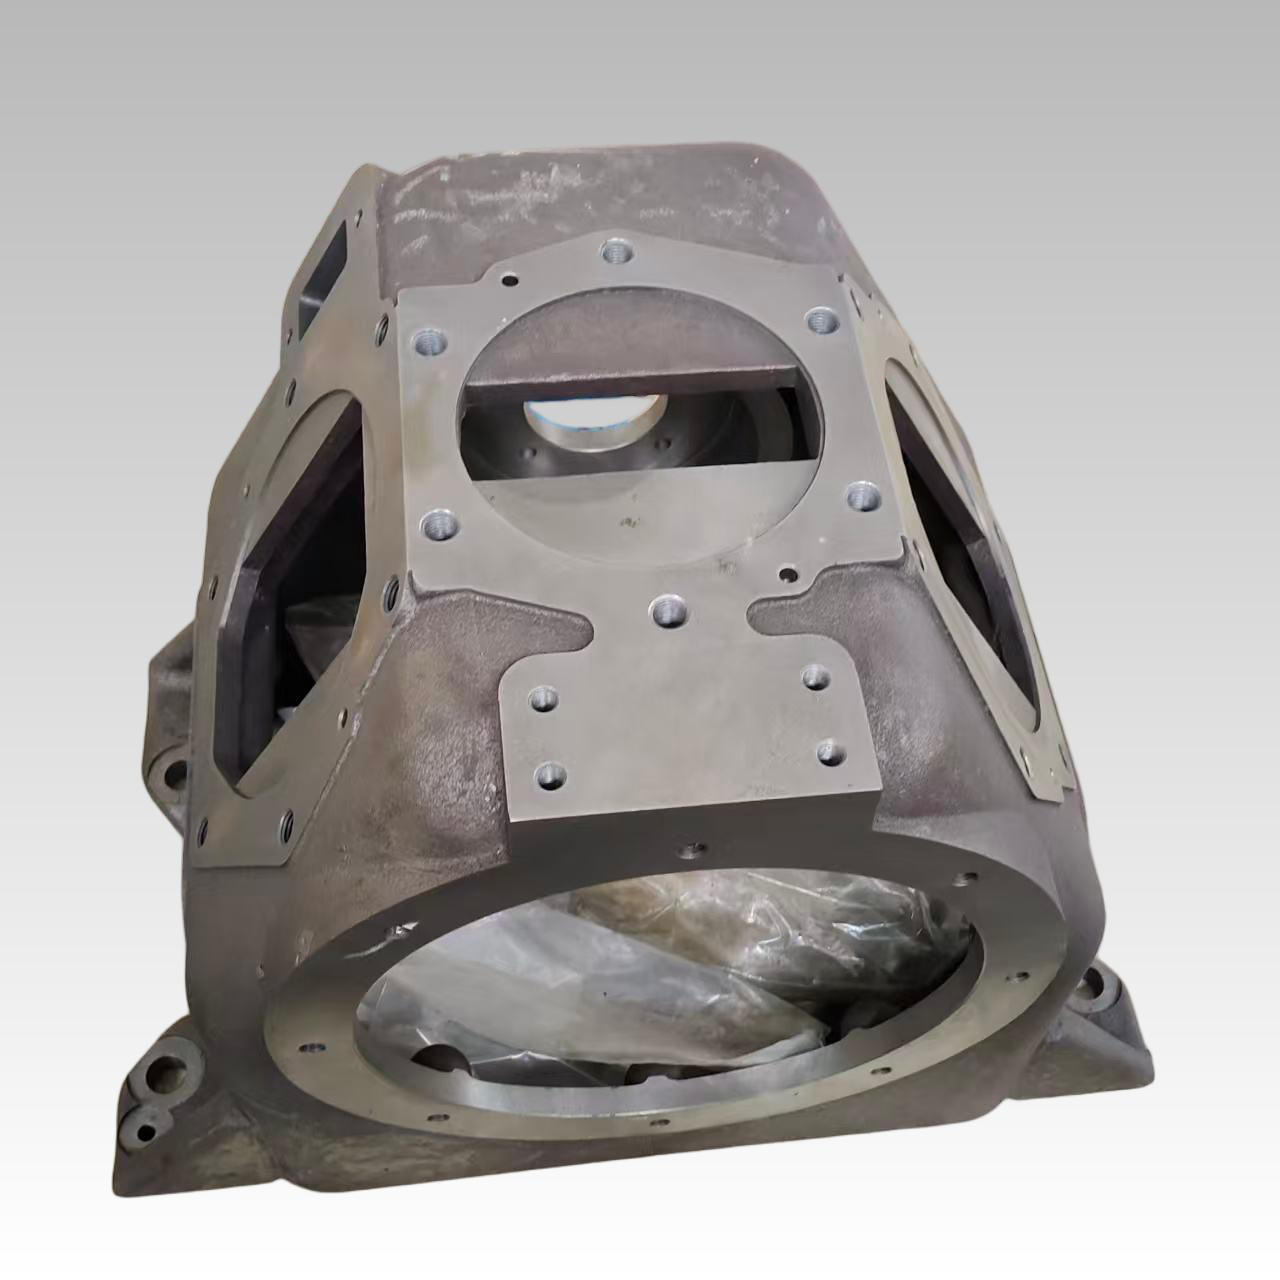
Ductile Iron Block for Heavy Machinery
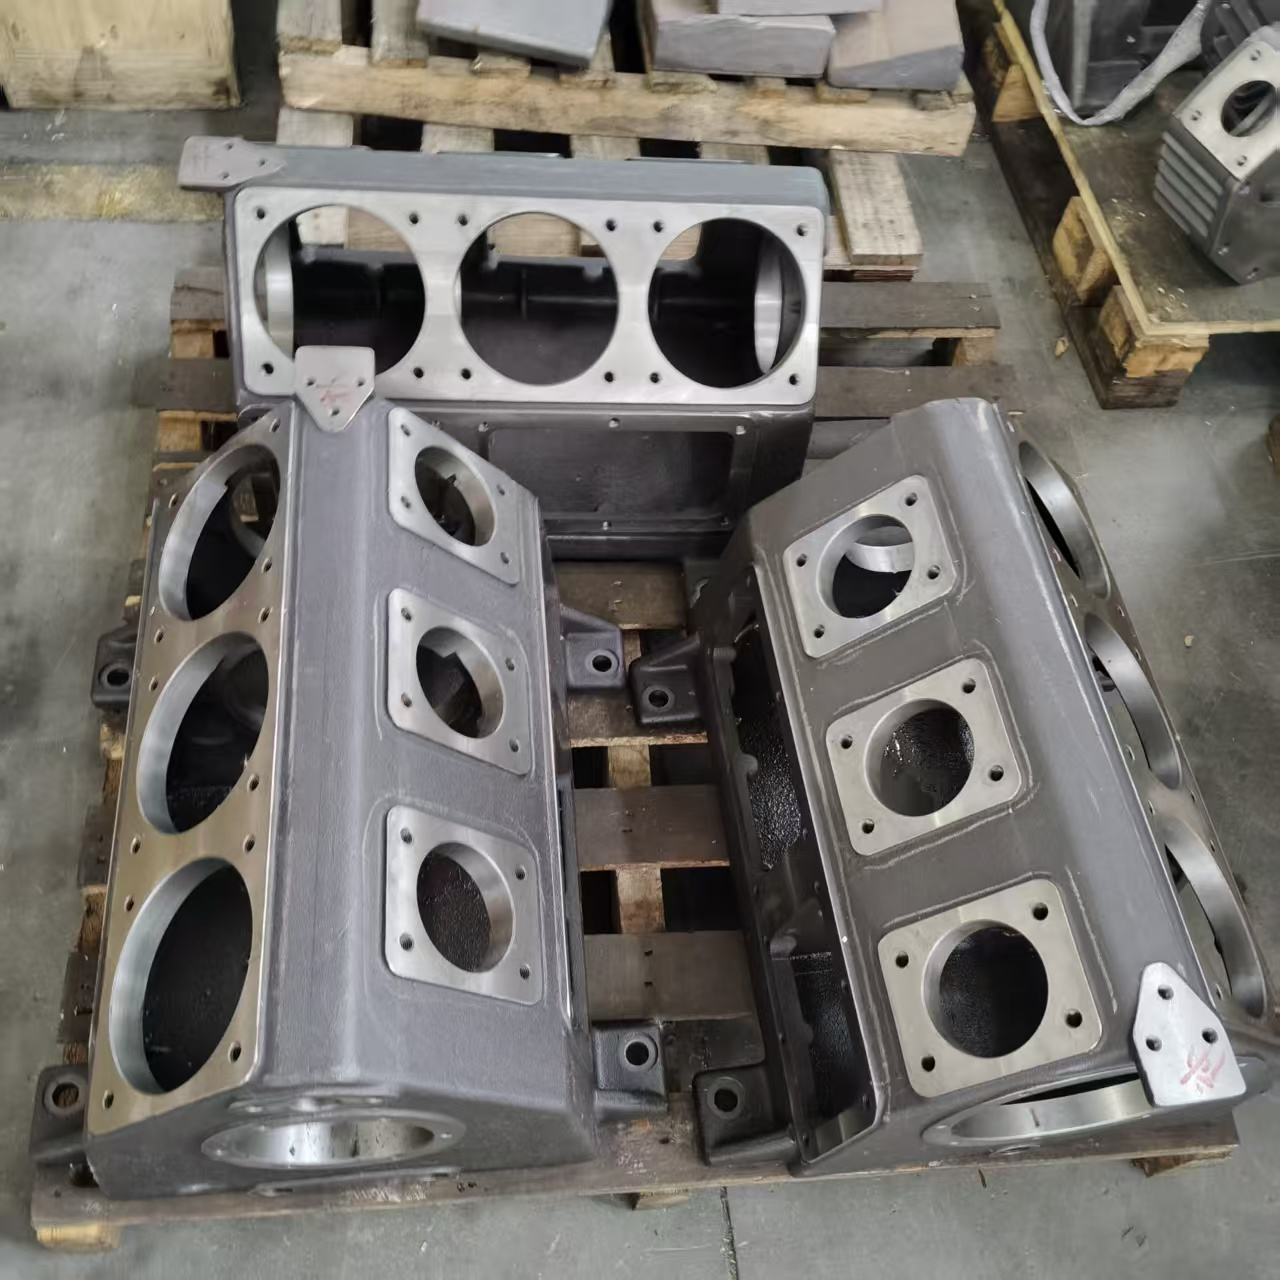
Machined Sand Casting Cylinder Block
Cylinder Block Casting Specifications
Standard parameters are listed below; every item can be adjusted to customer requirements.
| Item | Specification |
|---|---|
| Product | Cylinder Block / Engine Block casting, produced to customer drawings |
| Materials | Gray iron: ASTM A48 Cl.20–Cl.40, GG20–GG35; Ductile iron: ASTM A536 60-40-18, 70-50-05, GGG40–GGG60; other grades per customer requirements |
| Casting Process | Resin sand casting, green sand casting |
| Casting Weight | 0.1 kg – 3,000 kg (iron castings) |
| Dimensional Tolerance | CT8–CT12 (per ISO 8062) |
| Surface Roughness | Ra 6.3–25 μm as cast |
| Machining | CNC milling, boring, drilling and tapping to drawing tolerances |
| Surface Treatment | Shot blasting, anti-rust oil, painting |
| Quality Control | Spectrometer chemistry, test bars for mechanical properties, hardness testing, CMM dimension report |
| Standards | ASTM, SAE, AISI, ACI, DIN, EN, ISO, GB |
| Applications | Engine blocks, compressor housings, gearboxes and heavy machinery parts |
Sand Casting Cylinder Block – Production Process Flow
Every casting follows a standardized workflow with inspection gates between key processes:
| No. | Process Step | Key Control Points |
|---|---|---|
| 1 | Pattern & Core Box Making | Pattern built from the part drawing; shrinkage allowance confirmed by engineers |
| 2 | Sand Molding & Core Setting | Resin sand or green sand molds; cores form the water jackets and oil galleries |
| 3 | Melting & Pouring | Chemistry of every heat checked with a spectrometer before pouring |
| 4 | Cooling & Shakeout | Controlled cooling; casting separated from the sand mold |
| 5 | Fettling & Grinding | Risers and running system removed; parting lines ground smooth |
| 6 | Heat Treatment | Stress-relief annealing when required by the drawing |
| 7 | Blasting & Inspection | Shot blasting; dimension, hardness and internal quality inspection |
| 8 | CNC Machining & Final QC | Critical faces and bores machined; CMM report before packing |
Leesh Holdings Sand Casting Craftsmanship
Sand casting is the backbone of Leesh Holdings’ cast iron cylinder block casting production — it is the most widely used casting method in the world. Based on your part drawing, our engineers first build the pattern and core boxes; sand molds and cores then form the hollow water jackets, oil galleries and mounting bosses of the block. After the molten iron solidifies in the mold, the casting is shaken out, the risers and running system are removed, and the part is cleaned and inspected as a finished rough casting cylinder block, ready for machining or delivery.
Leesh Holdings owns 2 automatic production lines for cast iron and cast steel. For a ductile iron cylinder block casting, the chemistry of every heat is checked with a spectrometer and test bars are poured to verify tensile strength and elongation against the selected ASTM or EN grade, so the mechanical properties of your blocks are repeatable batch after batch.
- ✓ 2 automatic molding lines — flexible for both prototype and bulk production
- ✓ Green sand and resin sand processes for small to large batch runs
- ✓ Materials supplied to ASTM, SAE, AISI, ACI, DIN, EN, ISO and GB standards
- ✓ Casting weight from 0.1 kg to 3,000 kg with CT8–CT12 tolerance
- ✓ In-house CNC machining, so blocks arrive ready for your assembly line
The complete production workflow is illustrated in the process chart below:
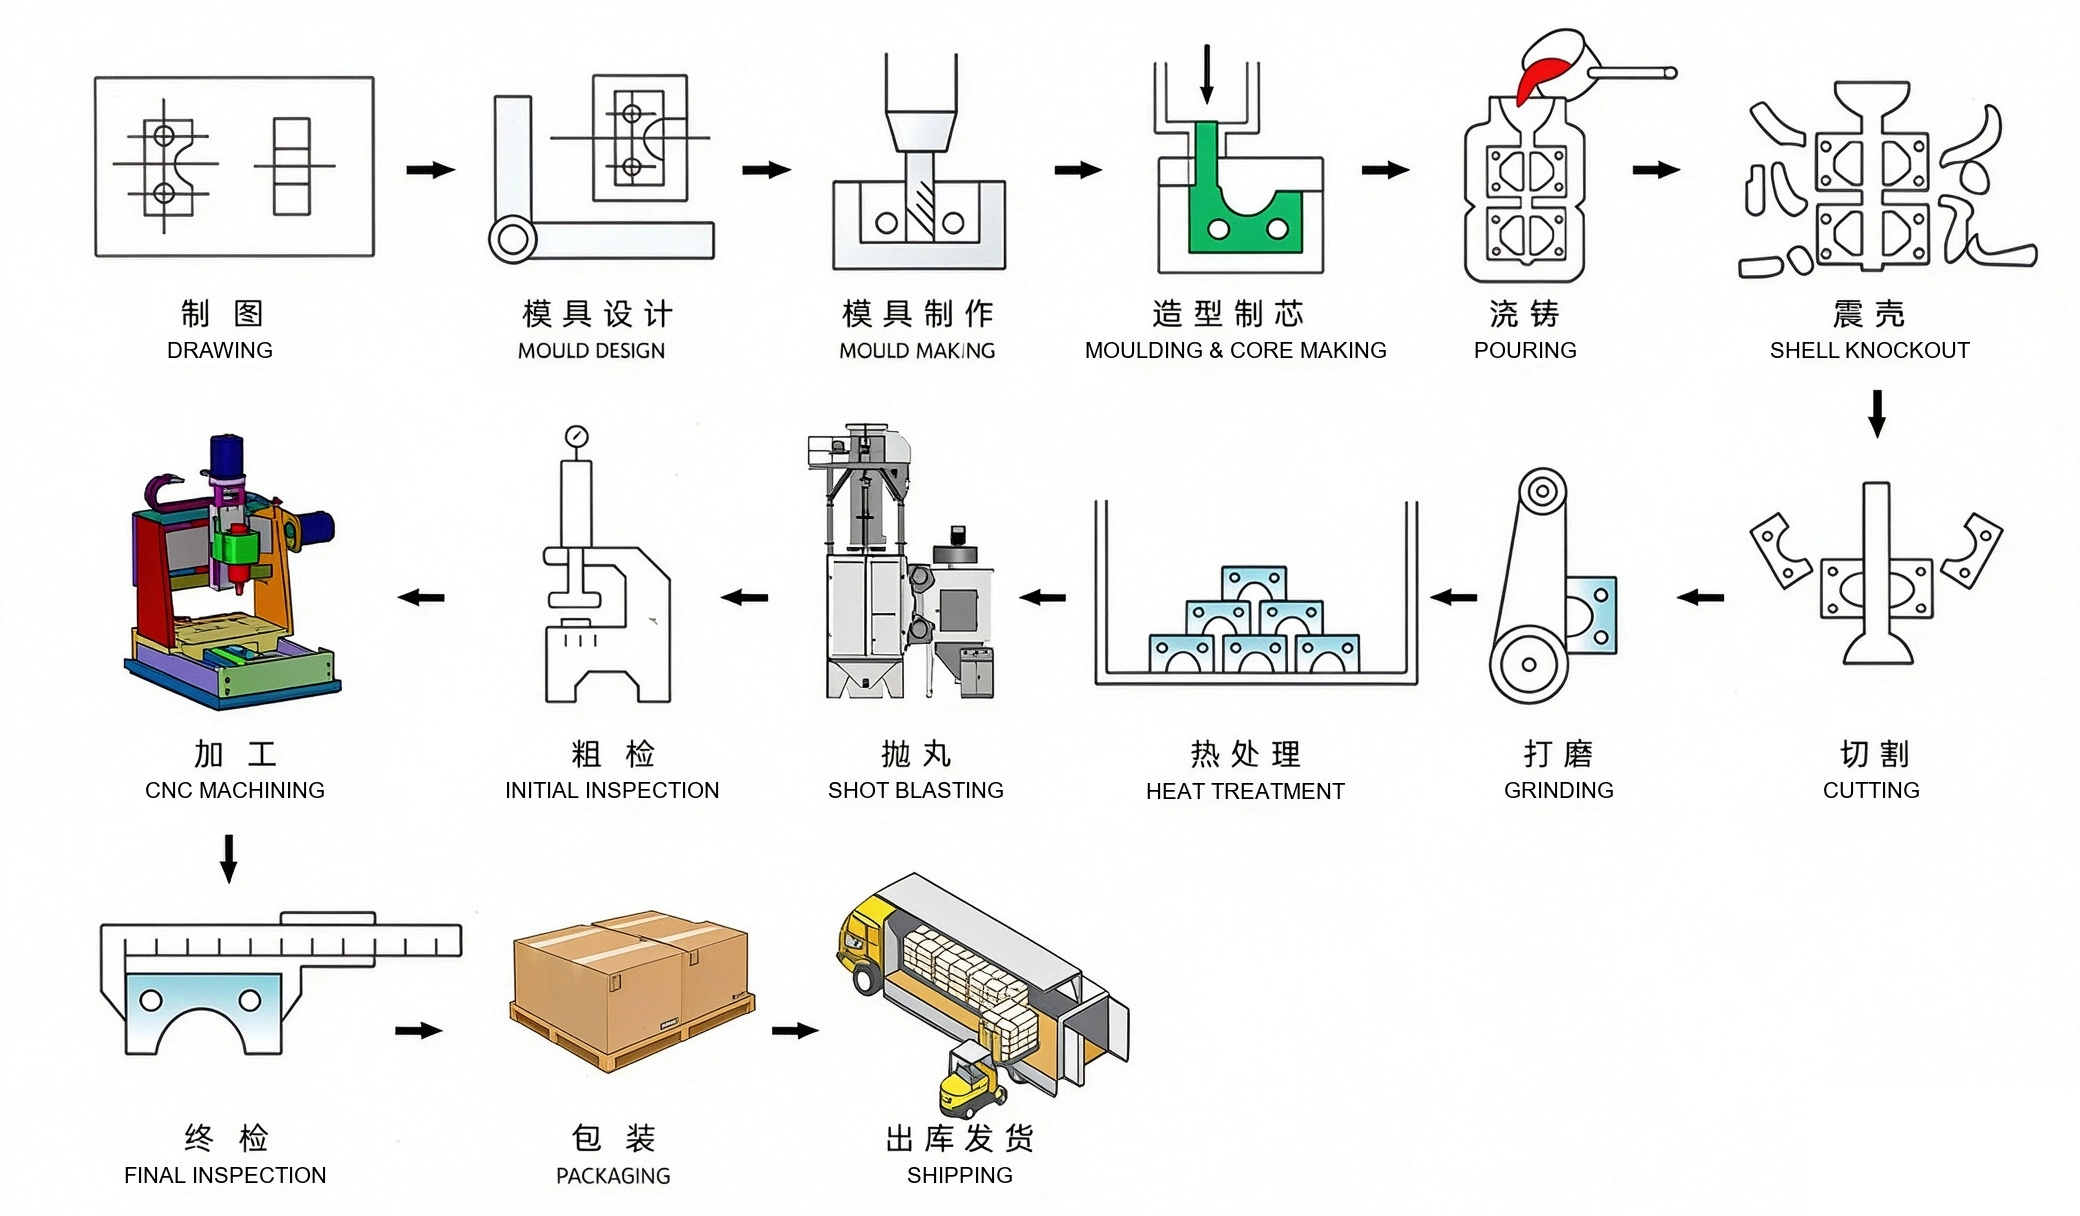
Sand casting process at Leesh Holdings — from part drawing to shipping
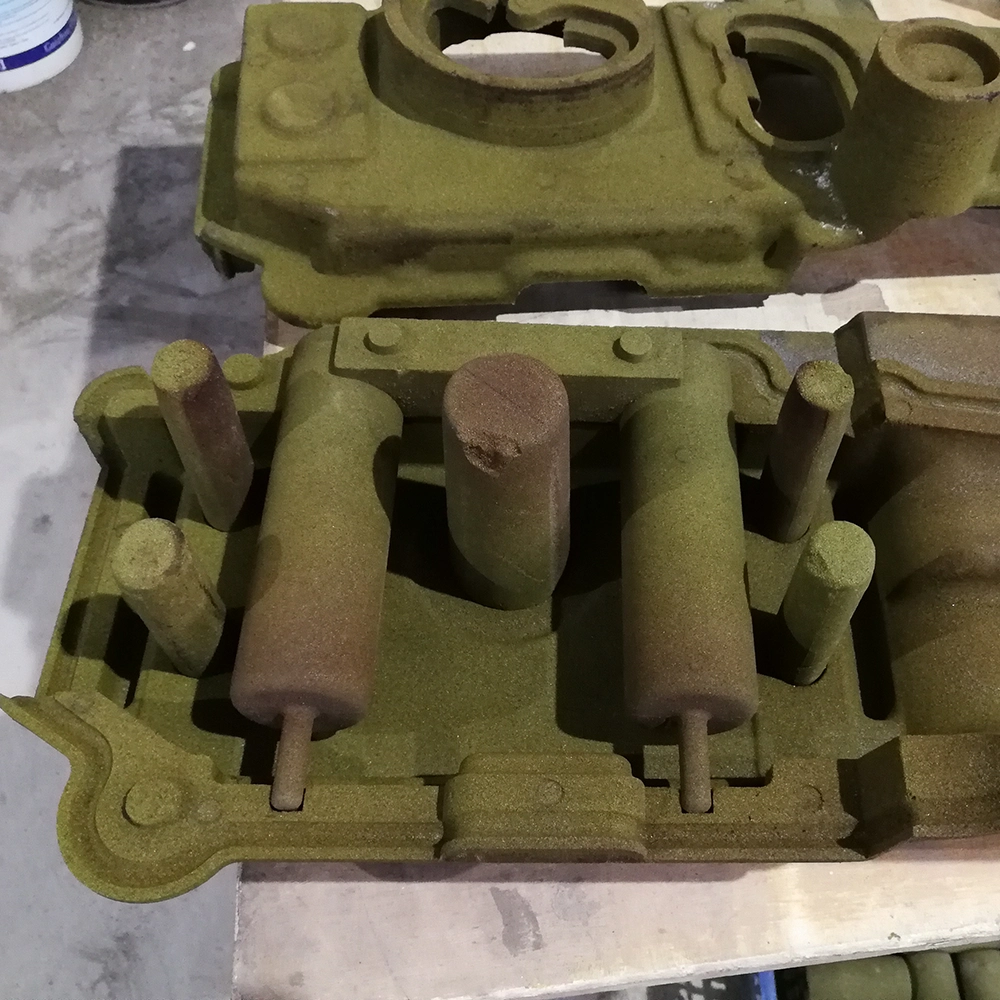
Pattern & Core Box Making

Resin Sand Molding

Melting & Pouring
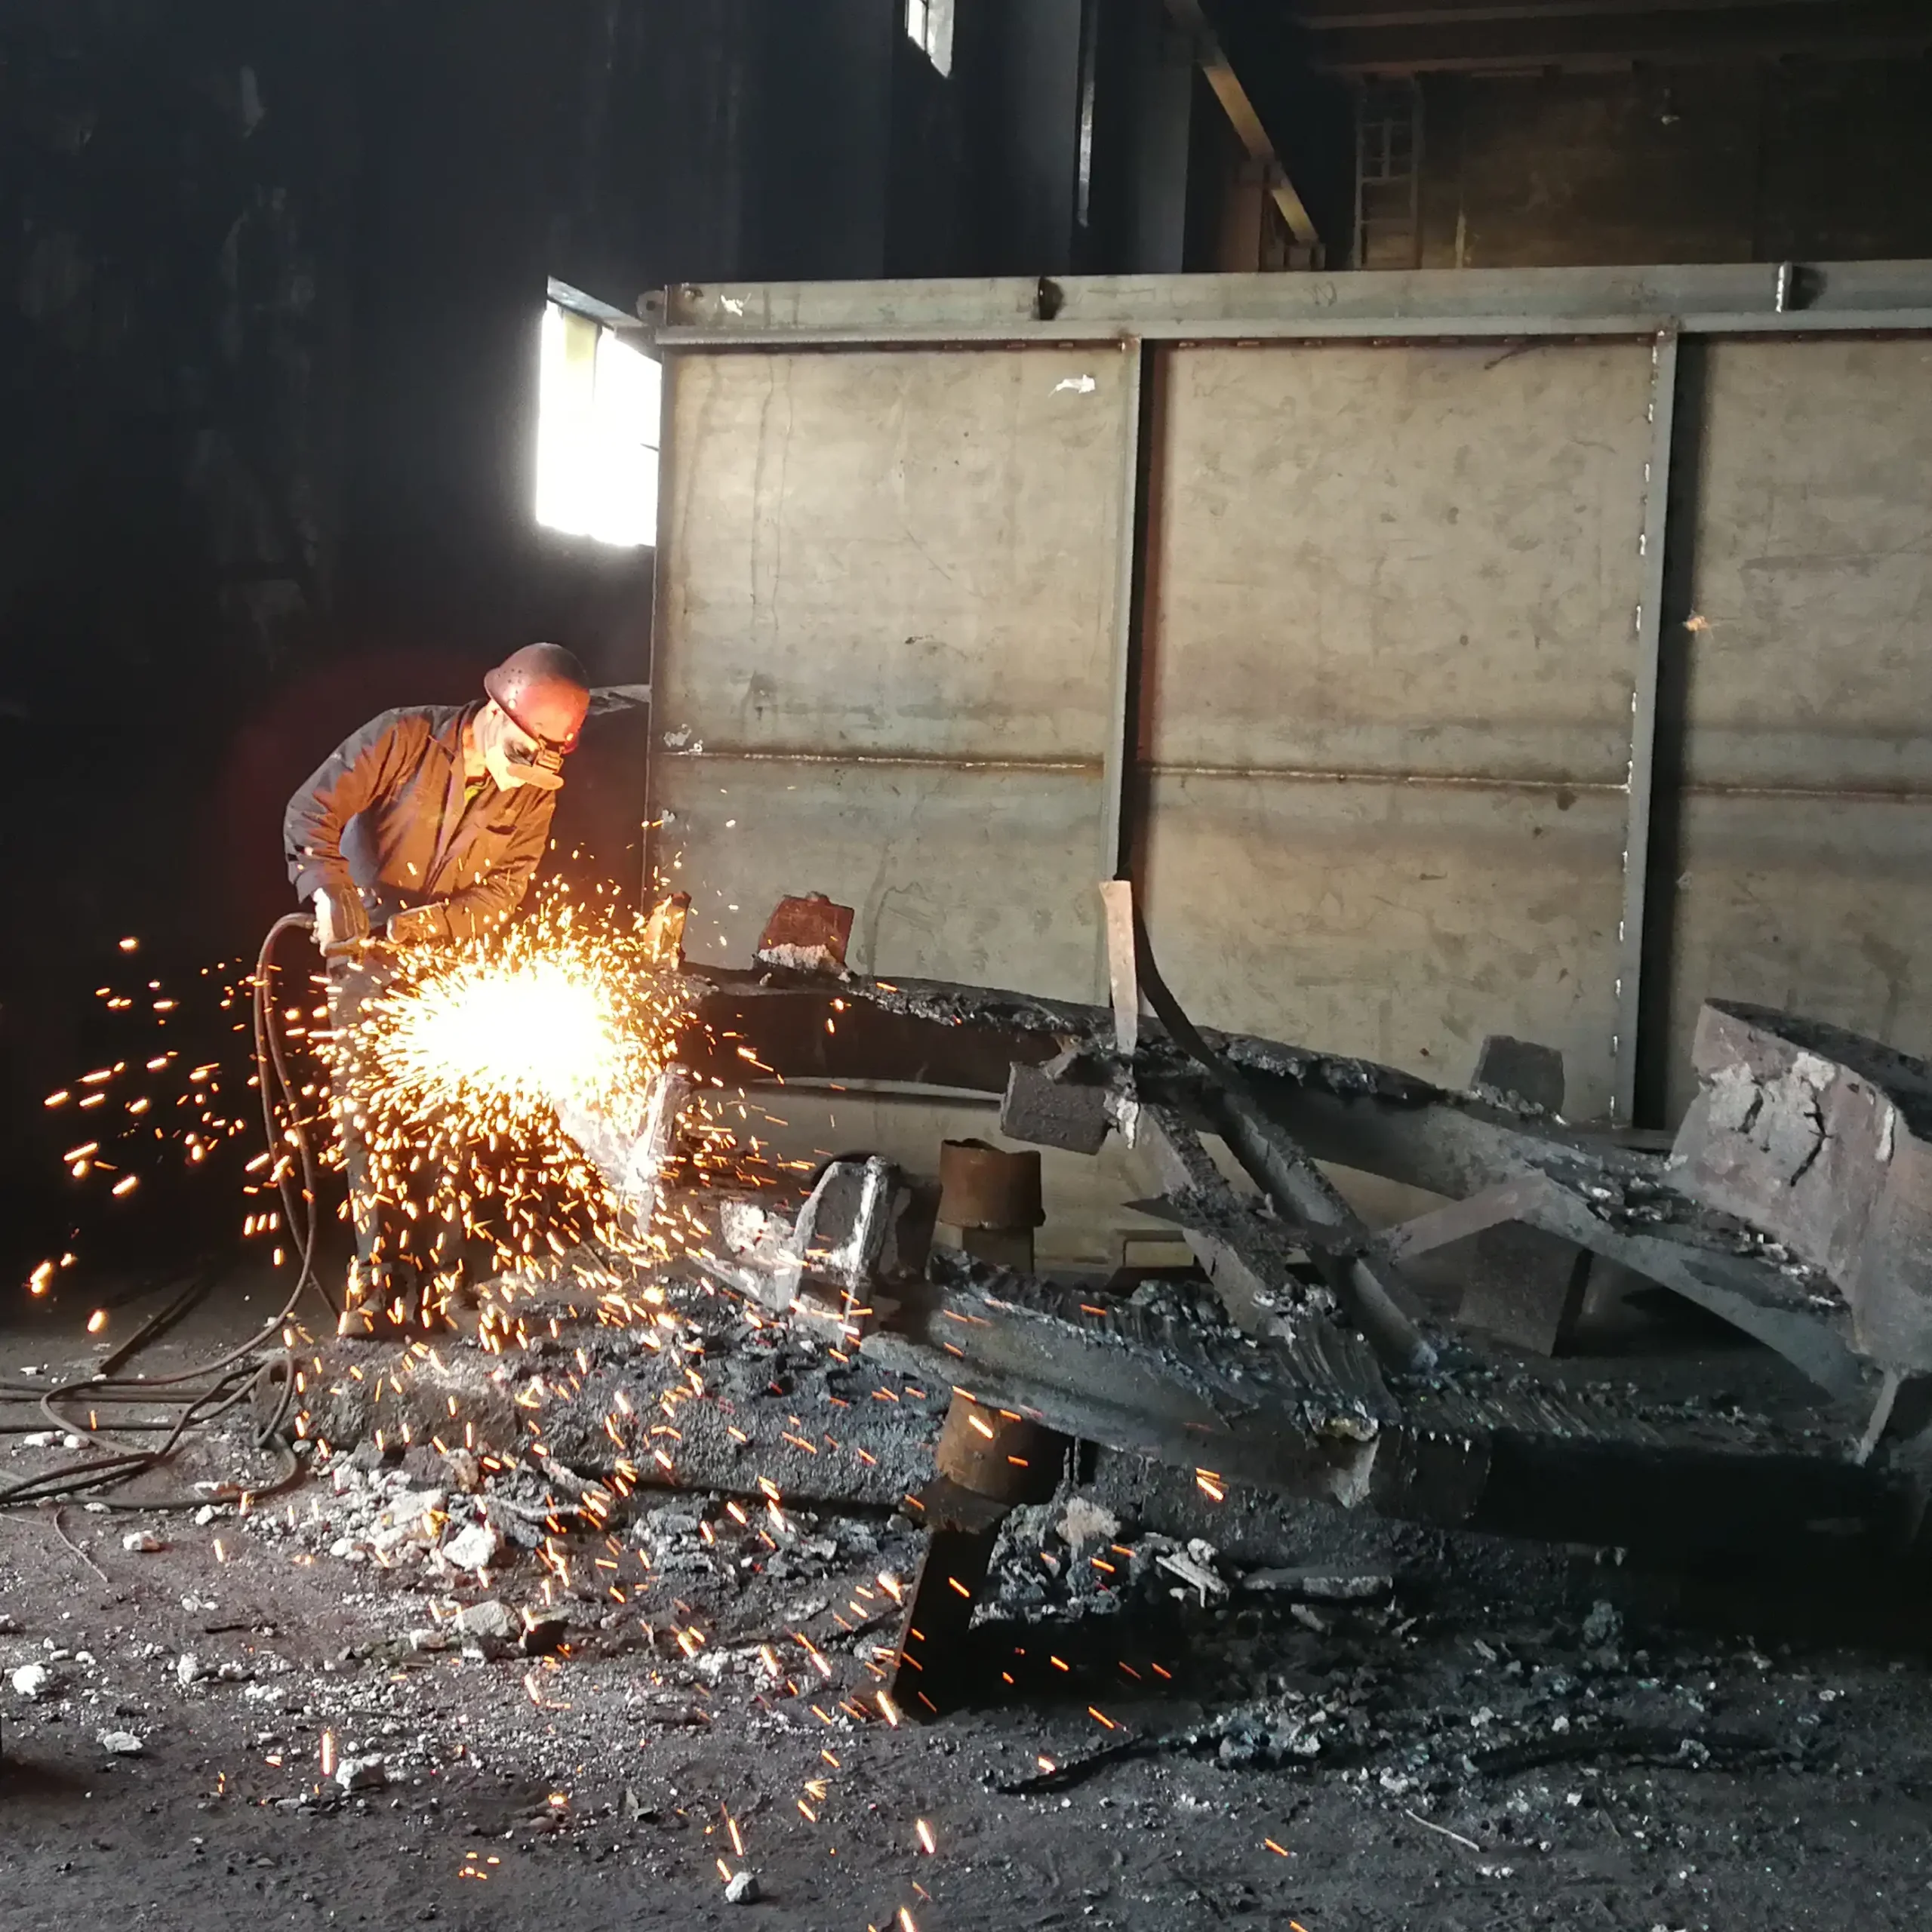
Shakeout & Fettling

CNC Machining
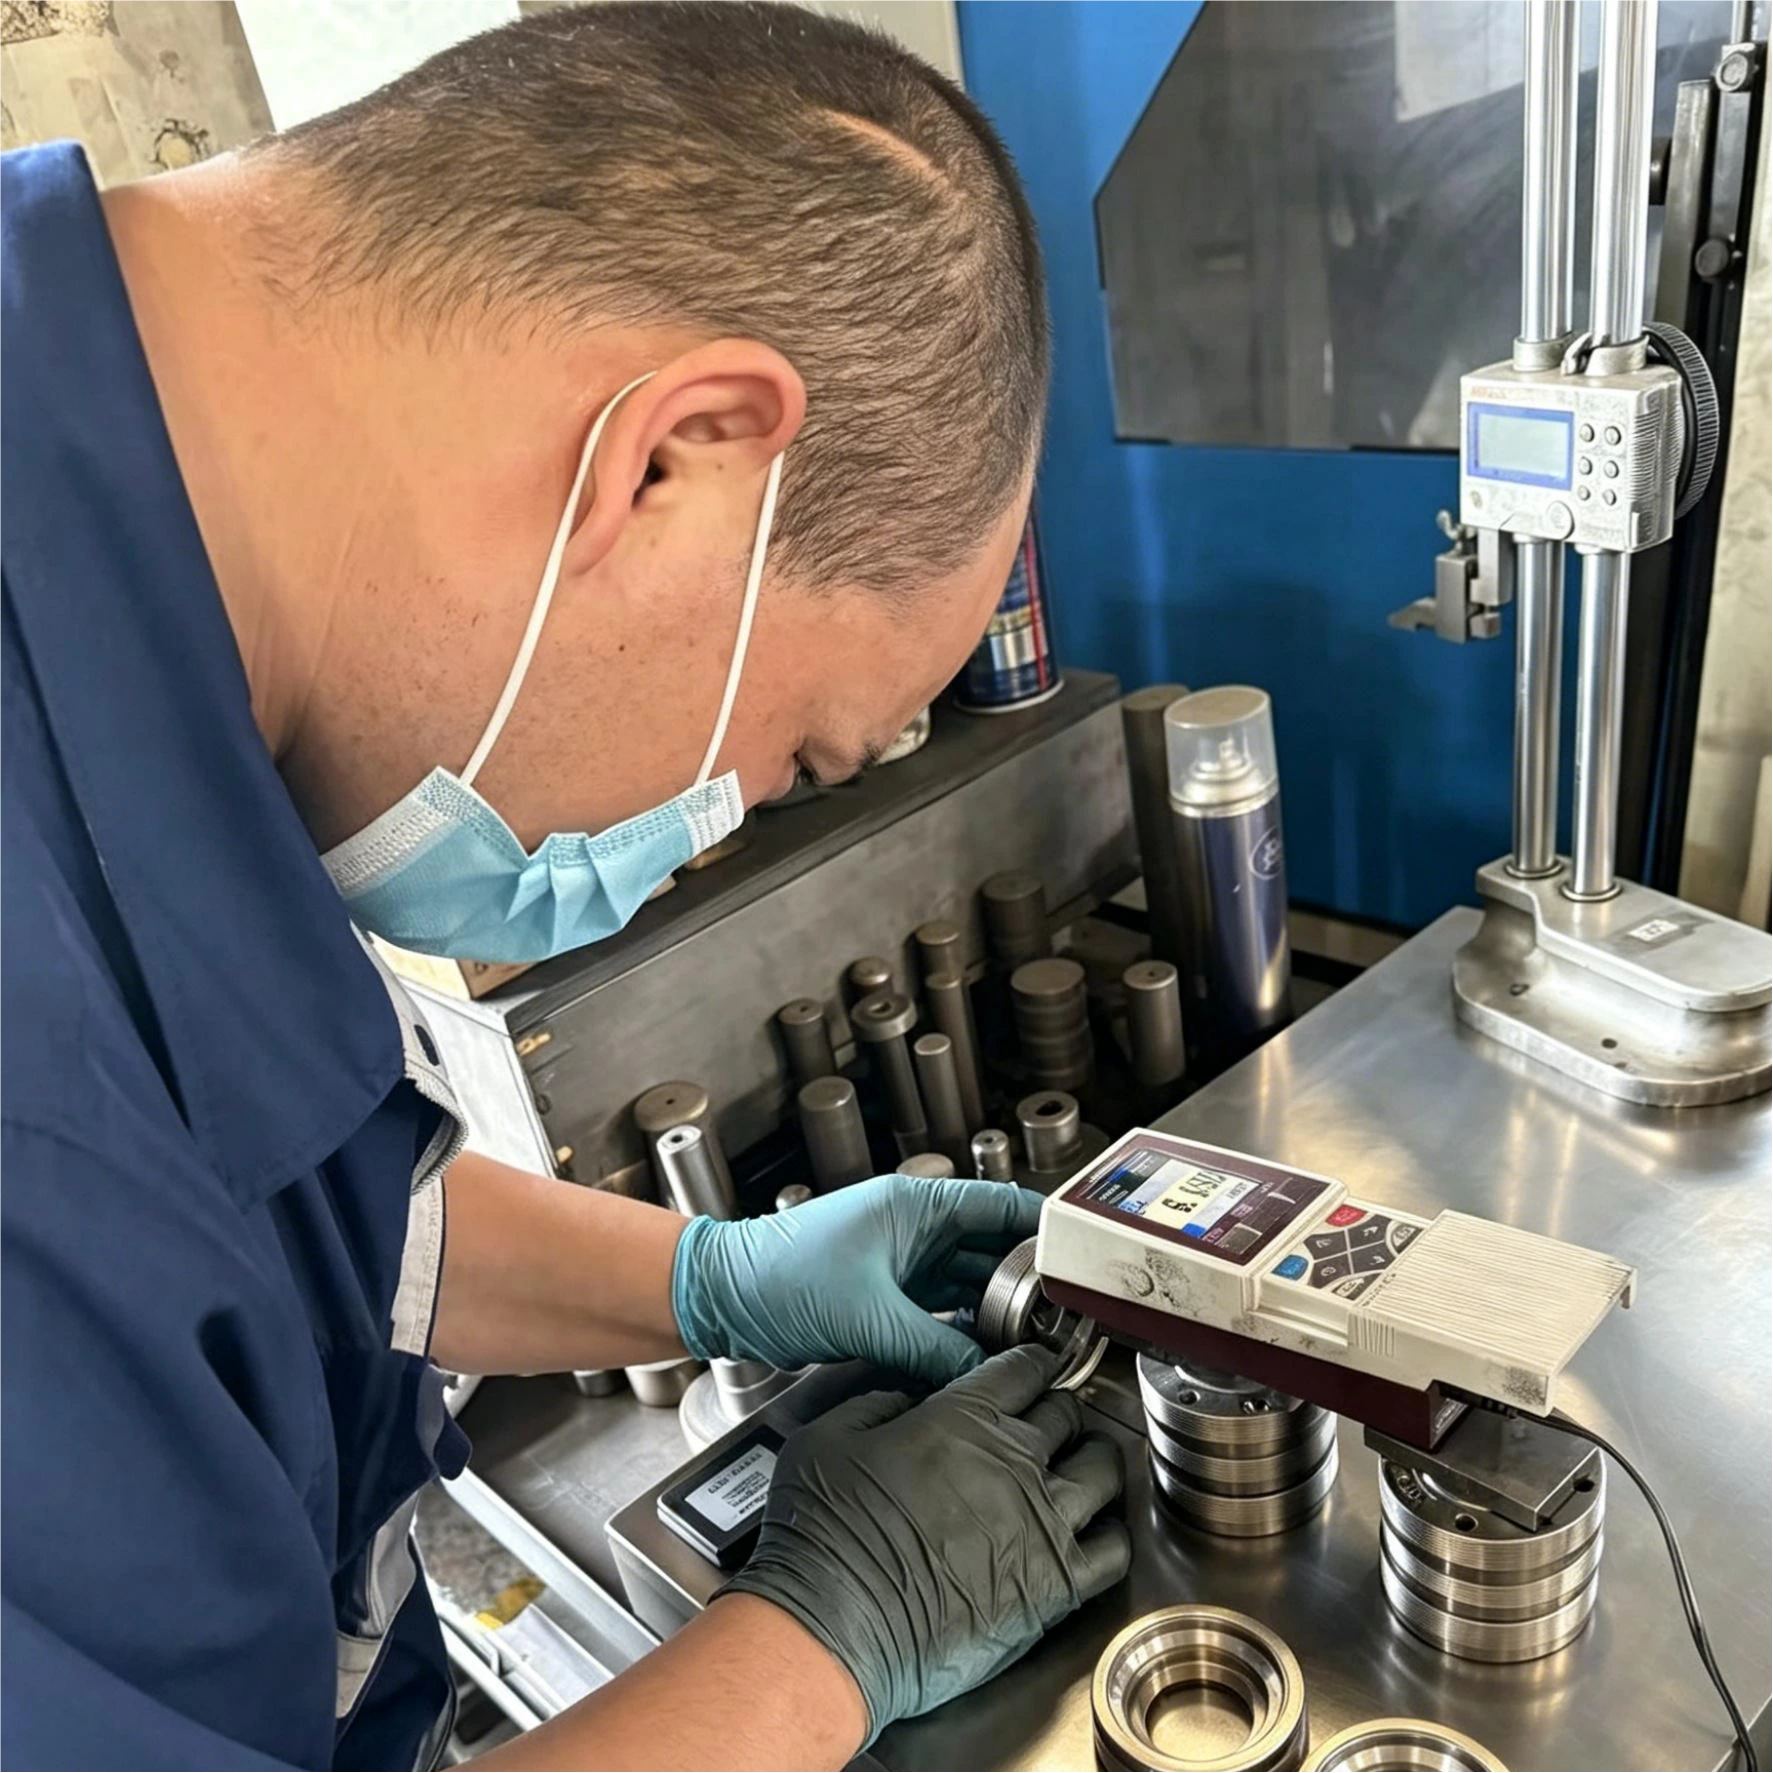
Quality Inspection
Applications of Cast Iron Cylinder Blocks
Our cylinder block casting service supports OEMs and end users across the following fields:
| Application Field | Typical Products | Key Requirements |
|---|---|---|
| Automotive & Commercial Vehicles | Engine blocks, flywheel housings | Pressure tightness, dimensional accuracy |
| Mining Machinery Cylinder Block | Crusher and hoist housings, hydraulic cylinder blocks | Heavy-section strength, wear resistance |
| Construction Machinery | Engine and valve blocks for loaders and excavators | Impact resistance, stable batch quality |
| Agricultural Machinery | Tractor engine blocks, gearbox housings | Cost efficiency, volume consistency |
| Compressors & Pumps | Compressor frames, bearing housings | Casting density, machined surface finish |
| Marine & Power Generation | Genset engine blocks, marine engine blocks | Coating quality, documentation support |
Why Choose Leesh Holdings for Cylinder Block Casting?
- ✓ One-stop production: sand casting foundry and CNC machining workshop under the same group
- ✓ Material flexibility: gray iron and ductile iron grades matched to your working conditions
- ✓ Engineering support: DFM feedback on your drawings before tooling is made
- ✓ Strict quality control: spectrometer, test bars, hardness and CMM reports for every batch
- ✓ Export experience: seaworthy packing and delivery for global customers
Cylinder Block Casting FAQs
What do you need to quote my part?
Please send a 2D drawing (PDF) and a 3D model (STEP/IGES) if available, together with the material grade, target weight, annual quantity and machining requirements. Our engineers will reply with price and lead time, and an NDA can be signed before the technical review.
Which materials and standards do you support?
Gray iron ASTM A48 Cl.20–Cl.40 and GG20–GG35, ductile iron ASTM A536 60-40-18 to GGG60, plus other grades per customer requirements. Materials follow ASTM, DIN, EN, ISO and GB standards.
Can you machine the block after casting?
Yes. CNC milling, boring, drilling and tapping are done in our own machining workshop, so cylinder bores and mounting faces arrive machined to your drawing.
How do you control quality?
Every heat is checked with a spectrometer, test bars verify the mechanical properties, and hardness, CMM dimension and internal quality inspections are carried out before packing. Reports are supplied with each batch.
What is your MOQ and delivery time?
MOQ is flexible and samples or pilot batches are welcome. Tooling usually takes a few weeks, and the production lead time depends on quantity and machining scope.
Get a Quote for Your Cylinder Block Casting Project
Send your drawings to sales@leesh.cn — our engineering team will review the part and reply with casting price, lead time and DFM suggestions.
