Leesh Holdings · Stainless Steel Lost-Wax Foundry Group
1.4301 Investment Casting Manufacturer & Supplier
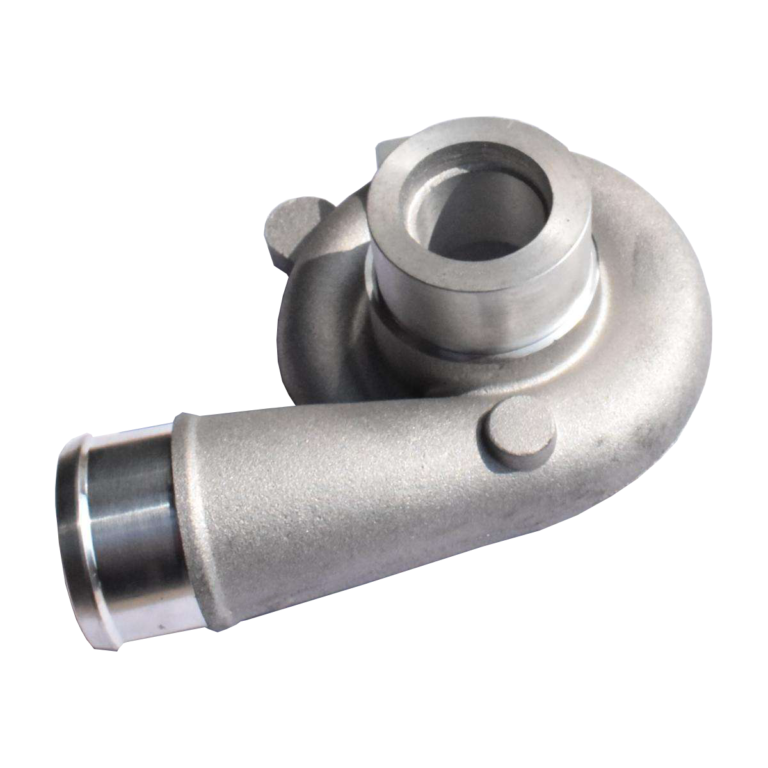
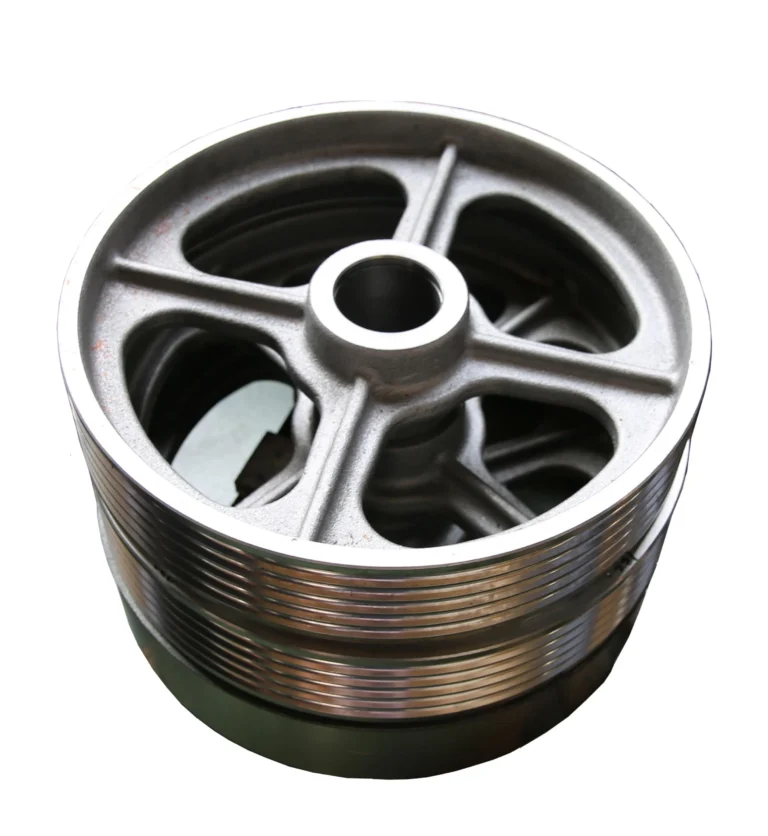
Leesh Holdings produces precision 1.4301 Investment Casting components for pump, valve, food-processing and marine OEMs — from in-house wax tooling to fully machined parts ready for your assembly line.
- Cast equivalent CF8 / SCS13
- In-house wax & shell tooling
- CNC machining & CMM inspection
- Export documentation included
Why Leesh Holdings
A dedicated 1.4301 Investment Casting line, built for OEM buyers
Leesh Holdings runs the complete production chain for 1.4301 Investment Casting under one roof — wax tooling, ceramic shell building, induction melting, finishing and CNC machining. Vertical control is how we hold tolerances, keep surfaces clean and answer RFQs faster than a trading company can.
Grade 1.4301 (EN 10088 X5CrNi18-10, broadly equivalent to AISI 304) is the most widely specified austenitic stainless steel for cast components, so we keep dedicated melt formulations, tooling libraries and inspection routines for it. Whether you need hundreds of pump impellers a month or a 50-piece prototype run of custom housings, the same production discipline applies.
Typical production values for guidance — send your drawing for a project-specific tolerance review.
Material Specifications
What is 1.4301 Investment Casting?
1.4301 Investment Casting pairs a proven material with a near-net-shape process. Grade 1.4301 — X5CrNi18-10 under EN 10088, the European counterpart of AISI 304 — is an 18/10 chromium-nickel austenitic stainless steel chosen for corrosion resistance, weldability and easy-to-clean surfaces. Poured into ceramic shells formed around disposable wax patterns, 1.4301 Investment Casting delivers complex stainless geometries that machining alone could not make economically.
Typical chemistry
| Element | Content (wt. %) |
|---|---|
| Carbon (C) | ≤ 0.07 |
| Silicon (Si) | ≤ 1.00 |
| Manganese (Mn) | ≤ 2.00 |
| Phosphorus (P) | ≤ 0.045 |
| Sulfur (S) | ≤ 0.030 |
| Chromium (Cr) | 17.5 – 19.5 |
| Nickel (Ni) | 8.0 – 10.5 |
| Nitrogen (N) | ≤ 0.11 |
Wrought 1.4301 limits per EN 10088; cast CF8 chemistry (ASTM A743) governs actual pours.
Typical mechanical properties — CF8-condition castings
| Property | Typical value |
|---|---|
| Tensile strength | ≥ 485 MPa |
| 0.2 % proof strength | ≥ 205 MPa |
| Elongation | ≥ 30 % |
| Hardness | ≈ 140 – 190 HB |
| Density | 7.9 g/cm³ |
Values vary with section size and heat treatment; every shipment carries an EN 10204 3.1 material test report.
Where chlorides are aggressive, we will tell you honestly if 1.4301 is the wrong choice — upgrading to 1.4408 (CF8M, the 316-type equivalent) is usually a small premium for a large gain in pitting resistance. That kind of material guidance is part of every Leesh Holdings RFQ review.
How We Make It
The 1.4301 Investment Casting process at Leesh Holdings
Six controlled steps take a wax pattern to a finished casting — every heat traceable, every lot documented.
Tooling & wax injection
Aluminium moulds inject dimensional-stable wax patterns; multi-cavity tooling scales output to your volumes without re-qualification.
Pattern assembly & shell building
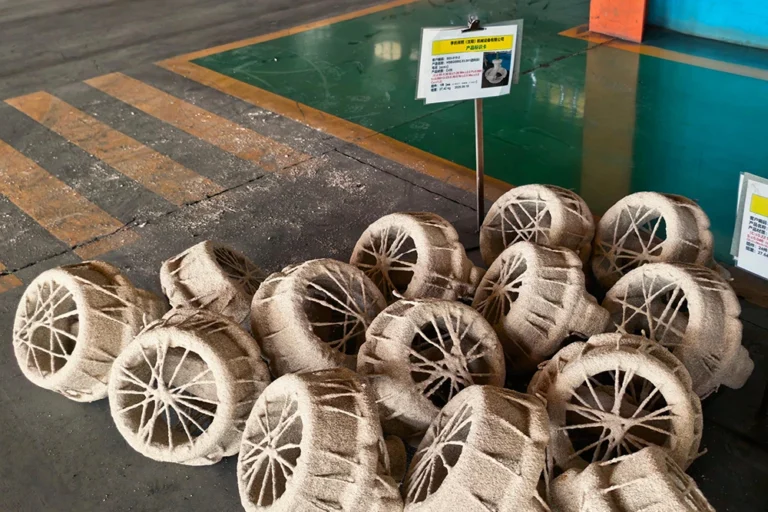
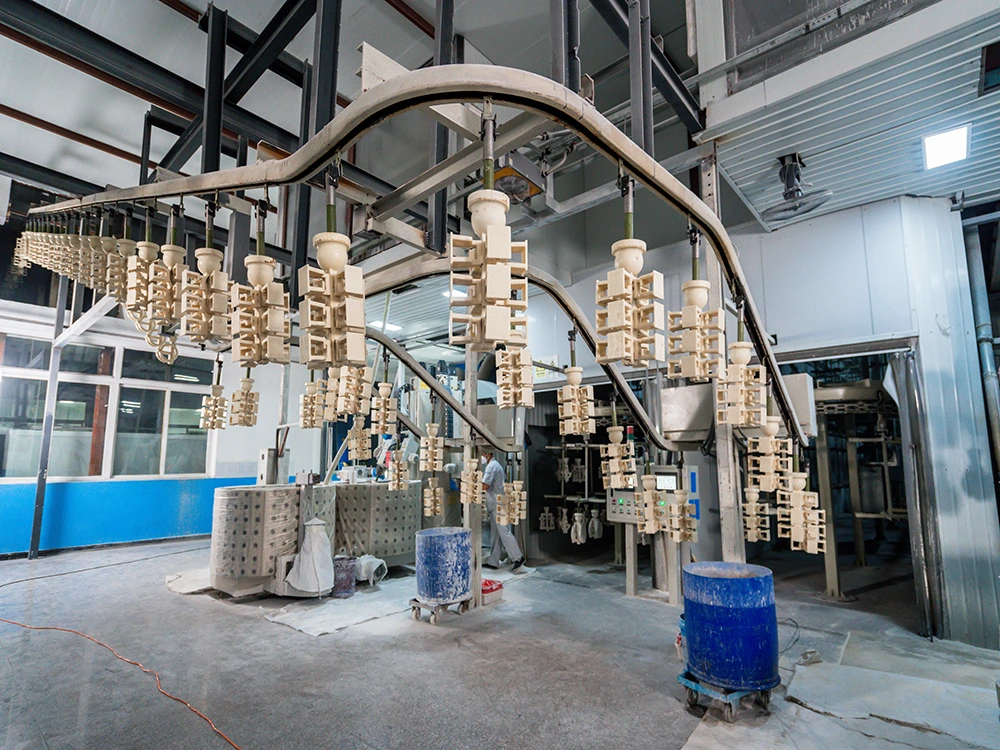
Patterns are gated onto trees and dipped repeatedly in colloidal-silica ceramic slurries to build a crack-resistant shell.
Dewax & firing
Autoclave dewaxing and high-temperature firing leave a rigid, gas-permeable ceramic mould ready for pouring.
Melting & pouring
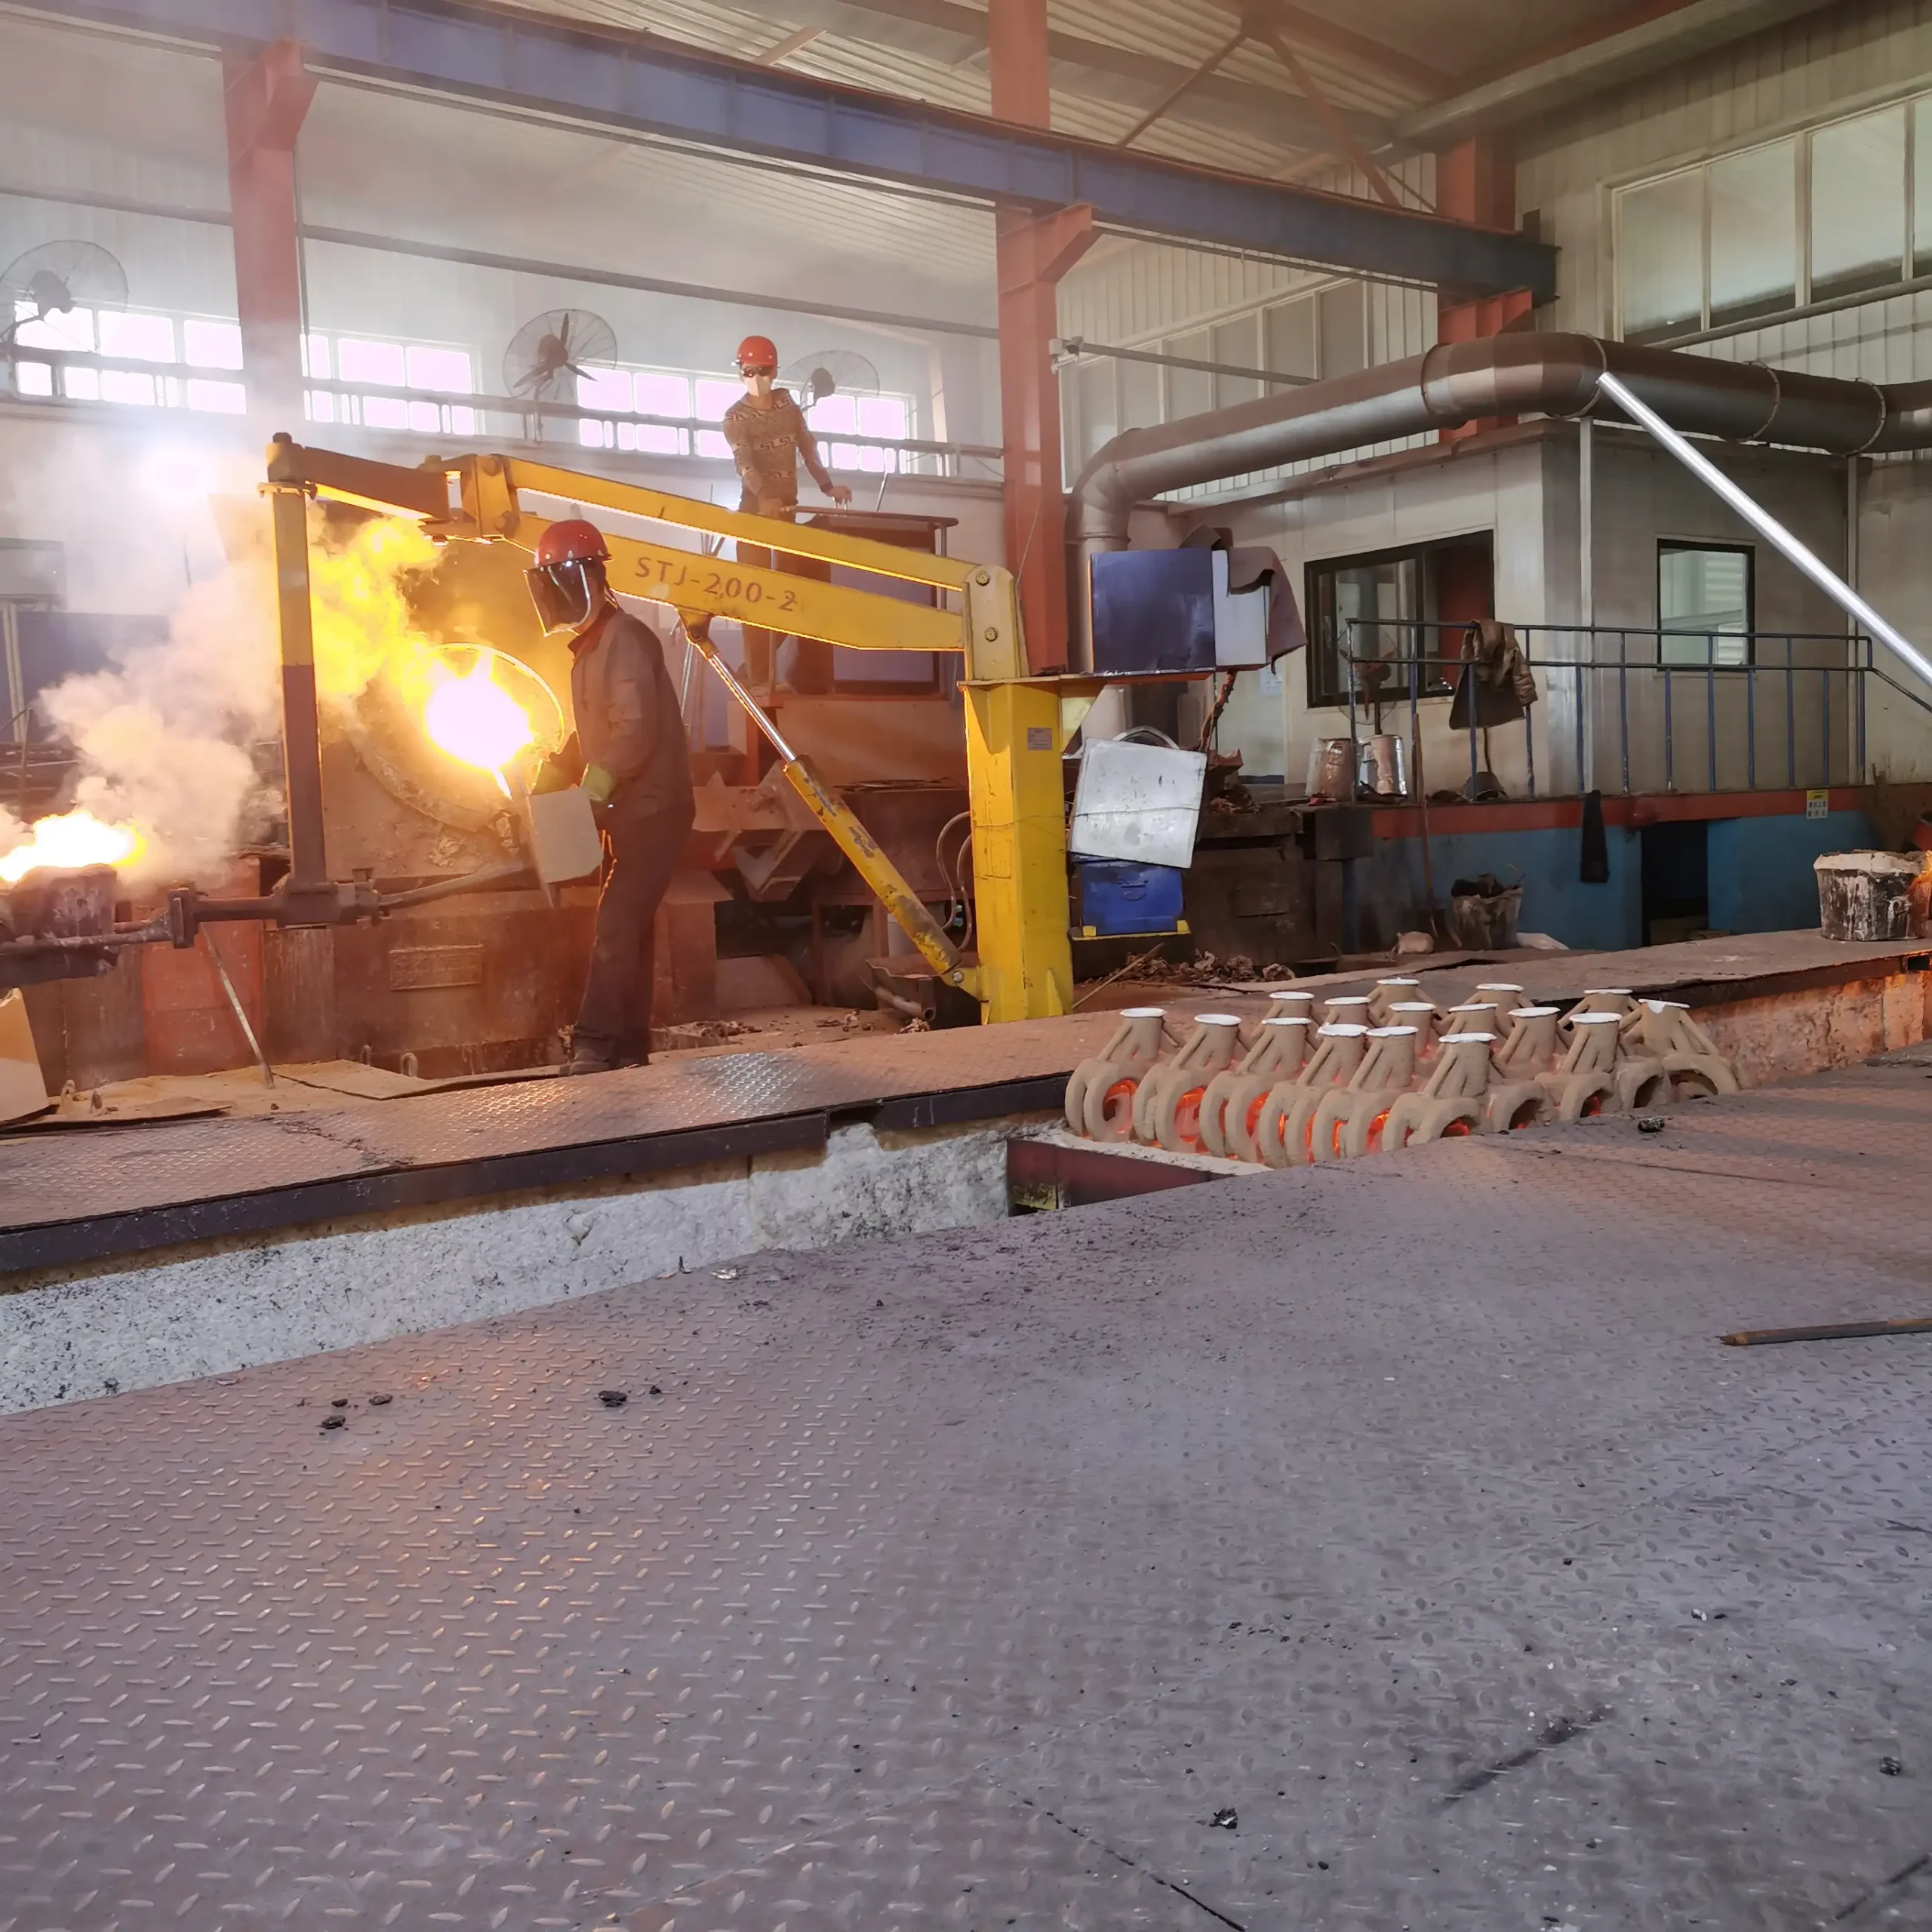
1.4301 / CF8 melt chemistry is verified by spectrometer before every pour at controlled superheat for clean fill.
Knockout & finishing
Shells are broken out; castings are cut off, ground, shot-blasted and heat-treated as the drawing requires.
Machining & final inspection
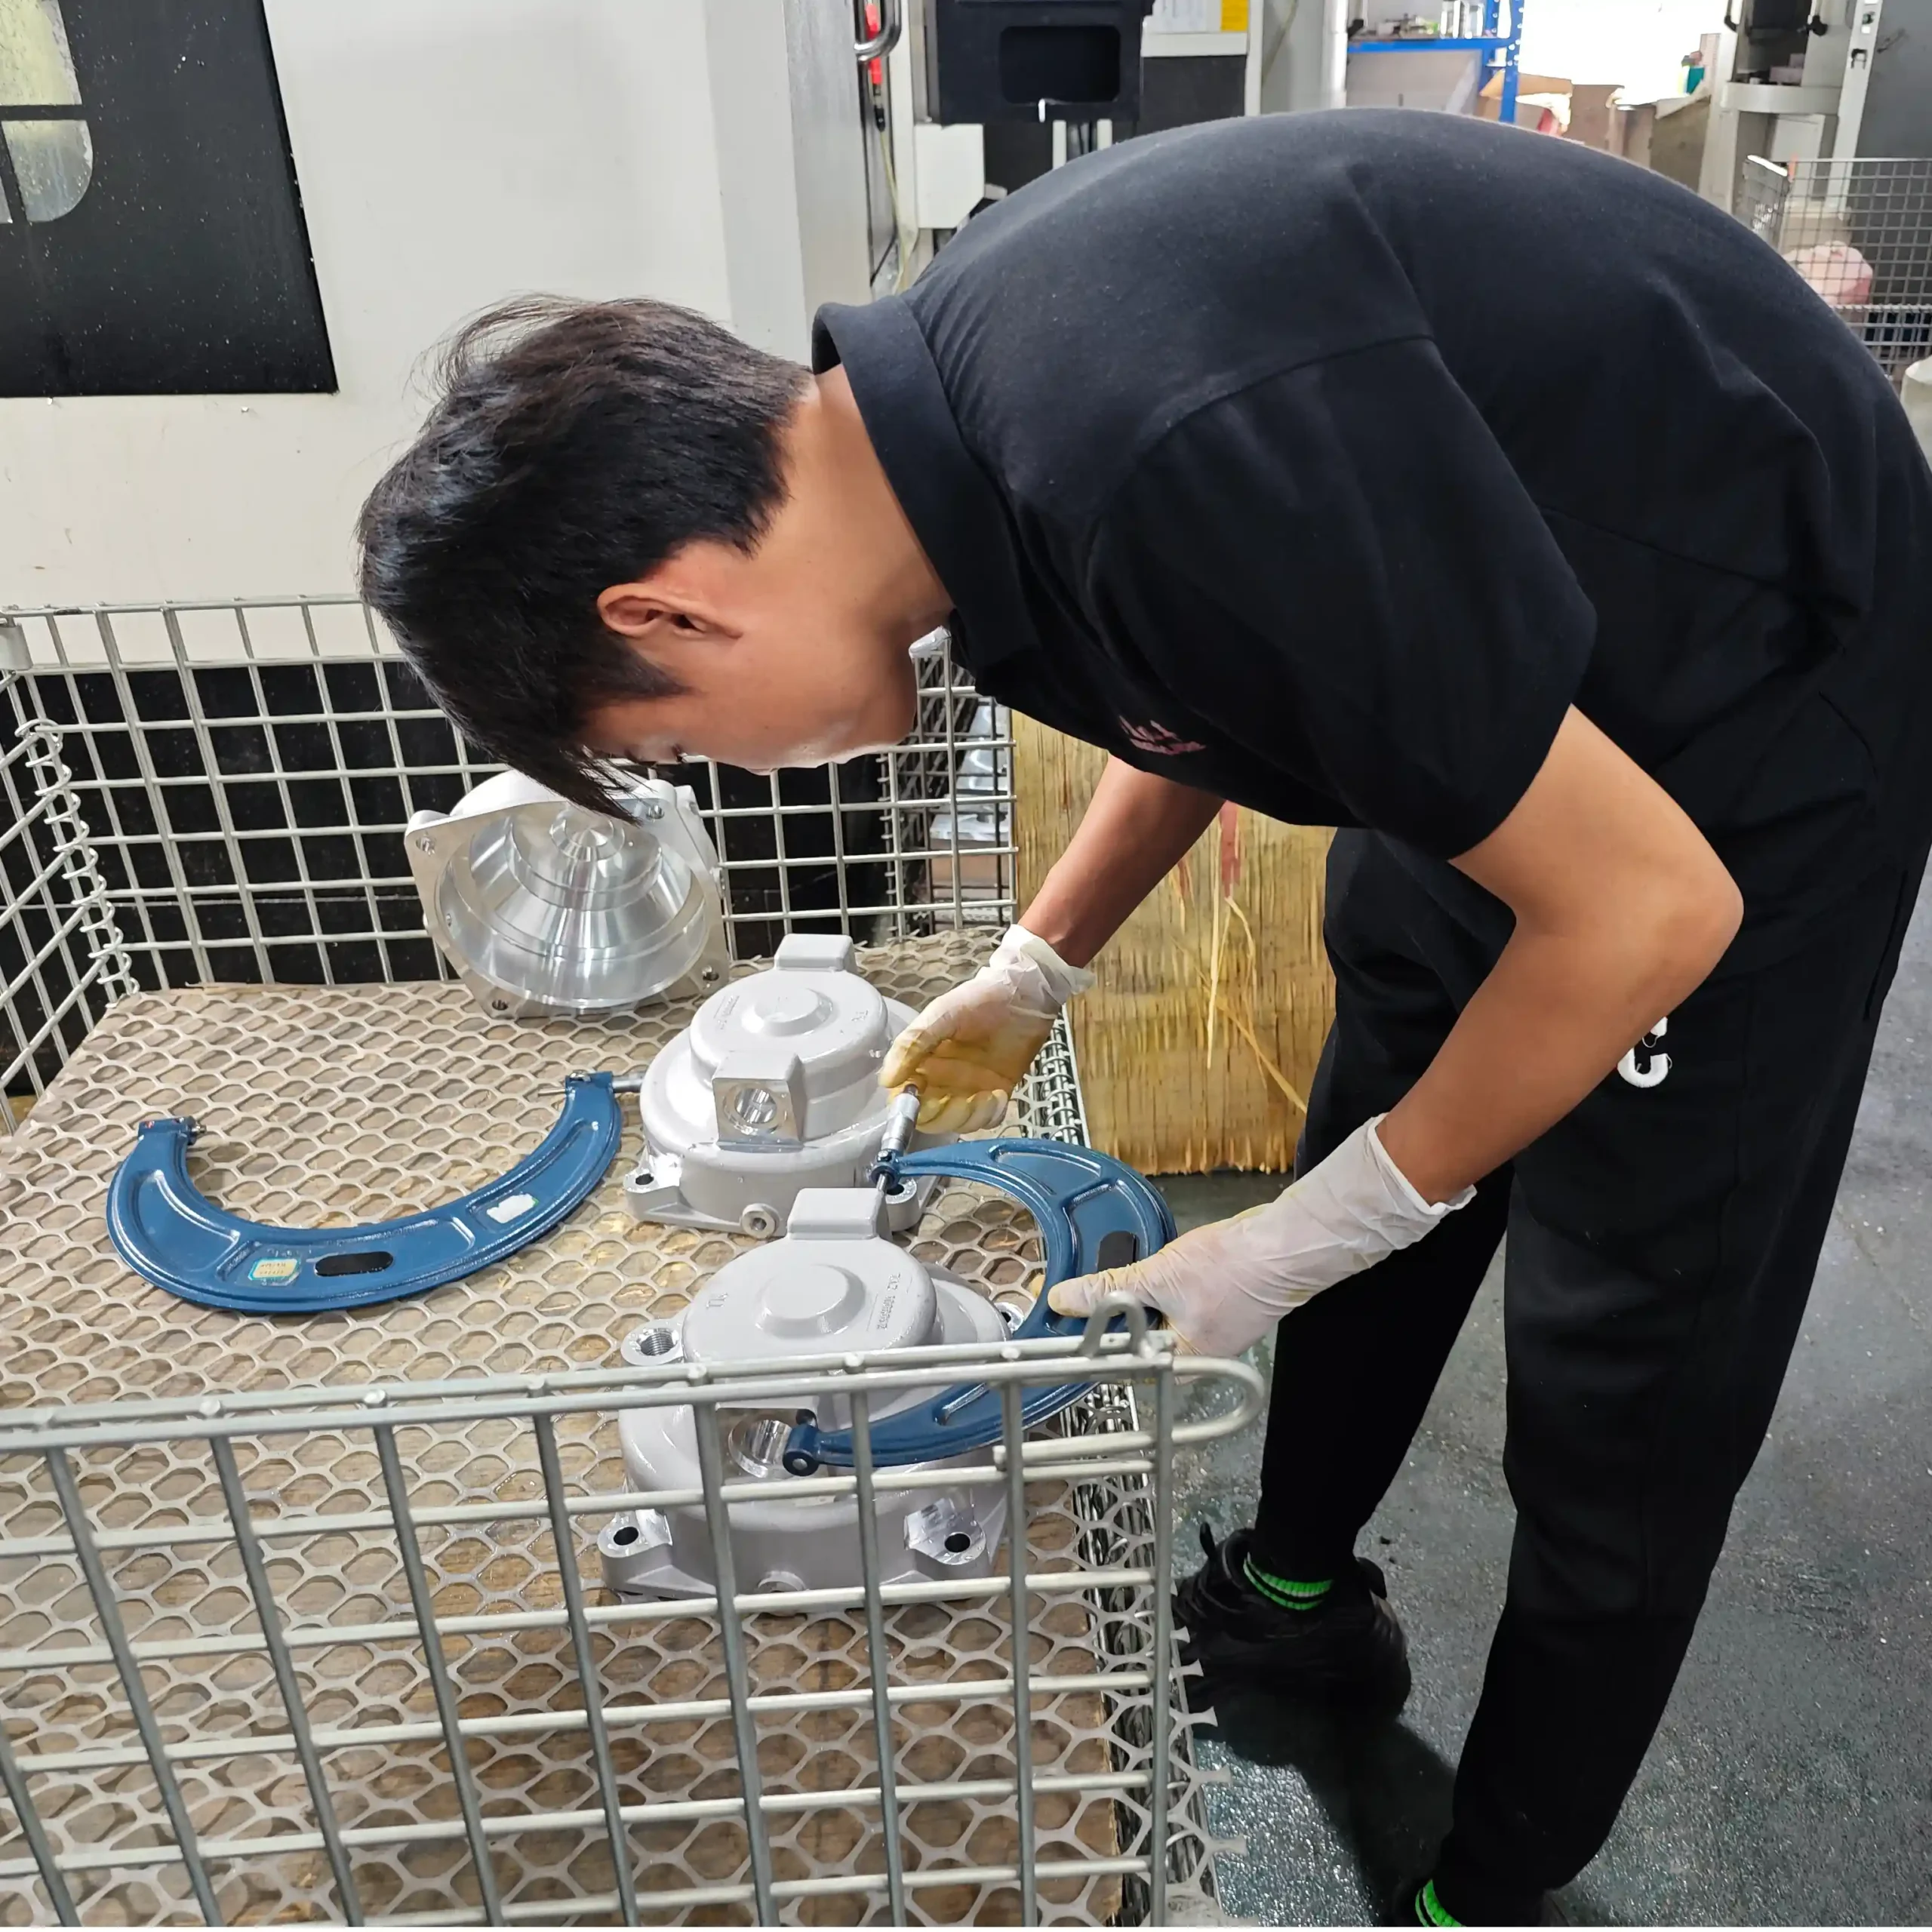
CNC machining, pickling & passivation, CMM dimensional checks and surface crack testing before export packing.
Documentation & traceability: heat-number traceability, EN 10204 3.1 material test reports, dimensional reports and PPAP-style files on request. Third-party inspection is welcome before shipment.
Foundry Inside
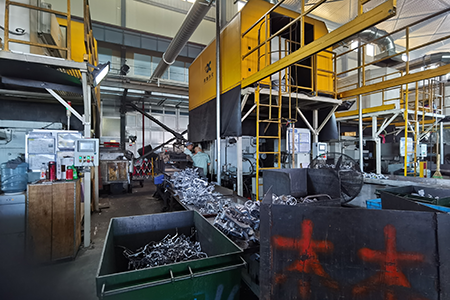
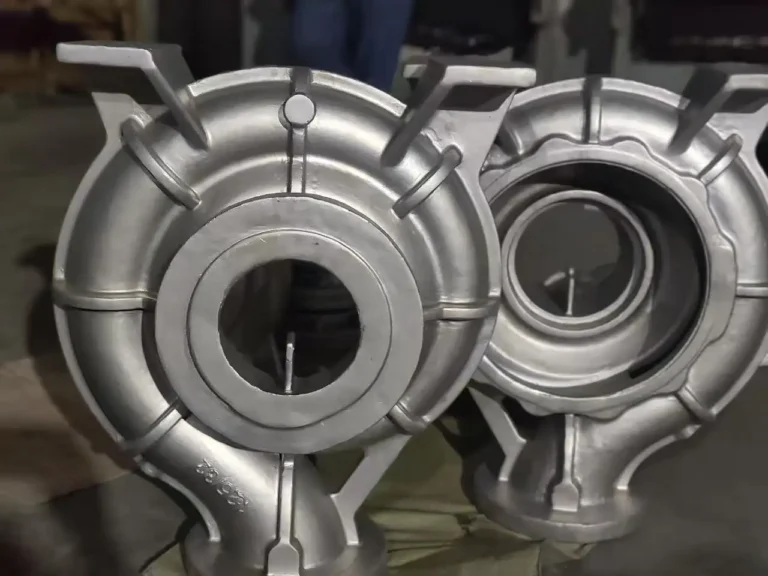
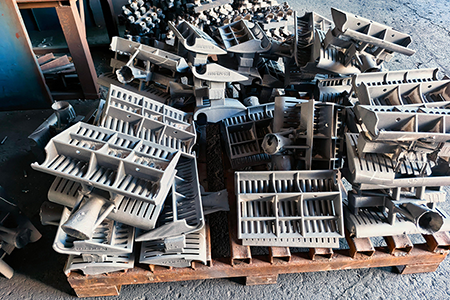
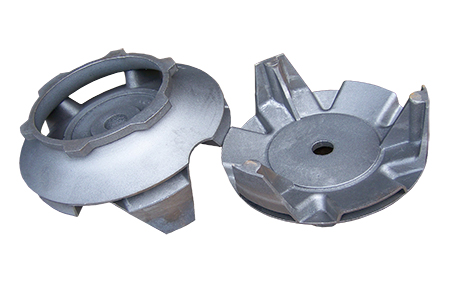
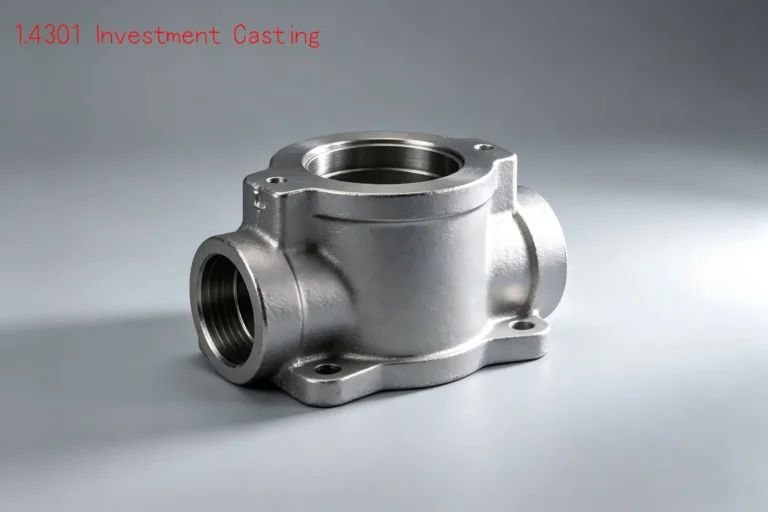
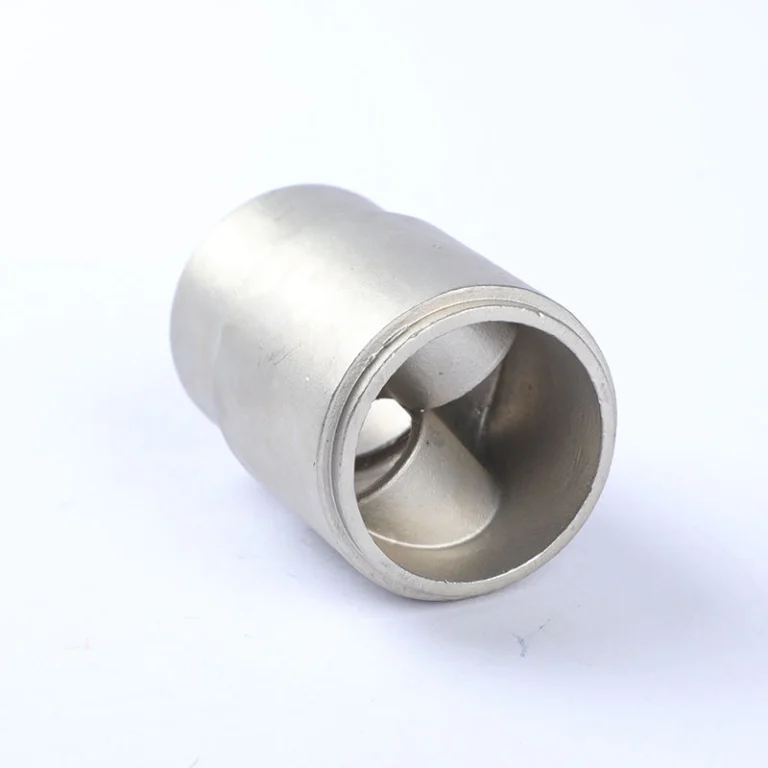
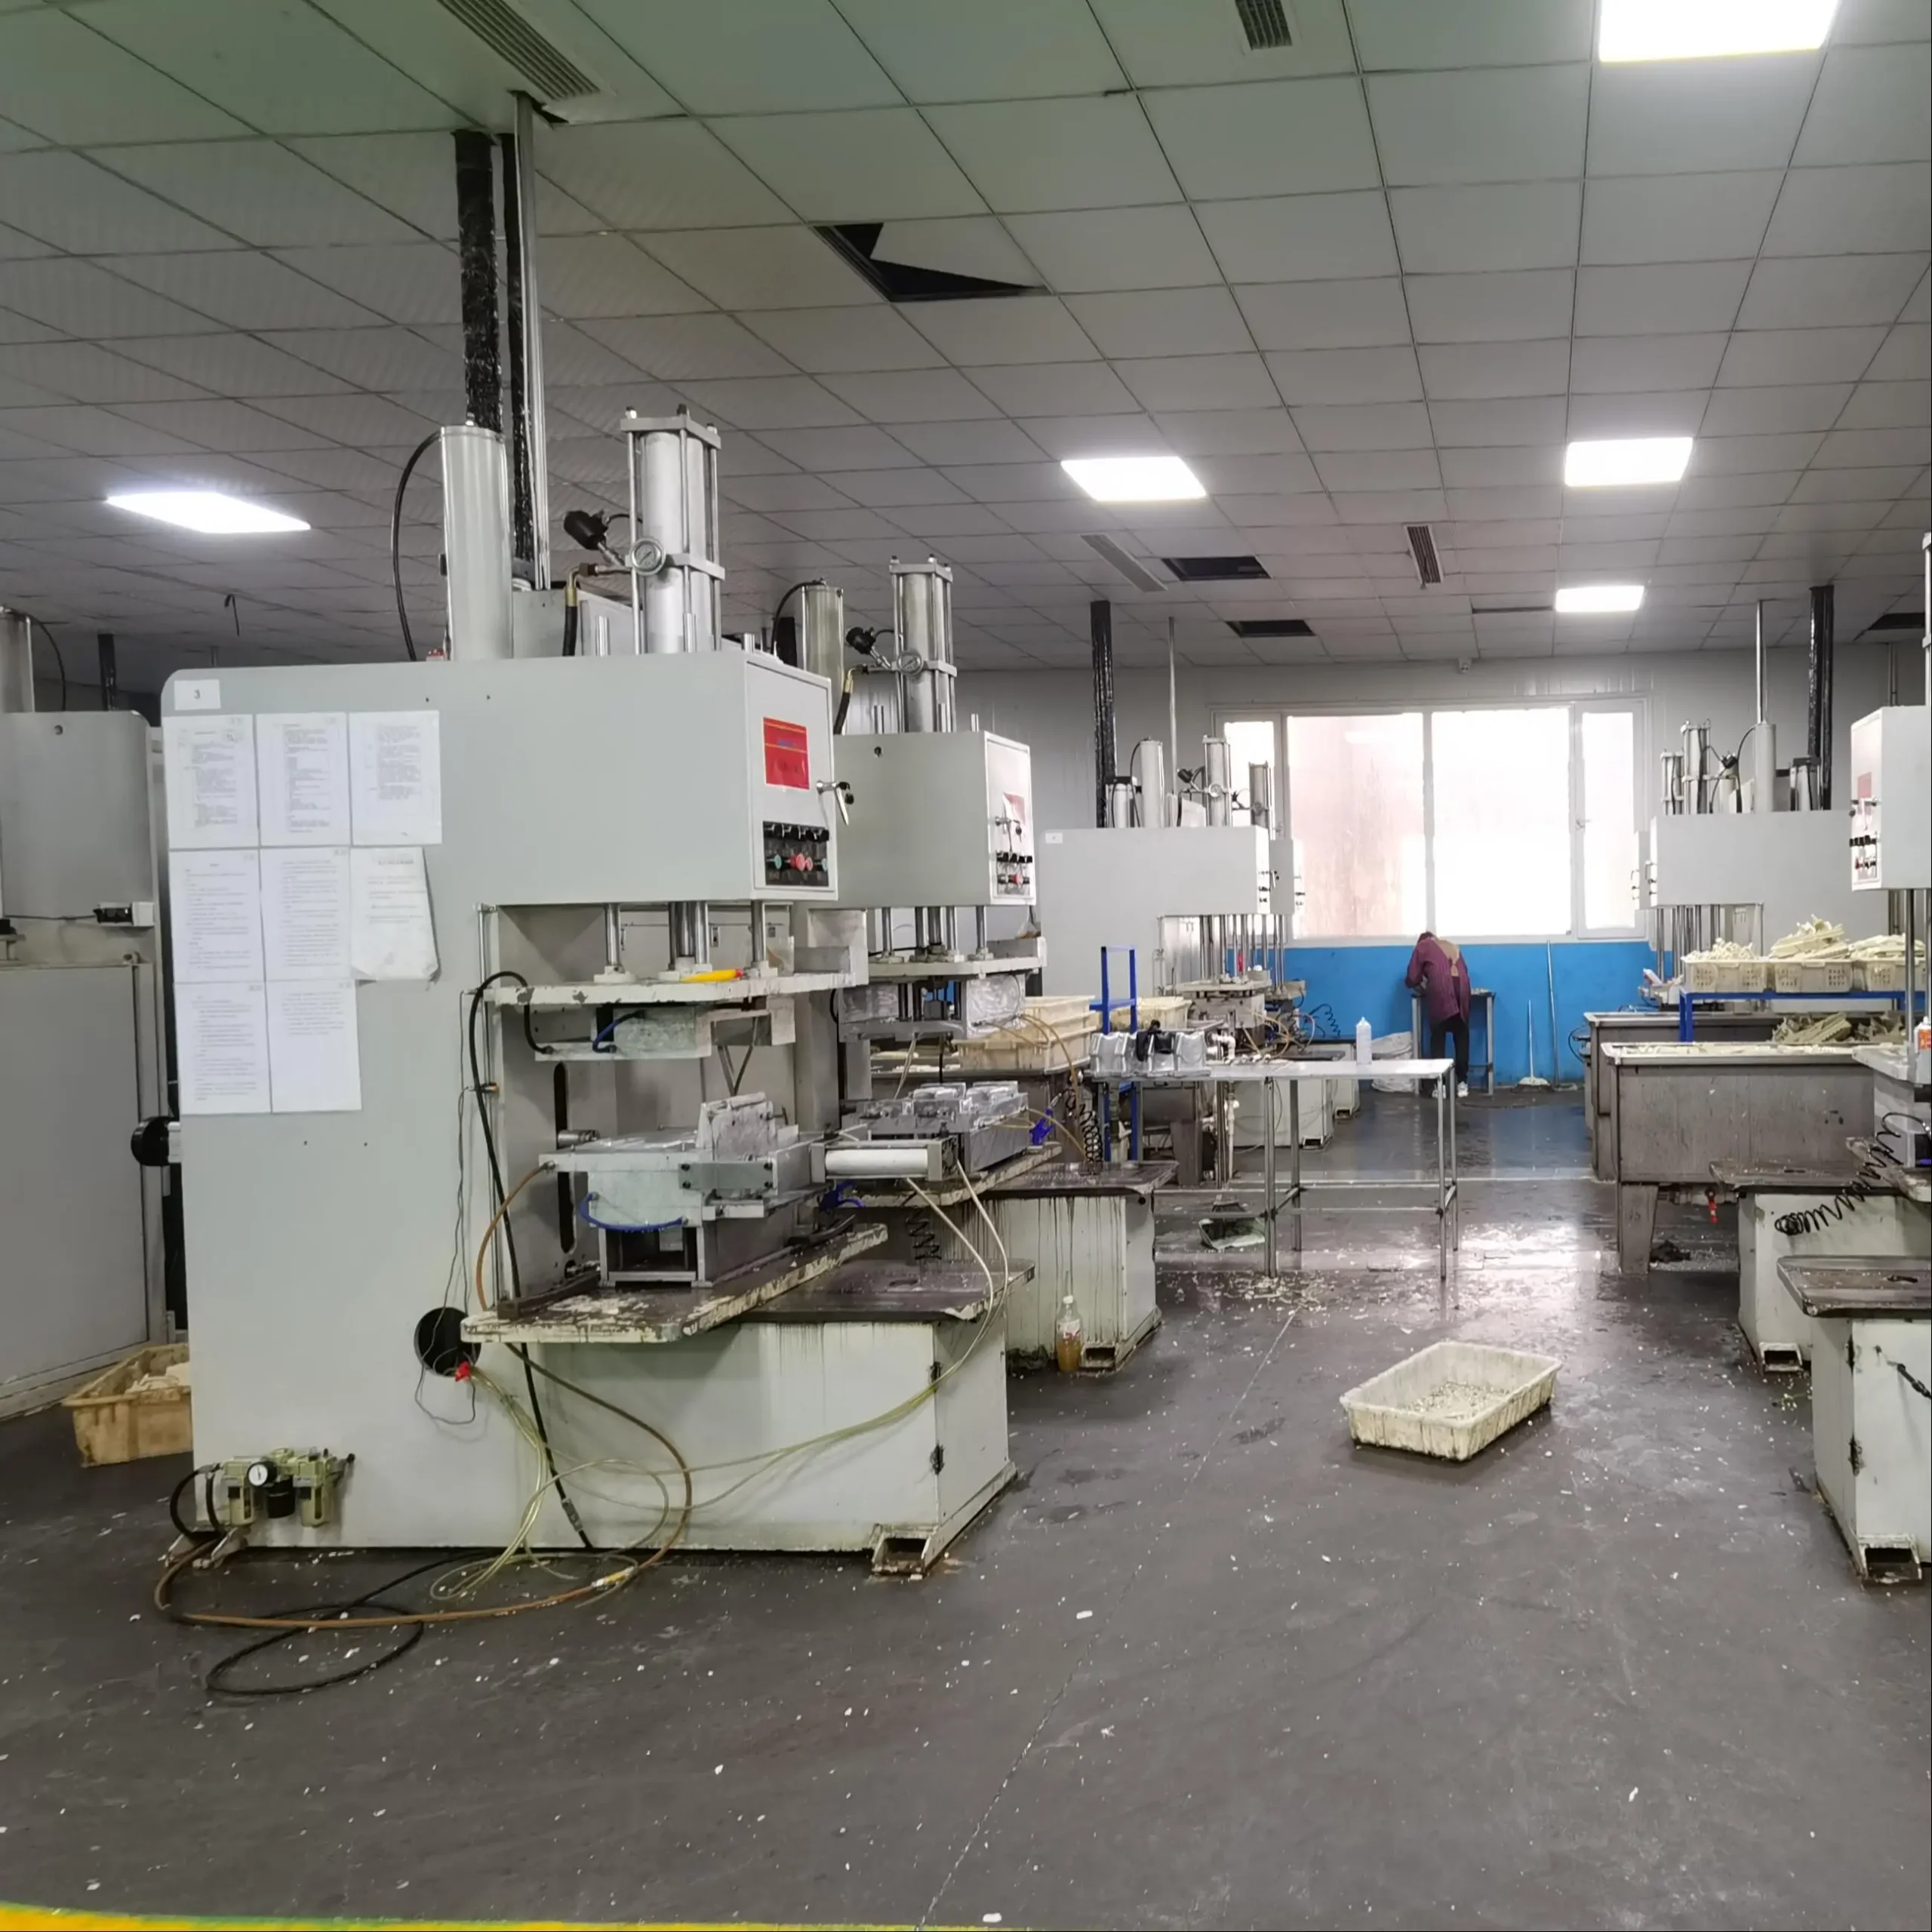
Foundry Inside — where your 1.4301 Investment Casting is made
Real photos from our own workshops, not stock renders. Ask for the latest shop tour and we will send a video walkthrough together with your quote.
Where It Goes
Applications for 1.4301 Investment Casting components
From palm-sized housings to metre-scale impellers, 1.4301 Investment Casting parts from Leesh Holdings serve OEMs in six recurring groups.
Pump & valve parts
Impellers, casings, bonnets and ball-valve bodies in 1.4301 stainless steel for water, food and process lines.
Food & beverage equipment
Corrosion-resistant, easy-clean components for mixing, filling and conveying systems.
Marine & coastal hardware
Deck fittings, brackets and lugs built for salt spray and daily washdown.
Architectural fittings
Cast nodes, clamps and connectors where strength and appearance both matter.
Chemical & process equipment
Dosing components, nozzles and fittings for moderate chemical service.
Energy & industrial machinery
Sensor housings, wear parts and custom brackets produced without welding seams.
FAQ
1.4301 Investment Casting — frequently asked questions
Is 1.4301 the right designation for a cast part?
For castings the closest equivalents are CF8 (ASTM A743) and SCS13 (JIS); wrought 1.4301 is the EN 10088 designation. Drawings specified as 1.4301 are poured to CF8-type chemistry with mechanical properties per the casting standard — we confirm the exact mapping in every quote.
What tolerances and surface finishes can you hold?
As-cast, plan on roughly ±0.3 mm on features up to 25 mm, scaling with size, and an Ra of 3.2–6.3 μm. Critical faces are brought to ±0.05 mm by CNC machining; pickling, passivation and electropolishing are available for surface finish.
What is your MOQ and lead time?
Typical MOQ starts around 50 pieces per item, lower for prototype runs. First articles usually take 3–4 weeks after tooling approval; production lots commonly ship in 30–45 days depending on machining scope.
Do you machine and finish castings in-house?
Yes — CNC turning and milling, drilling and tapping, pickling and passivation, assembly and CMM inspection are handled in our own shops. Heat treatment and special coatings run through long-term audited partners under our process control.
How do I get a 1.4301 Investment Casting quote?
Email your 2D drawing (PDF), 3D model (STEP or IGES), alloy callout, annual quantity and destination port to david.lee@leesh.cn. Our engineers reply within 2–3 working days with pricing, a tolerance plan and lead time, including tooling cost when new tooling is required.
Next Step
Get a fast 1.4301 Investment Casting quote
Send drawings to david.lee@leesh.cn — our engineers reply with pricing, a tolerance plan and a firm lead time. Prefer to talk first? Include your phone number and time zone in the first email.